Titanium CNC machining, without the tool-mark surprises.
Grade 2 and Grade 5 (Ti-6Al-4V) machined with dedicated tooling, coolant and fixtures. ±0.002 mm on critical features, CMM first article, 5–10 day prototypes.
- Grade 2 and Grade 5 (Ti-6Al-4V)
- Dedicated tooling and coolant
- ±0.002 mm critical features
- CMM first article
- Anodising and bead blasting
What we machine in titanium
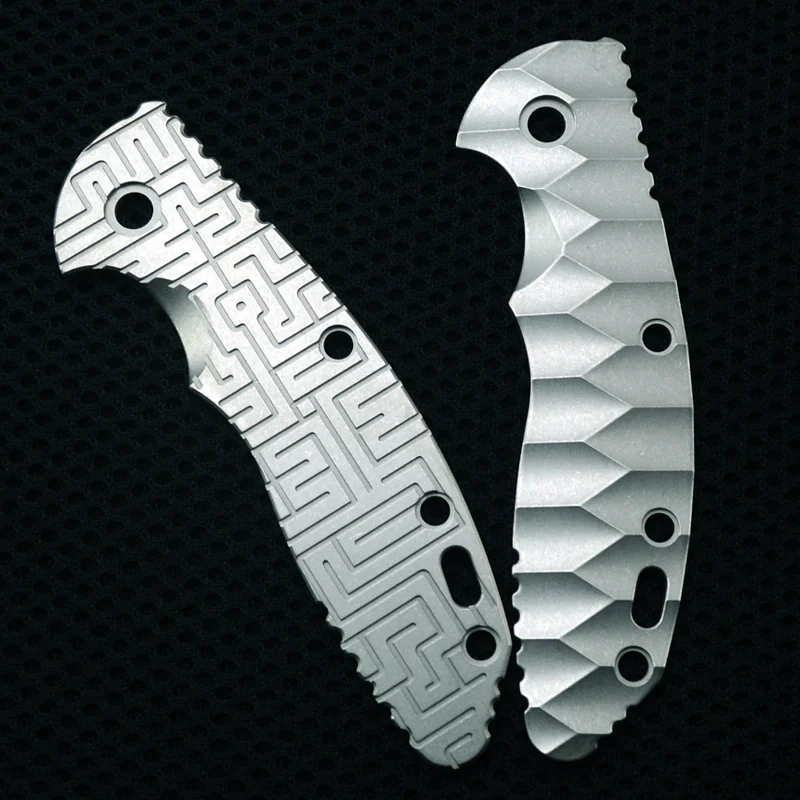
Knife scales, liners and hardware
Scales, liners, spacers, clips and pivots. We hold pivot-hole fit and lock-face geometry, and finish without rounding the edges.
Medical-adjacent non-critical parts
Trays, fixtures, housings and instrument bodies. No implants and no patient-contact BOM parts — we do not hold ISO 13485.
Aerospace brackets and mounts
Non-flight-critical brackets, mounts and test hardware. Material certificates available on request.
Marine and dive components
Corrosion-resistant housings, clips and hardware for saltwater use.
Consumer and EDC parts
Pocket clips, beads, lanyards and small mechanical components.
Prototype and replacement parts
One part or a pilot run, including reverse-engineered parts from a sample.
Grade 2 vs Grade 5
| Grade 2 (commercially pure) | Grade 5 (Ti-6Al-4V) | |
|---|---|---|
| Strength | Moderate | High, heat-treatable |
| Machinability | Easier | Harder; work-hardens quickly |
| Typical use | Corrosion resistance, chemical, marine, jewelry | Knife parts, aerospace, high-load components |
| Finishing | Anodises to strong colours | Anodises; colour is less vivid than Grade 2 |
| Our approach | Standard titanium route | Sharp tools, low surface speed, high-pressure coolant |
If you are choosing between grades, tell us the load and the environment; we will say which one we would machine.
How we machine titanium
- Dedicated tooling and coolant. Titanium never shares a tool holder, insert or coolant tank with aluminum or steel.
- Sharp tools, low surface speed. Titanium work-hardens, so rubbing is the enemy. We change inserts before they wear, not after.
- High-pressure coolant. Heat stays in the chip instead of the part, which protects thin walls and surface finish.
- Light finish passes. The last pass removes the work-hardened skin without pushing the part away from the cutter.
- CMM first article. The first part is measured before the run continues, so a drift is caught at part one, not part fifty.
Finishes for titanium
Anodising
Type II in clear, blue, gold, purple and black. Colour is controlled by voltage, so send a sample if the shade matters.
Bead blasting
Matte, uniform surface that hides tool marks and fingerprints.
Brushing and polishing
Satin or mirror finishes for visible parts.
Laser marking
Part numbers, serials and logos, quoted with the part.
What we do not claim
We do not hold ISO 13485 or AS9100, and we do not make implants or flight-critical parts. We do not have 5-axis machining; most titanium parts can be made in two or three setups on a 4-axis machine, and if a part genuinely needs simultaneous 5-axis we will say so before quoting. We do not anodise in-house — finishing is through partner plants, quoted as one finished part, one invoice.
Titanium material data · Knife manufacturing · Quality and inspection
FAQ
Which titanium grades do you machine?
Grade 2 commercially pure and Grade 5 (Ti-6Al-4V) most often. We also quote Grade 9 and Grade 23 when the material is available; send the spec and we will confirm.
Do you use the same tools and coolant for titanium and aluminum?
No. Titanium gets its own tooling, coolant and fixtures. Sharing tooling with aluminum or steel is how titanium parts pick up contamination and tool marks.
Can you anodise titanium?
Yes — Type II anodising in clear, blue, gold, purple and black, through a partner plant. We also offer bead blasting, brushing and polishing.
Why do titanium parts show tool marks?
Titanium work-hardens and conducts heat poorly, so the cutter rubs instead of cutting if speeds and feeds are wrong. We run sharper tools, lower surface speed, high-pressure coolant and a lighter finish pass.
What tolerance can you hold in titanium?
±0.002 mm on critical milled features, ISO 286 IT6–IT8 fits, and ISO 2768-mK for unmarked dimensions. Thin walls and long parts are quoted with the achievable tolerance stated.
Can you make medical titanium parts?
We machine non-implant components such as trays, fixtures, housings and instruments. We do not hold ISO 13485 and do not make implants or parts that go on a patient-contact BOM.
Can you make knife parts in titanium?
Yes — scales, liners, spacers, clips and hardware. See the knife manufacturing page for finishes and tolerances.
Send a titanium part. Get a real quote in 16 hours.
Upload a STEP file and drawing. We reply with price, lead time, finishing options and a DFM note on the features that will fight the tolerance.