CNC Machining Stainless Steel
Stainless is specified far more often than it is needed, and that costs money — it cuts several times slower than aluminium, so on a production batch the grade on the drawing can move the price more than any feature on it. When the part really does live in water, chemicals or a washdown, this is what each grade gives you.
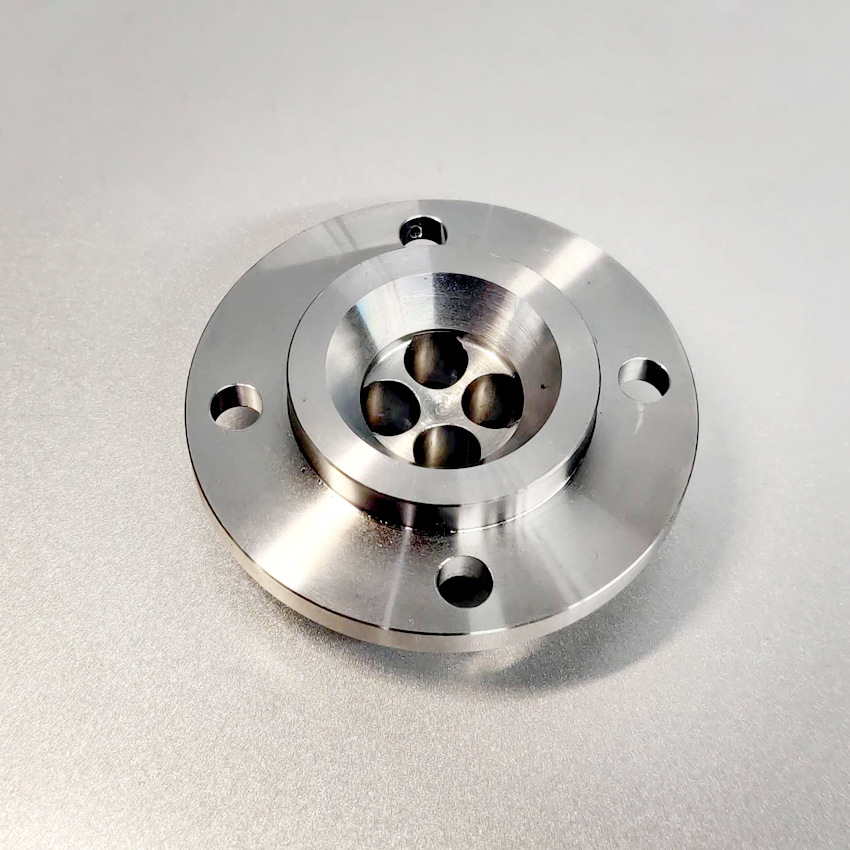
The grades we machine, and what separates them
The practical decision is usually 303 against 304 against 316L: how much corrosion resistance you actually need, and how much machining time you are willing to pay for it.
| Grade | Best for | Machinability | Notes |
|---|---|---|---|
| 303 | Fittings, shafts, fasteners and anything made in quantity | The easiest stainless to cut | Sulphur added for machinability, which costs a little corrosion resistance. Not suitable for welding |
| 304 / 304L | General corrosion resistance at sensible cost | Moderate; work hardens readily | The default stainless. 304L has lower carbon for welding. Not for chloride or marine exposure |
| 316 / 316L | Marine, chemical, food and medical environments | Slower than 304 | Molybdenum gives real chloride resistance. The extra cycle time is the price of that |
| 17-4 PH | High strength plus corrosion resistance; shafts, valve parts, tooling | Moderate; harder once aged | Precipitation hardening — machine in the solution-treated condition where possible, then age |
| 416 | Free-machining magnetic stainless for shafts and hardware | Good | Magnetic and heat treatable, lower corrosion resistance than 304 |
| 440C | Knife blades, bearings, wear parts | Difficult, especially hardened | High carbon martensitic grade; usually machined soft then hardened and ground or EDM cut |
Work hardening is the thing to understand
Stainless does not simply resist cutting — it hardens where it has been rubbed. A worn edge, too light a cut, or a tool that dwells in the cut leaves a harder skin behind, and the next pass has to get through that. The instinct to take a lighter cut when something is going wrong is exactly the wrong instinct here.
What works is a positive, deliberate cut: sharp tooling, a real chip load, rigid holding, and plenty of coolant. Cycle times are longer than aluminium and that is simply the material, not the shop.
Work hardening also matters at inspection. A stainless part that has been rubbed rather than cut can measure correctly and still be a problem later, which is one reason we measure the first article before the batch runs rather than after. How we inspect →
| At a glance | |
|---|---|
| Typical tolerance | ±0.002 mm (±0.0001 in) on machined features |
| Machinability | Moderate — 303 easiest, 316L and 440C slowest |
| Standard finishes | Passivation, bead blast, brush, polish, electropolish |
| Magnetic | 303, 304 and 316 are essentially non-magnetic; 416, 440C and 17-4 PH are magnetic |
| Certificates | EN 10204 3.1 on request |
Four things worth settling on a stainless drawing
Ask whether it needs to be stainless at all
If the grade was chosen for appearance rather than corrosion, anodised aluminium often looks better and costs far less to cut. If it lives in salt water, 316L it is.
Specify passivation if corrosion resistance matters
Machining smears iron across the surface, which is where rust starts on a stainless part. Passivation removes it. It changes nothing visible, so it has to be on the order to happen.
Watch internal corners and deep pockets
Stainless punishes long tools and small radii much harder than aluminium does. A larger corner radius saves real money here.
Say if the part is welded
304L and 316L exist for welding. Specifying 303 for a part that will be welded is a common and expensive mistake.
Finishes that work on stainless steel
Stainless is usually finished by texture rather than by coating — the corrosion resistance is in the metal, not on top of it.
Passivate anything that will meet moisture
Machining smears free iron across a stainless surface — off the tooling, and off any carbon-steel chips in the shop. That iron rusts even though the part does not, which is why a stainless part can show orange spots within a month. Passivation takes the iron off and lets the chromium oxide re-form. It is cheap, and it is the single finish worth asking for on a part that lives outdoors, in water or in a wash-down area.
| Finish | What it does | Worth knowing |
|---|---|---|
| Bead blast | Even matt grey | Hides tool marks. Slightly rougher surface than as-machined |
| Brushing | Directional satin grain | Say which faces and which direction. Grain across a joint line shows |
| Buff polishing | Bright, close to mirror | The dearest of the texture finishes on stainless |
| Electropolishing | Smooths and brightens, and cleans the surface | Takes a little material off — allow for it on a tight tolerance |
| Tumbled | Deburrs and evens the edges | Rounds sharp edges |
| Black oxide | Dark conversion coating | Thinner and less durable on stainless than on carbon steel |
Passivation, electropolishing and black oxide are done at partner plants we have used for years. The parts come back here and are checked before they ship.
Four stainless jobs, start to finish
Filmed in our shop in Dongguan. Where a clip sits beside a single part, that machine is cutting that exact part.
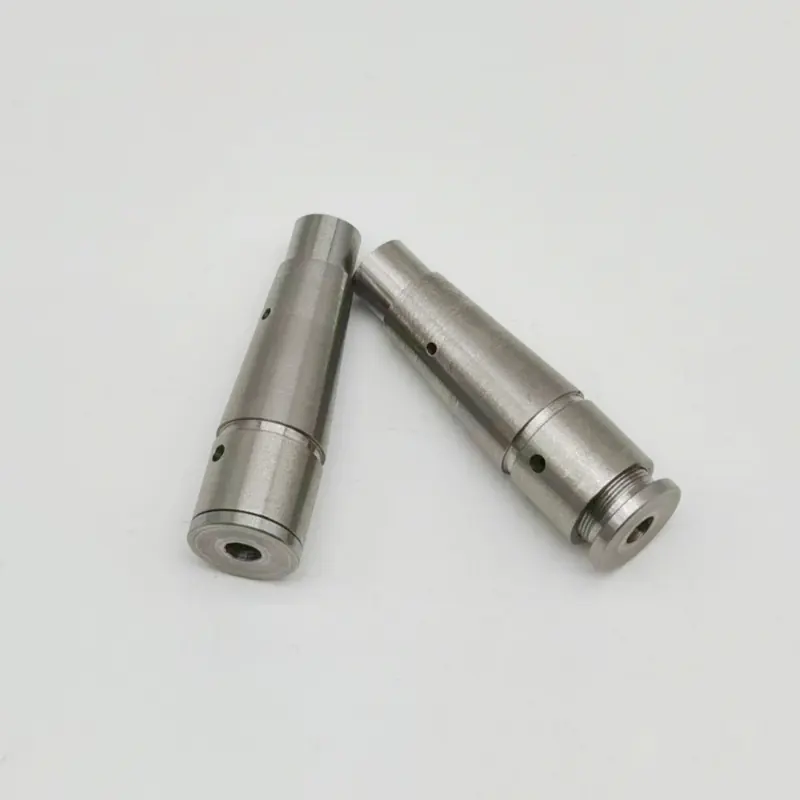
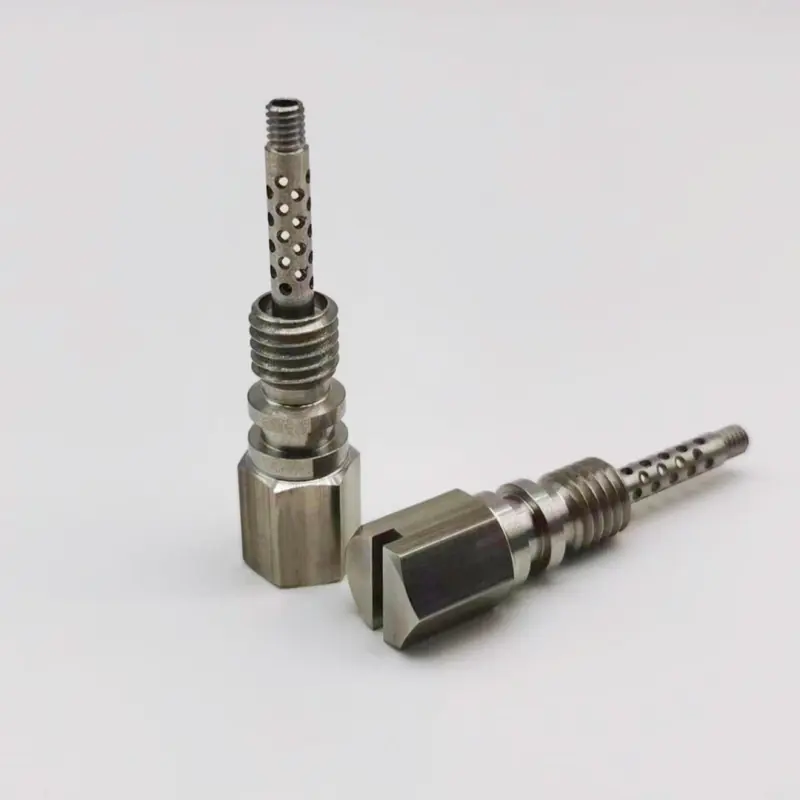
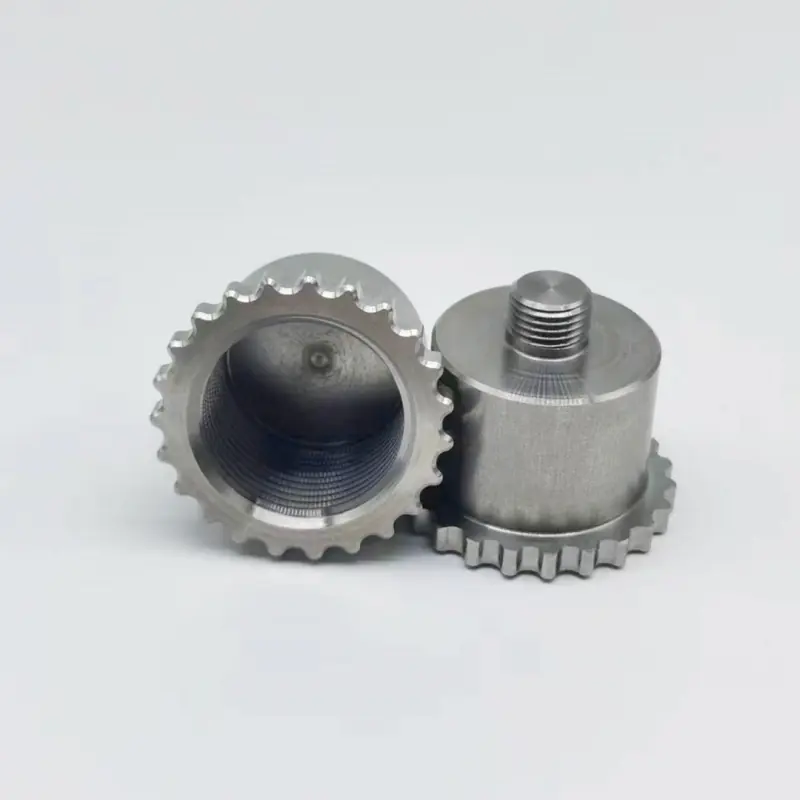
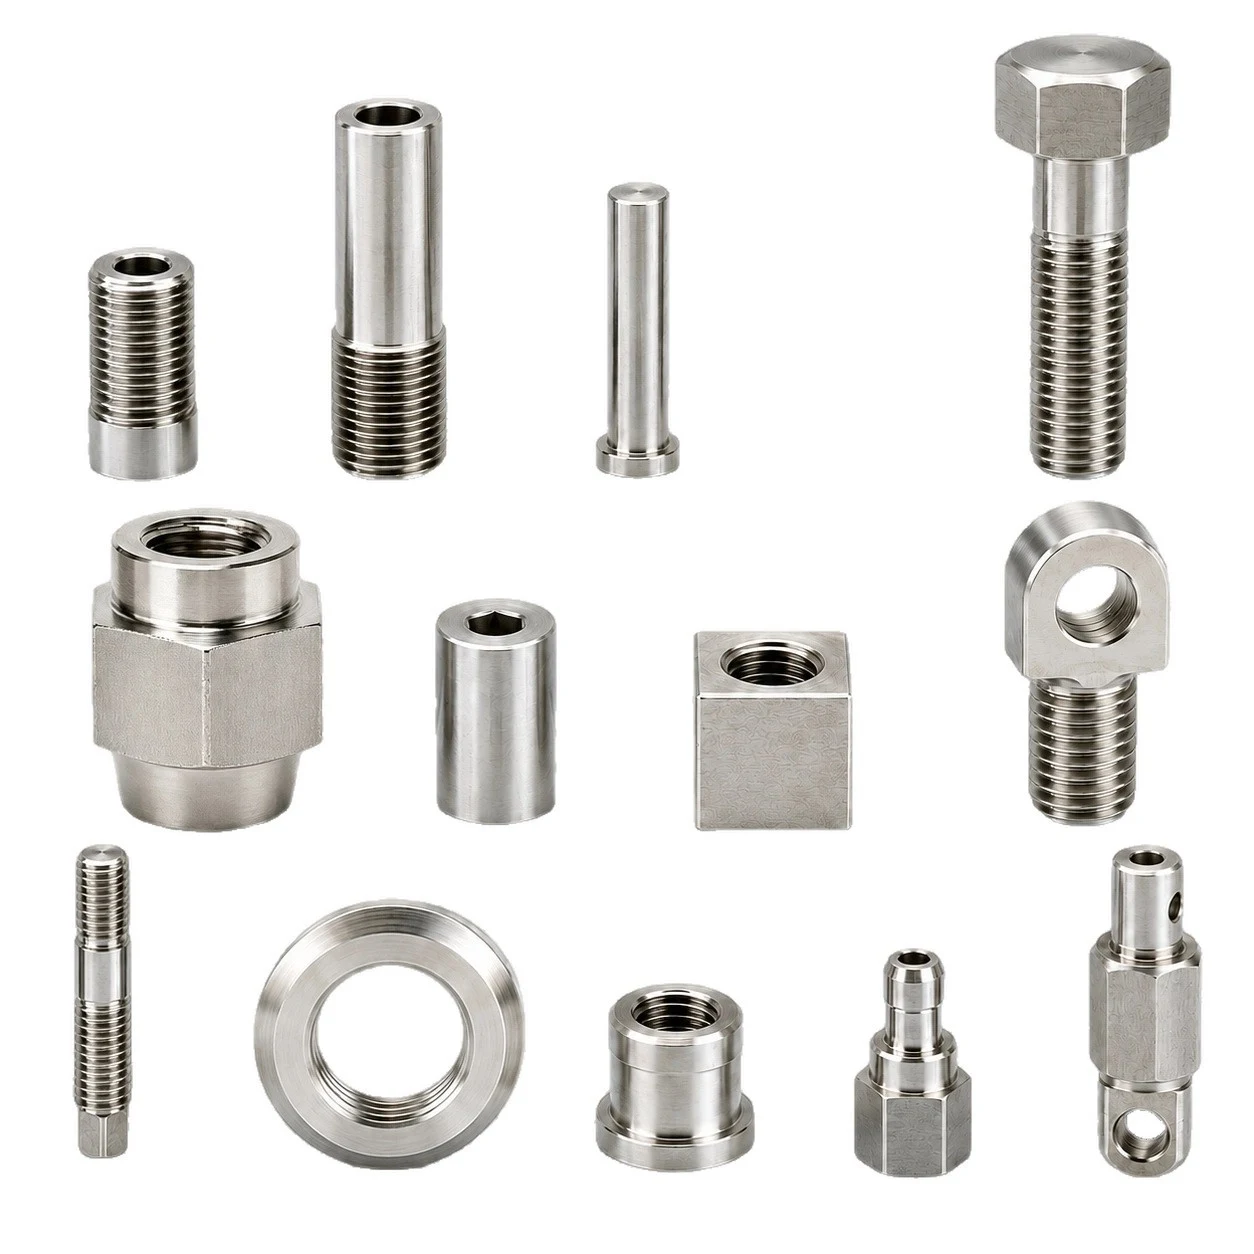
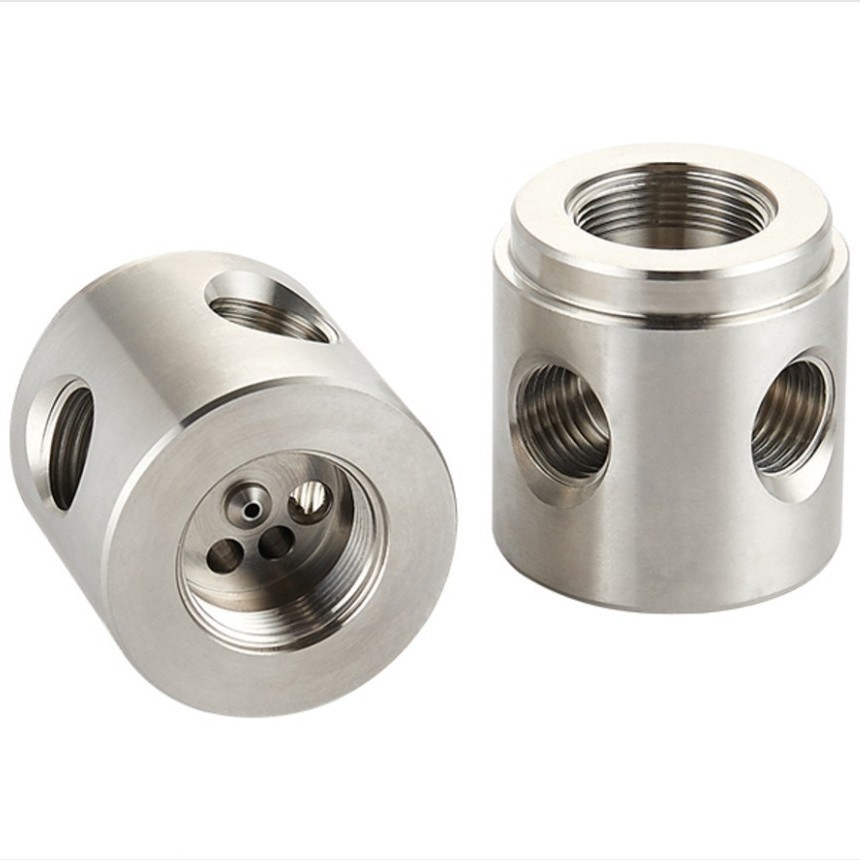
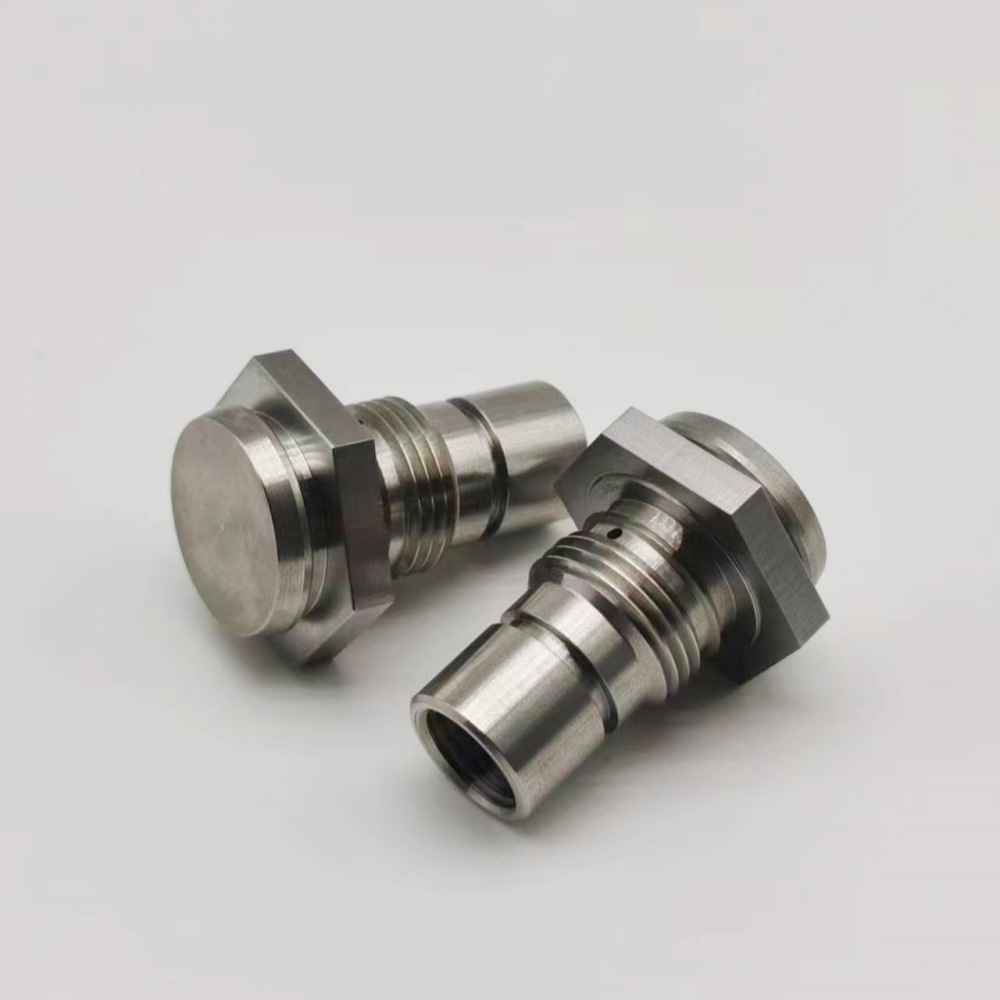
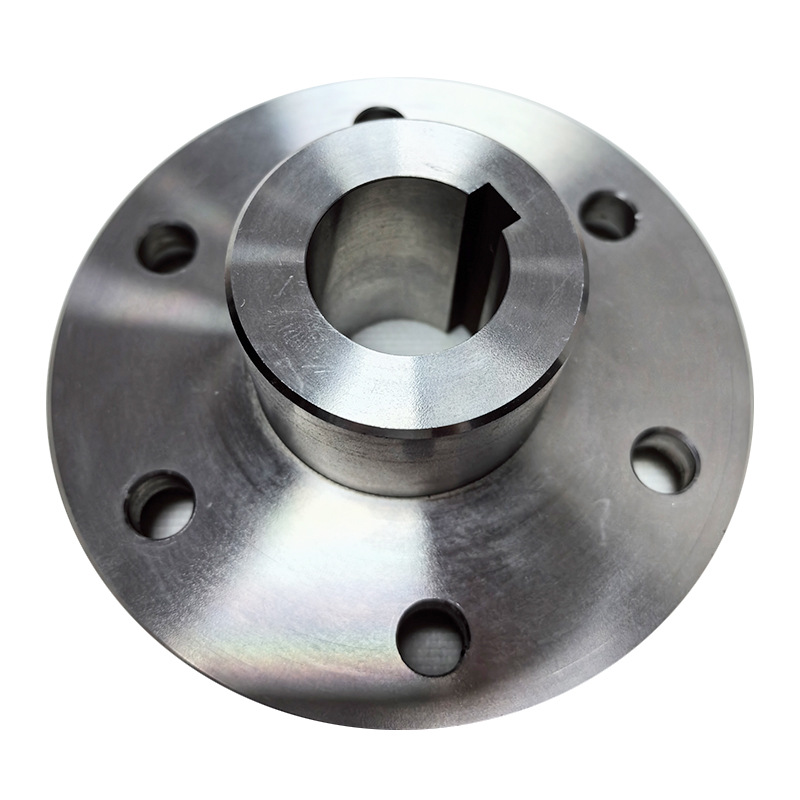
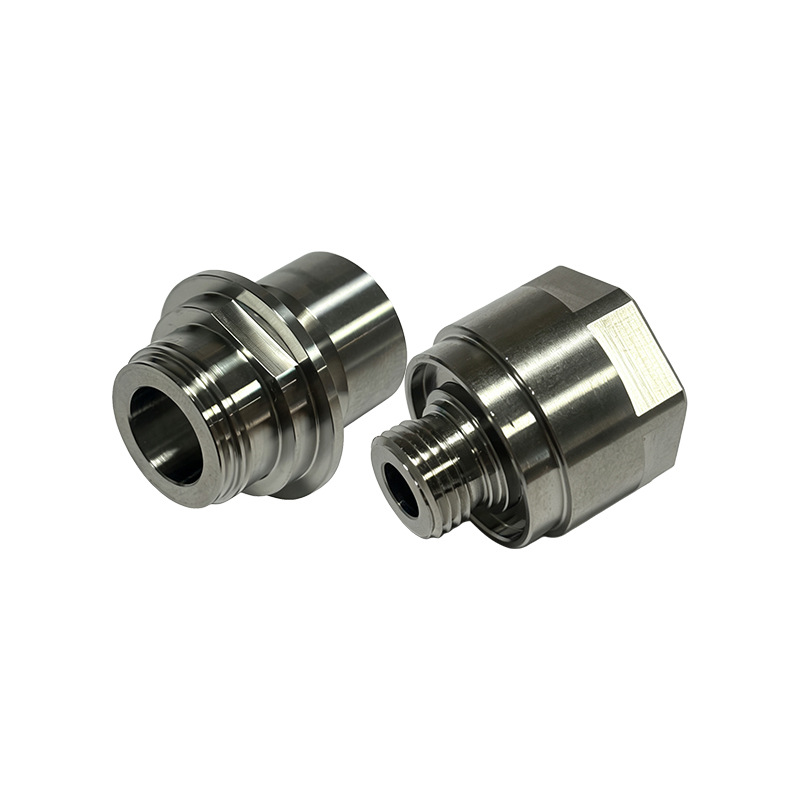
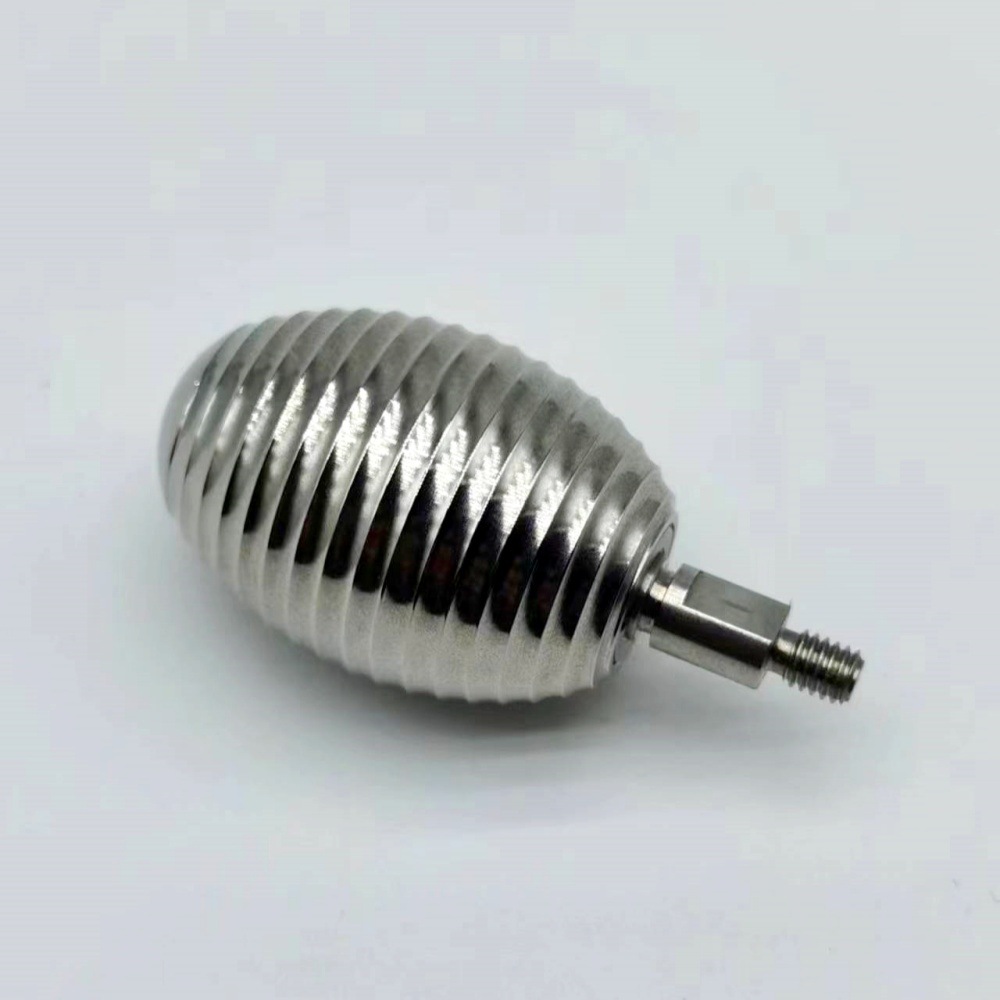
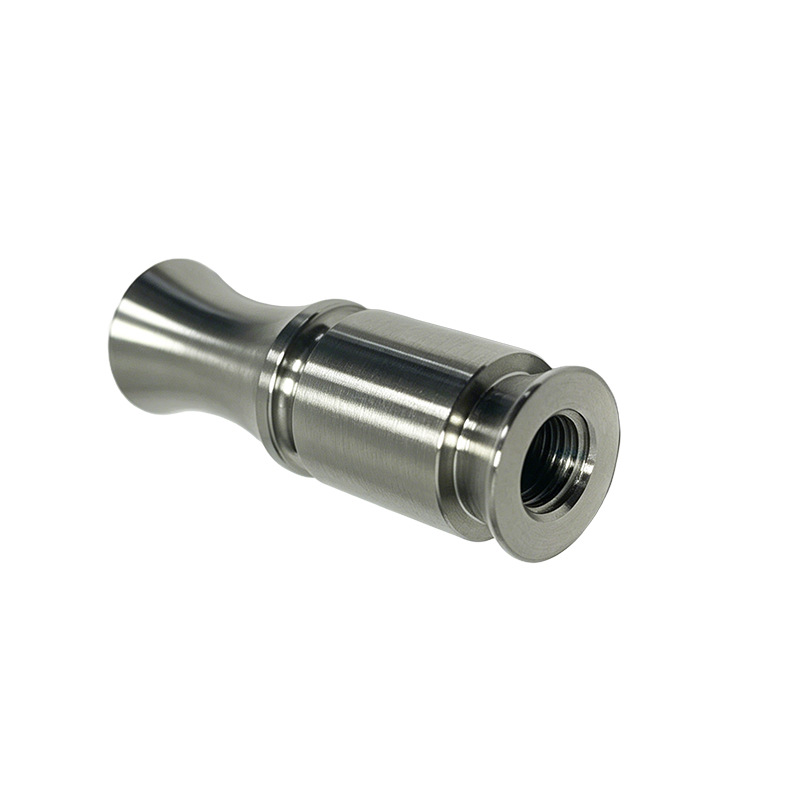
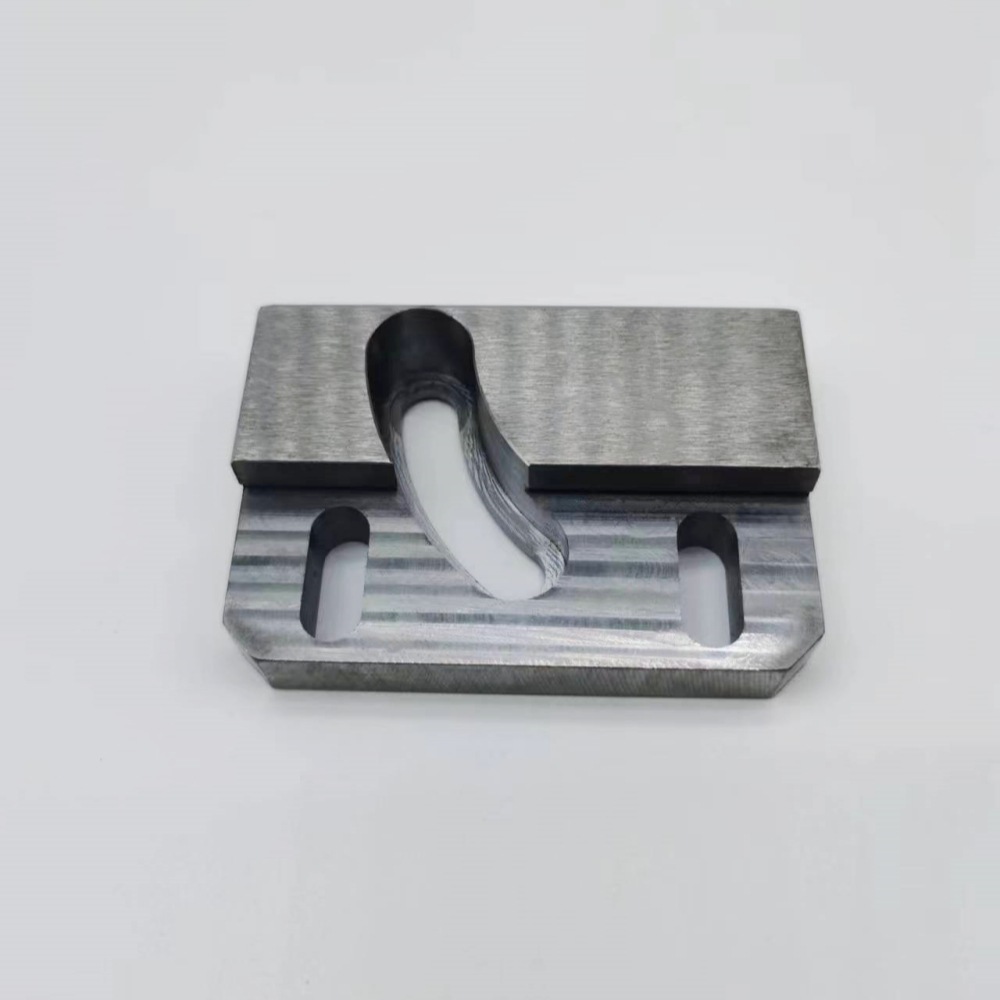
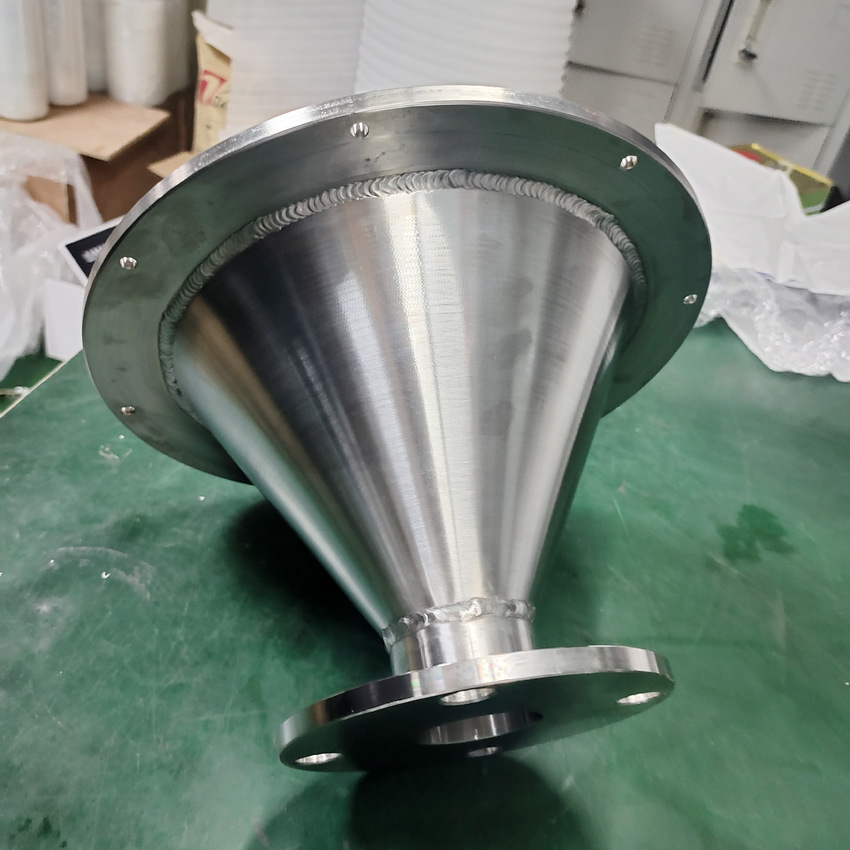
CNC machined stainless steel parts
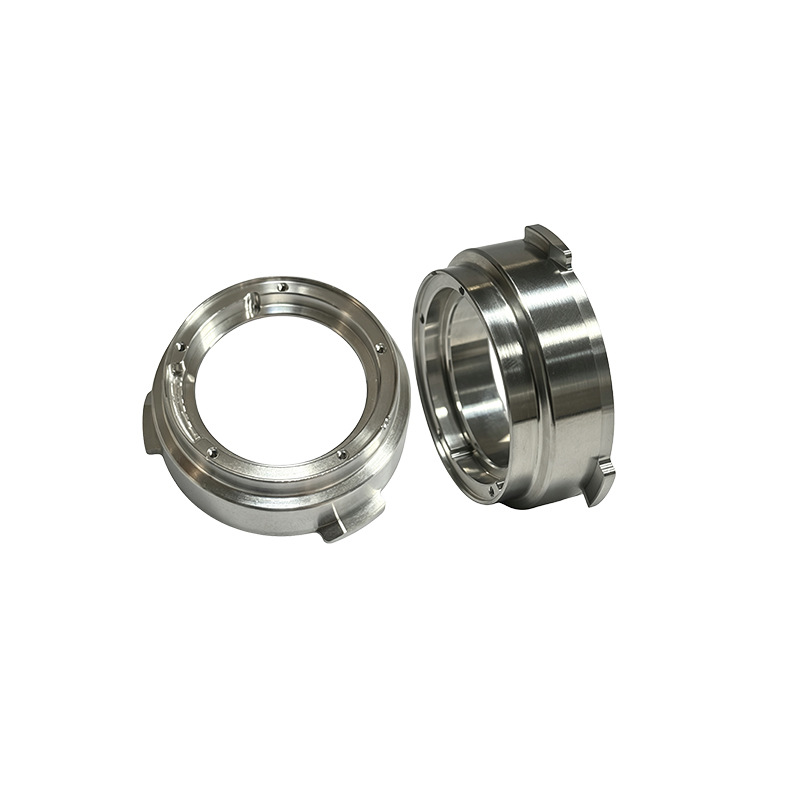
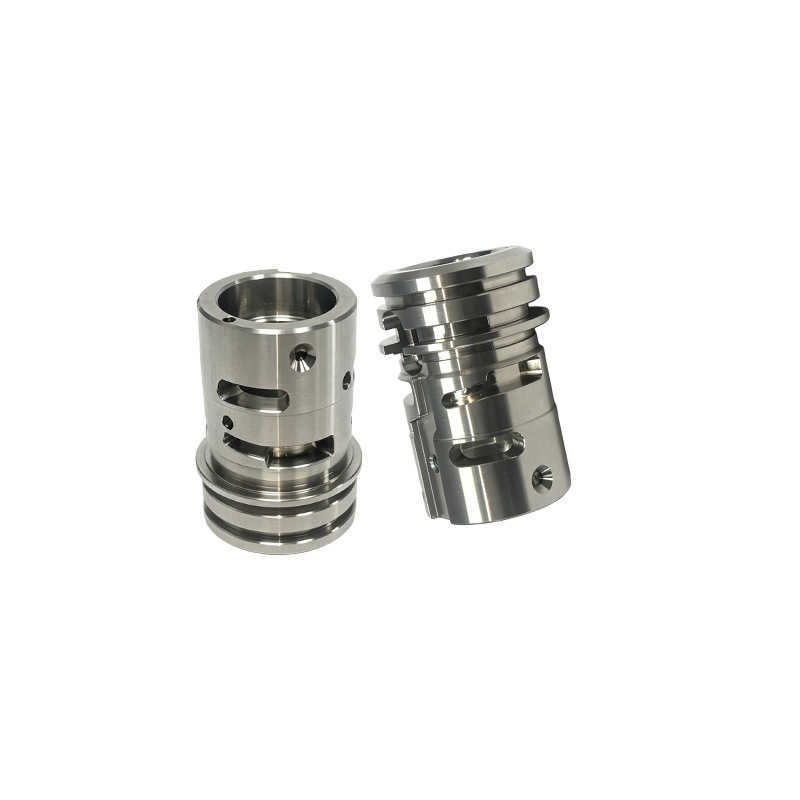
Valve bodies, fittings, mounts and housings in 303, 304, 316 and 17-4 PH — turned, milled, and inspected here before they ship.
Ready for a quote?
Send the drawing — price and lead time within 16 hours. STEP, IGES, X_T, DWG, DXF or PDF.
No minimum order.