The reliable place to
source your rapid
prototypes and
custom CNC parts
Milling, turning, wire and sinker EDM, sheet metal and 35+ finishes under one roof in Dongguan. Send a drawing; within 16 hours Bill sends back price, lead time, and the two or three changes that would make the part cheaper.
Precision CNC Machining Capabilities
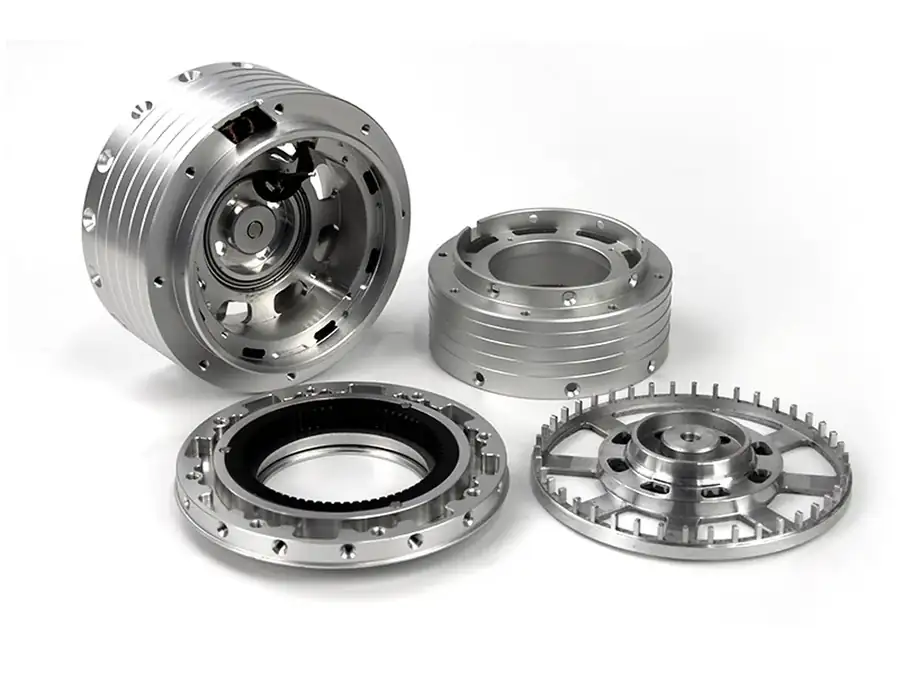
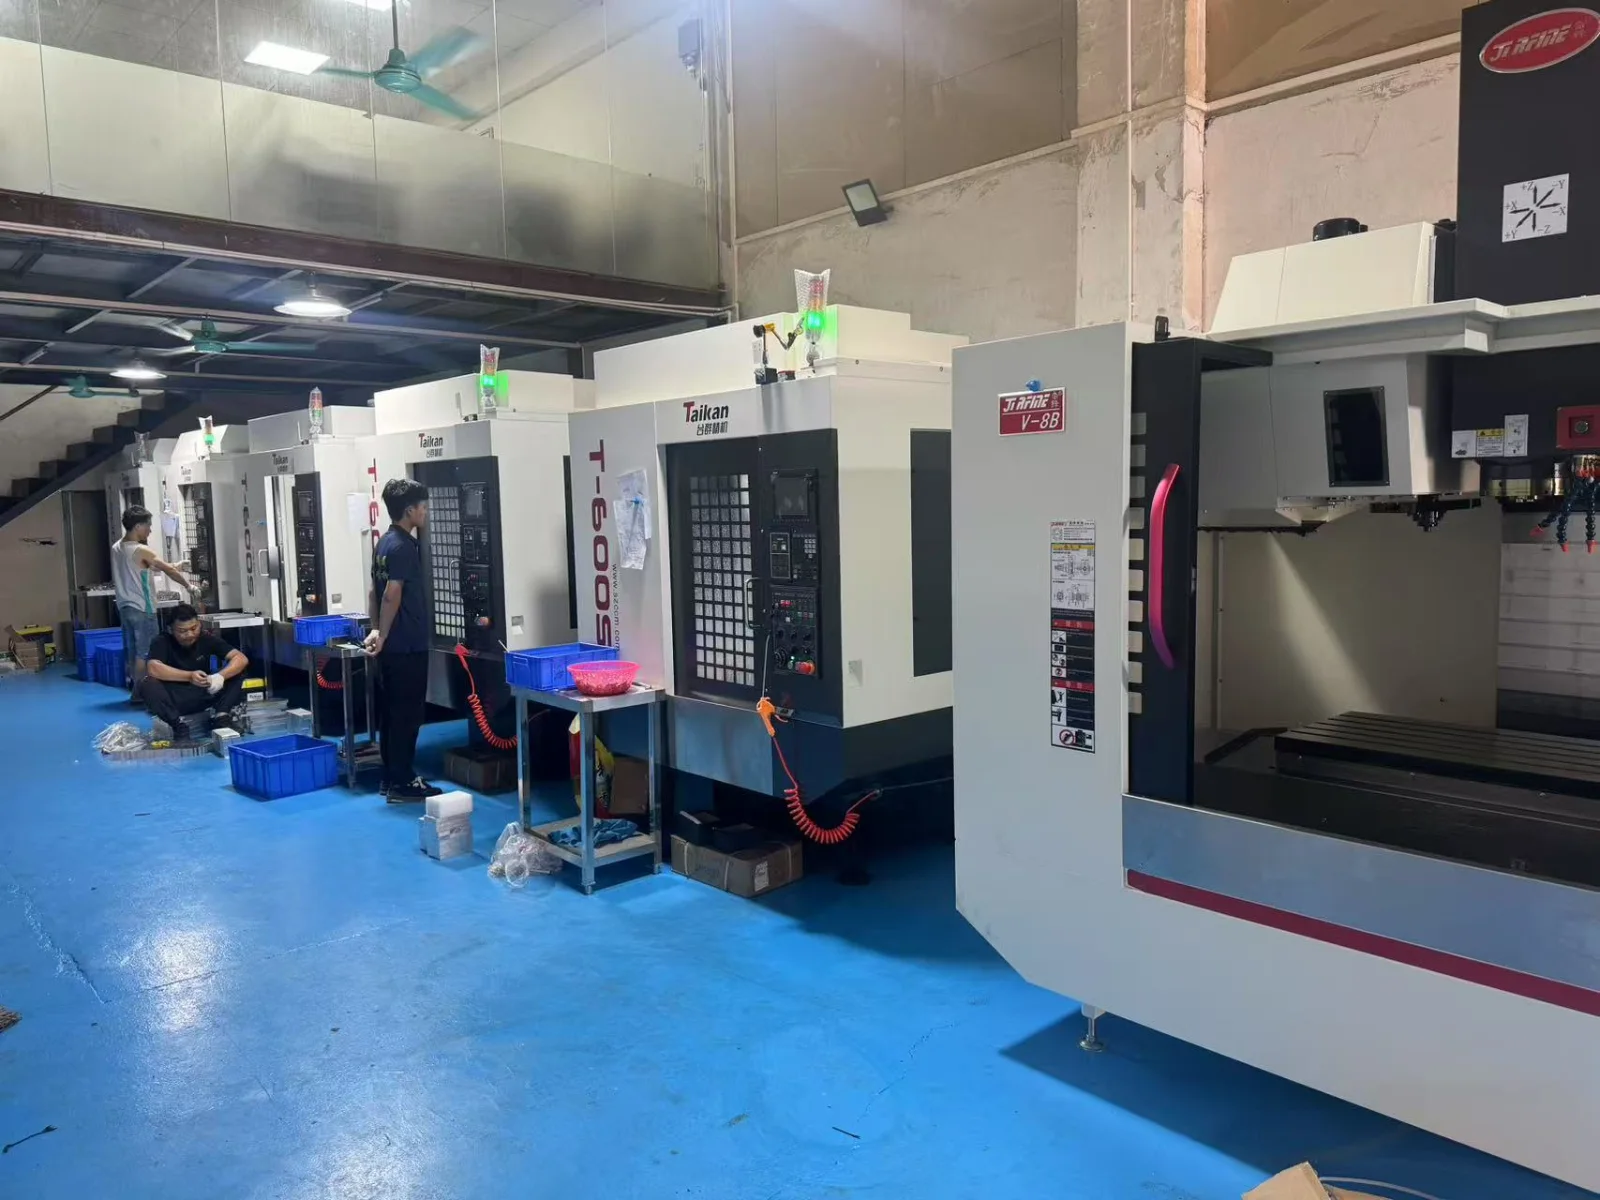
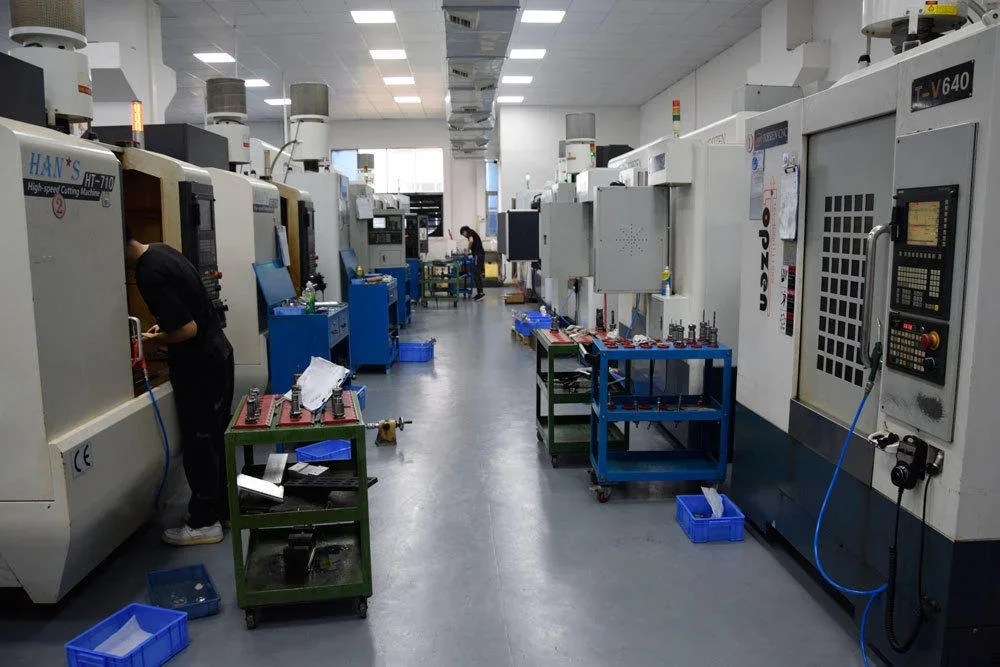
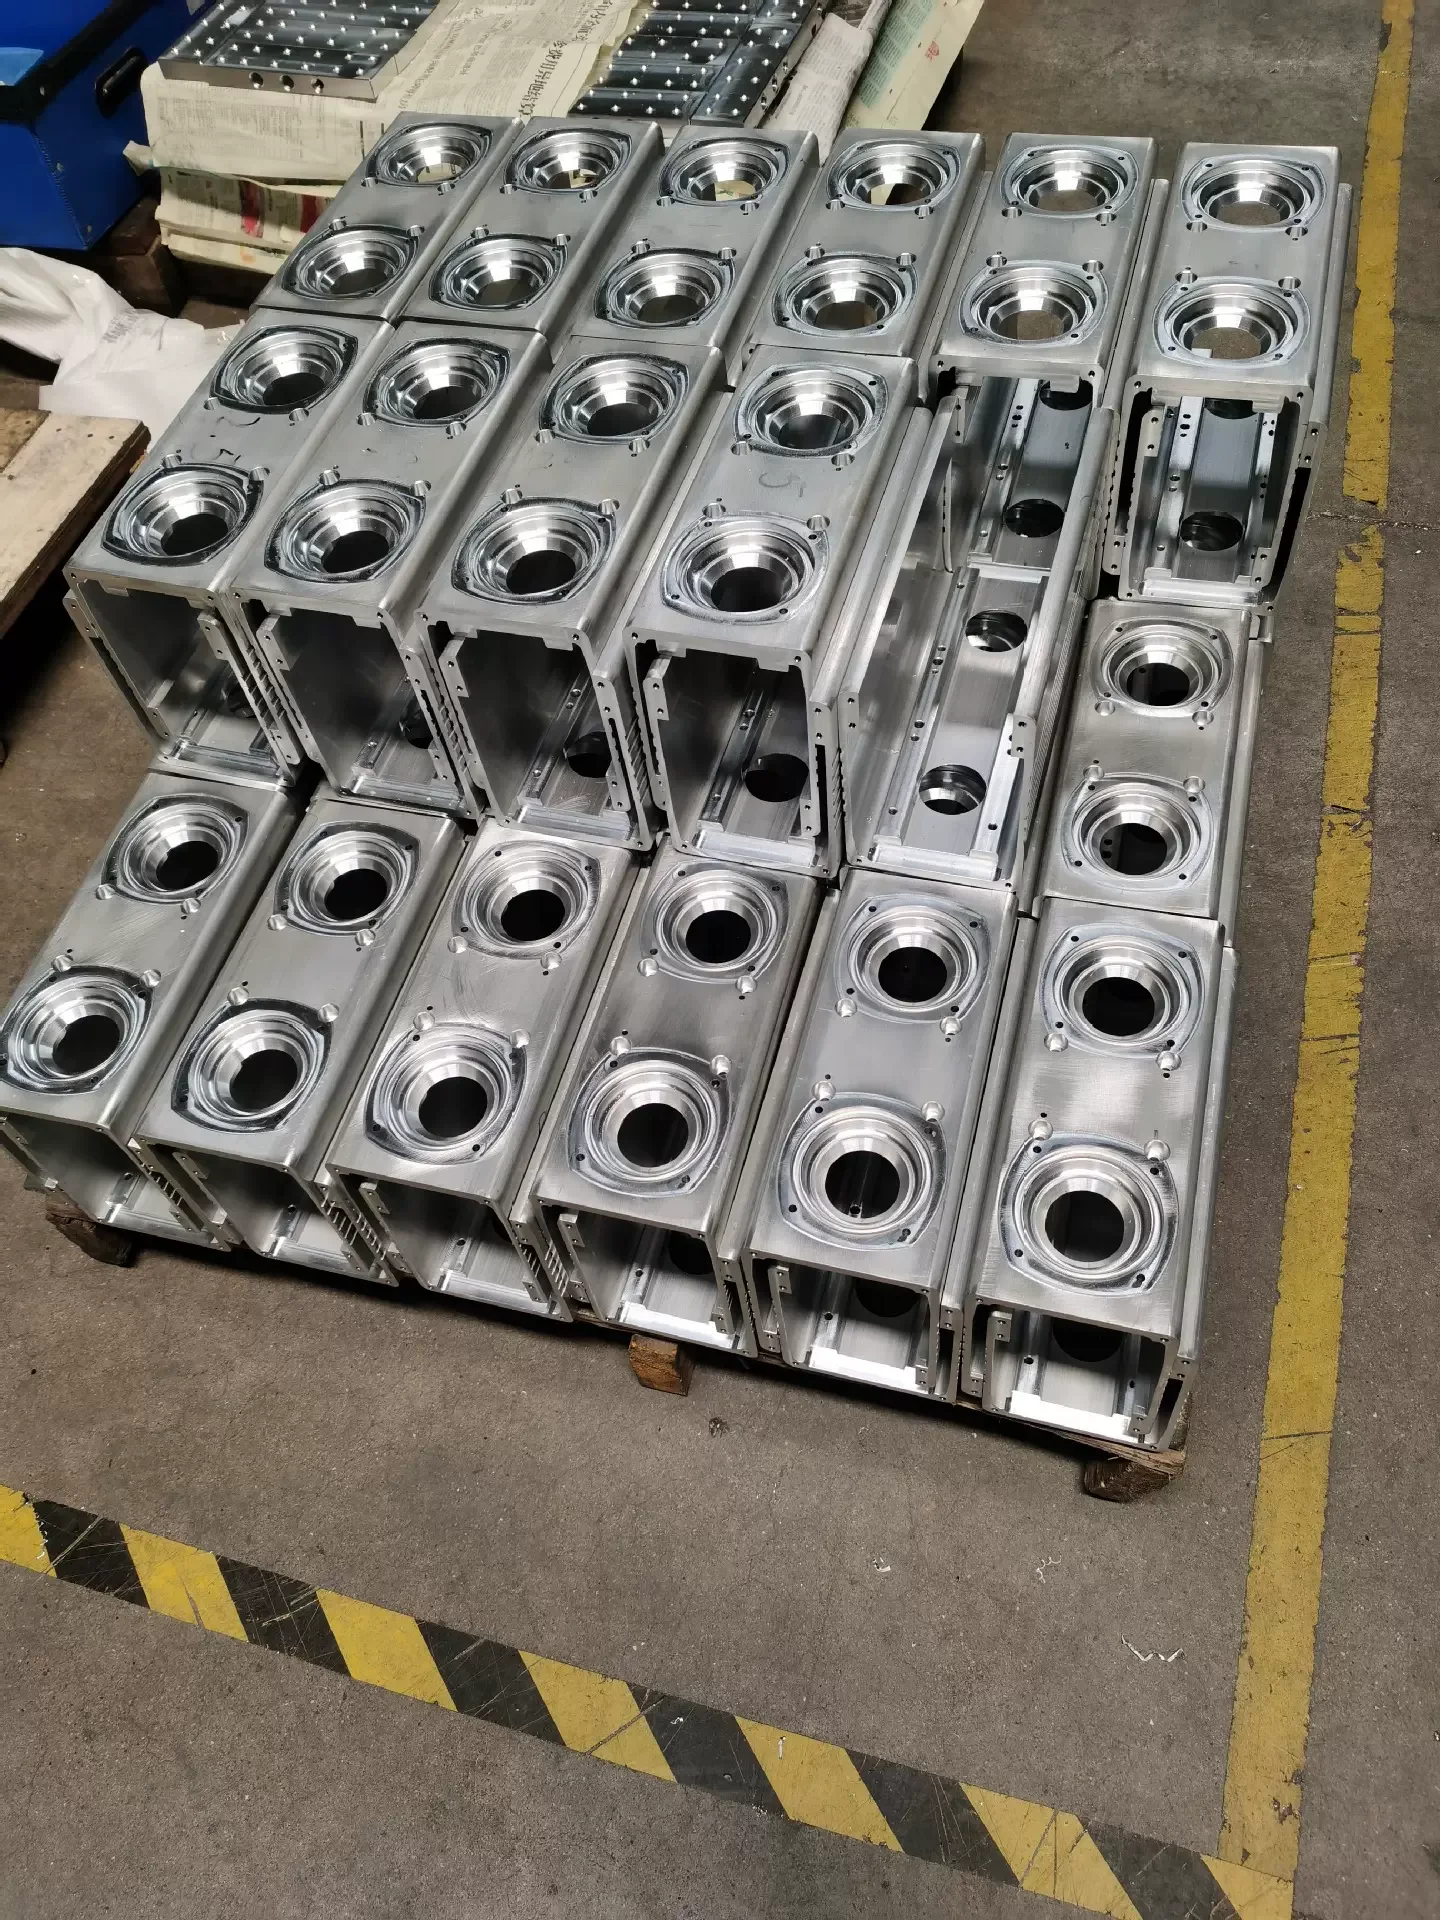
GY machines custom metal parts in aluminium, brass, stainless steel, copper and steel, and CNC plastic parts in Delrin (POM), Nylon, PEEK and other engineering plastics — milled, turned, EDM-cut and finished on our own floor in Dongguan. 32 machining centres, 12 lathes and 12 EDM machines under one roof, and every first article is measured on a CMM before the run continues. Nothing is subcontracted out of sight.
CNC Milling
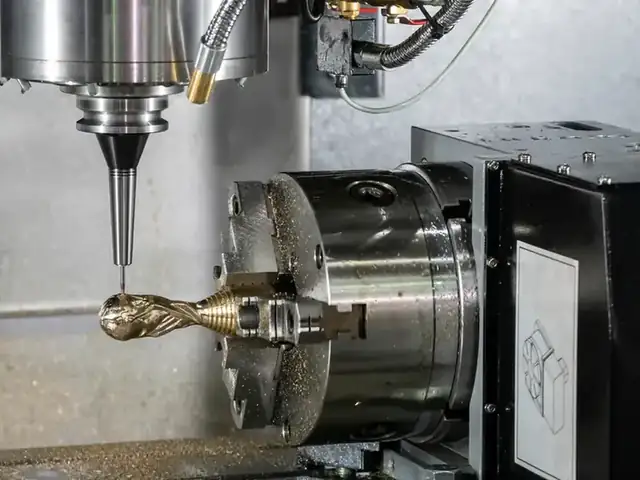
Housings, brackets, manifolds, plates and fixtures on 2-, 3- and 4-axis centres. Thirteen of the 32 centres are four-axis, so multi-face parts stay in one setup and true position holds between features.
- Achievable tolerance±0.01 mm on critical features
- Envelope800 × 600 × 500 mm
- Axes2 / 3 / 4 — no 5-axis
- Machines32
CNC Turning
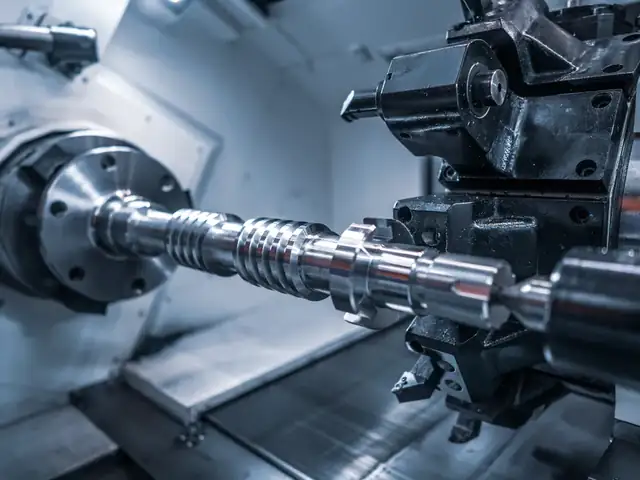
Shafts, bushings, pins, fittings and threaded parts on twelve CNC lathes. Turned parts that need cross-holes or flats go straight to a milling setup in the same building.
- DiameterØ 3 – 250 mm
- FitsISO 286 IT6 – IT8
- ThreadsMetric, UN, UNF, NPT
- Machines12
Wire & Sinker EDM
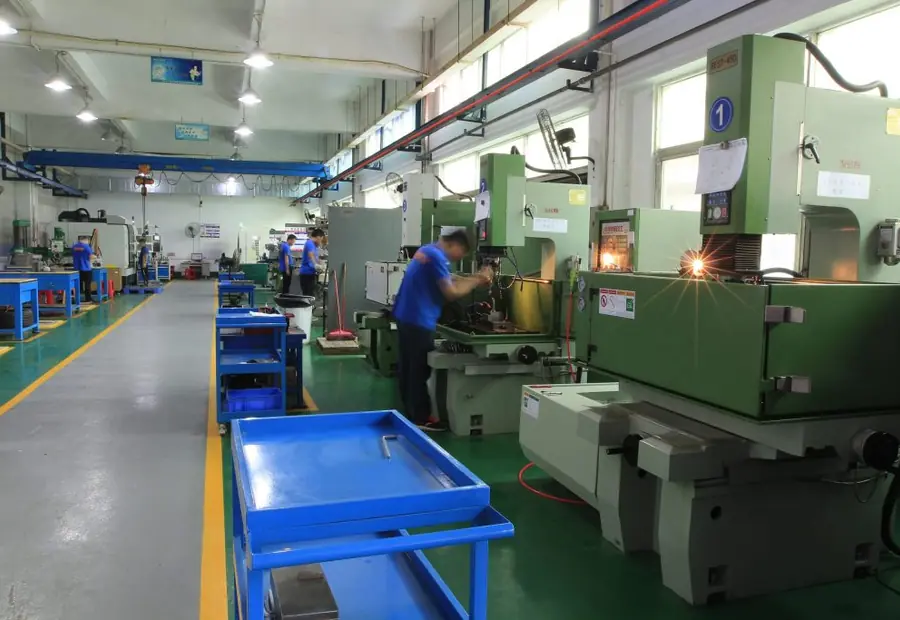
Six wire EDMs and six sinker EDMs for sharp internal corners, hardened tool steel, thin slots, keyways and features a cutter simply cannot reach. Electrodes are made in-house.
- Wire EDM6 machines
- Sinker EDM6 machines
- Typical useHardened steel, dies
- Corner radiusFrom 0.1 mm
Sheet Metal
Punching, bending, forming and welding for enclosures, panels, chassis and brackets — finished and assembled with the machined parts that go inside them.
- Punching machines4
- ProcessesPunch, bend, weld
- MaterialsSteel, stainless, alu
Rapid Prototyping
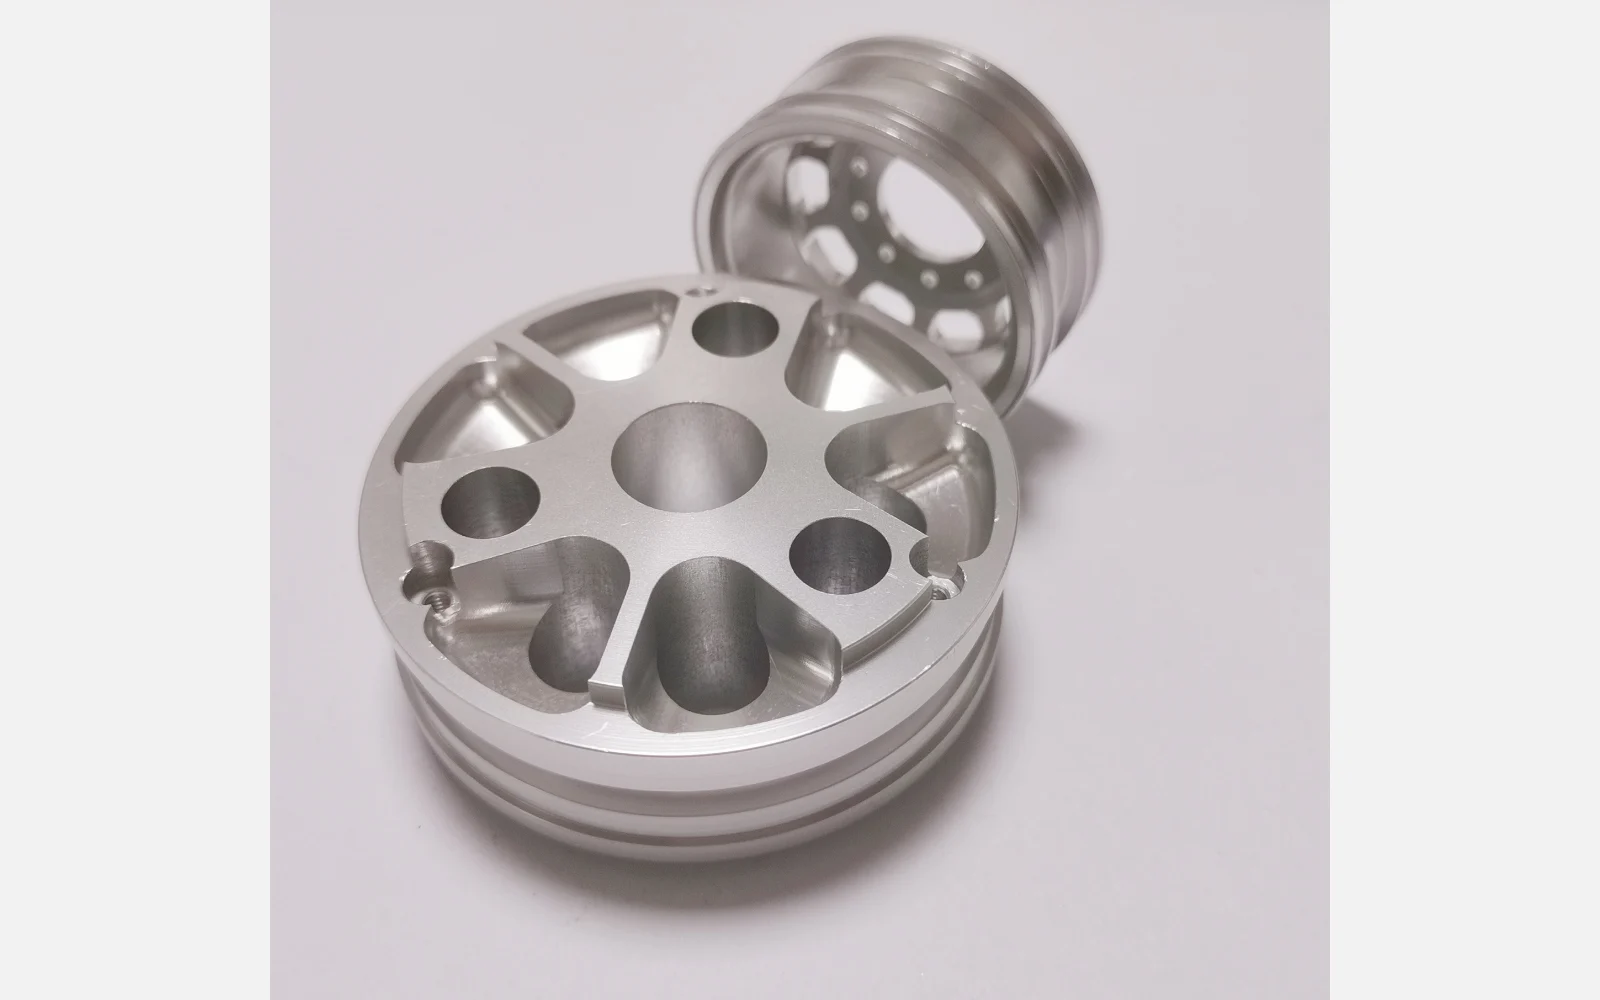
One to fifty pieces, cut from the same machines and measured the same way as production. Send a STEP file and a drawing; you get a price in 16 hours and, for most aluminium and plastic parts, finished pieces on their way within a week.
- Quantity1 – 50 pcs
- Typical lead time5 – 10 working days
- ThenSame tooling for production
Surface Finishing
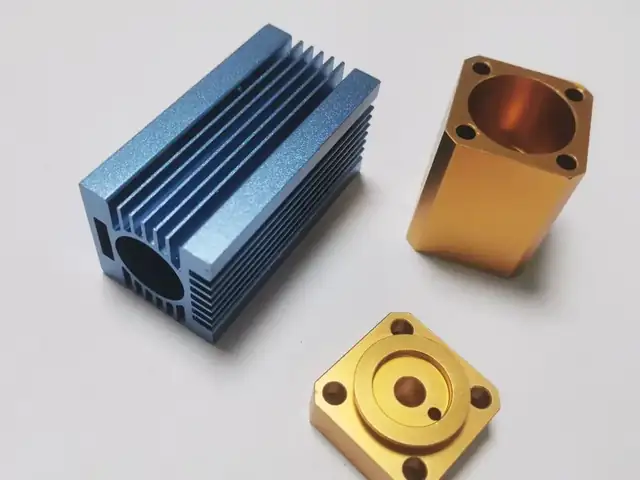
Anodising in clear, black, colour and hard coat, plus plating, powder coating, black oxide, passivation, blasting, brushing, tumbling and hand polishing. All managed by us, on one invoice.
- Finishes offered35+
- AnodisingType II & III
- DeclarationsRoHS / REACH
Which of these sounds like you?
Nobody comes here wanting a machine shop. Pick the thing that is expensive, late or wrong, and we will show you what we do about it.
Four things you get on every order
We are a small factory competing with big platforms. These are the four places we decided not to cut corners.
Your drawings stay in the shop
Files are used to quote and make your parts, nothing else. Never shared with other suppliers, never posted. We sign your NDA before you send anything, or send you ours.
See more →An engineer answers, not a bot
Bill reads every drawing before it is priced. If a tolerance or a feature will double the cost, you hear about it in the quote — not after the first article.
See more →Door to door, tracked
DHL, FedEx or UPS to your dock, or your own forwarder. Commercial invoice and HS codes with every shipment, so nothing sits in customs waiting on paperwork.
See more →If a part is wrong, we fix it
Every first article is measured on the CMM before the run starts. If a toleranced feature is out on delivery, tell us within 14 days — we remake or credit it.
See more →Where our parts end up
Nine industries we have actually machined for. Knives and EDC is the one line where we do the whole product, not just a component.
Automotive
Brackets, adapters, test fixtures, cooling plates and aftermarket components in steel, stainless and 6061/7075.
See more →Electronics & semiconductor
Test fixtures, heat sinks, vacuum-chamber components and precision plates where flatness matters more than looks.
See more →Telecom equipment
Pin-fin heat sinks, RF cavities and filter housings, usually 6061 with a bright or black anodised finish.
See more →Medical devices
Instrument housings, manifold blocks and PEEK or POM components, with dimensional reports on every batch.
See more →Robotics
Joint housings, gearbox flanges, encoder mounts and mounting plates — usually aluminium, usually in a hurry.
See more →Industrial machinery
Replacement parts, jigs, fixtures, shafts and wear components for machines that are already on a factory floor.
See more →Consumer products
Machined housings, hinges, bezels and hardware where surface finish is judged by the person holding it.
See more →Hardware
Fasteners, fittings, knurled parts, split rings and turned components in brass, stainless and titanium.
See more →Knives & EDC
Titanium and G10 scales, liners, clips, pivots, stop pins — and full knife OEM from drawing to finished, assembled product.
See more →100+ materials, 35+ surface finishes
Six material families and more than a hundred grades in regular use, finished in-house or with partners we have used for years. If your drawing calls out an EN, DIN or JIS grade we cross-reference it and confirm the equivalent on the quote. EN 10204 3.1 material certificates on request.
Aluminium
Grades & data →The default for housings, brackets, heat sinks and fixtures: light, fast to machine, anodises well. 7075 when you need near-steel strength.
- MachinabilityExcellent
- FinishesAnodise, bead blast, chromate
- Typical useEnclosures, plates, fixtures
Stainless steel
Grades & data →Corrosion resistance for fittings, valve bodies, medical and food-contact parts. 303 for volume turning, 316L for marine and chemical, 17-4 PH when it must be hard.
- MachinabilityFair to good
- FinishesPassivate, electropolish, bead blast
- Typical useFittings, shafts, manifolds
Brass & copper
Grades & data →Brass for fittings, knurled parts and decorative hardware; copper when thermal or electrical conductivity is the point.
- MachinabilityExcellent (C360)
- FinishesPolish, plate, black oxide
- Typical useFittings, contacts, heat spreaders
Titanium
Grades & data →Half the weight of steel with the same strength, and it does not corrode. Slower to cut, so we run it with the right tooling and coolant rather than fast.
- MachinabilitySlow, well understood here
- FinishesStone-wash, anodise (colour), blast
- Typical useKnife scales, aerospace-style brackets
Steel & tool steel
Grades & data →Mild and alloy steels for shafts, gears and structural parts; tool steels heat-treated and finished on wire EDM or by grinding.
- MachinabilityGood (annealed)
- FinishesBlack oxide, zinc, nitride, paint
- Typical useShafts, gears, dies, wear parts
Engineering plastics
Grades & data →Machined, not moulded, so one piece costs the same per part as a hundred. Delrin for precision, PEEK for heat and chemicals, PTFE for low friction.
- MachinabilityExcellent to good
- FinishesAs-machined, bead blast
- Typical useBushings, insulators, medical
Every part measured before it ships
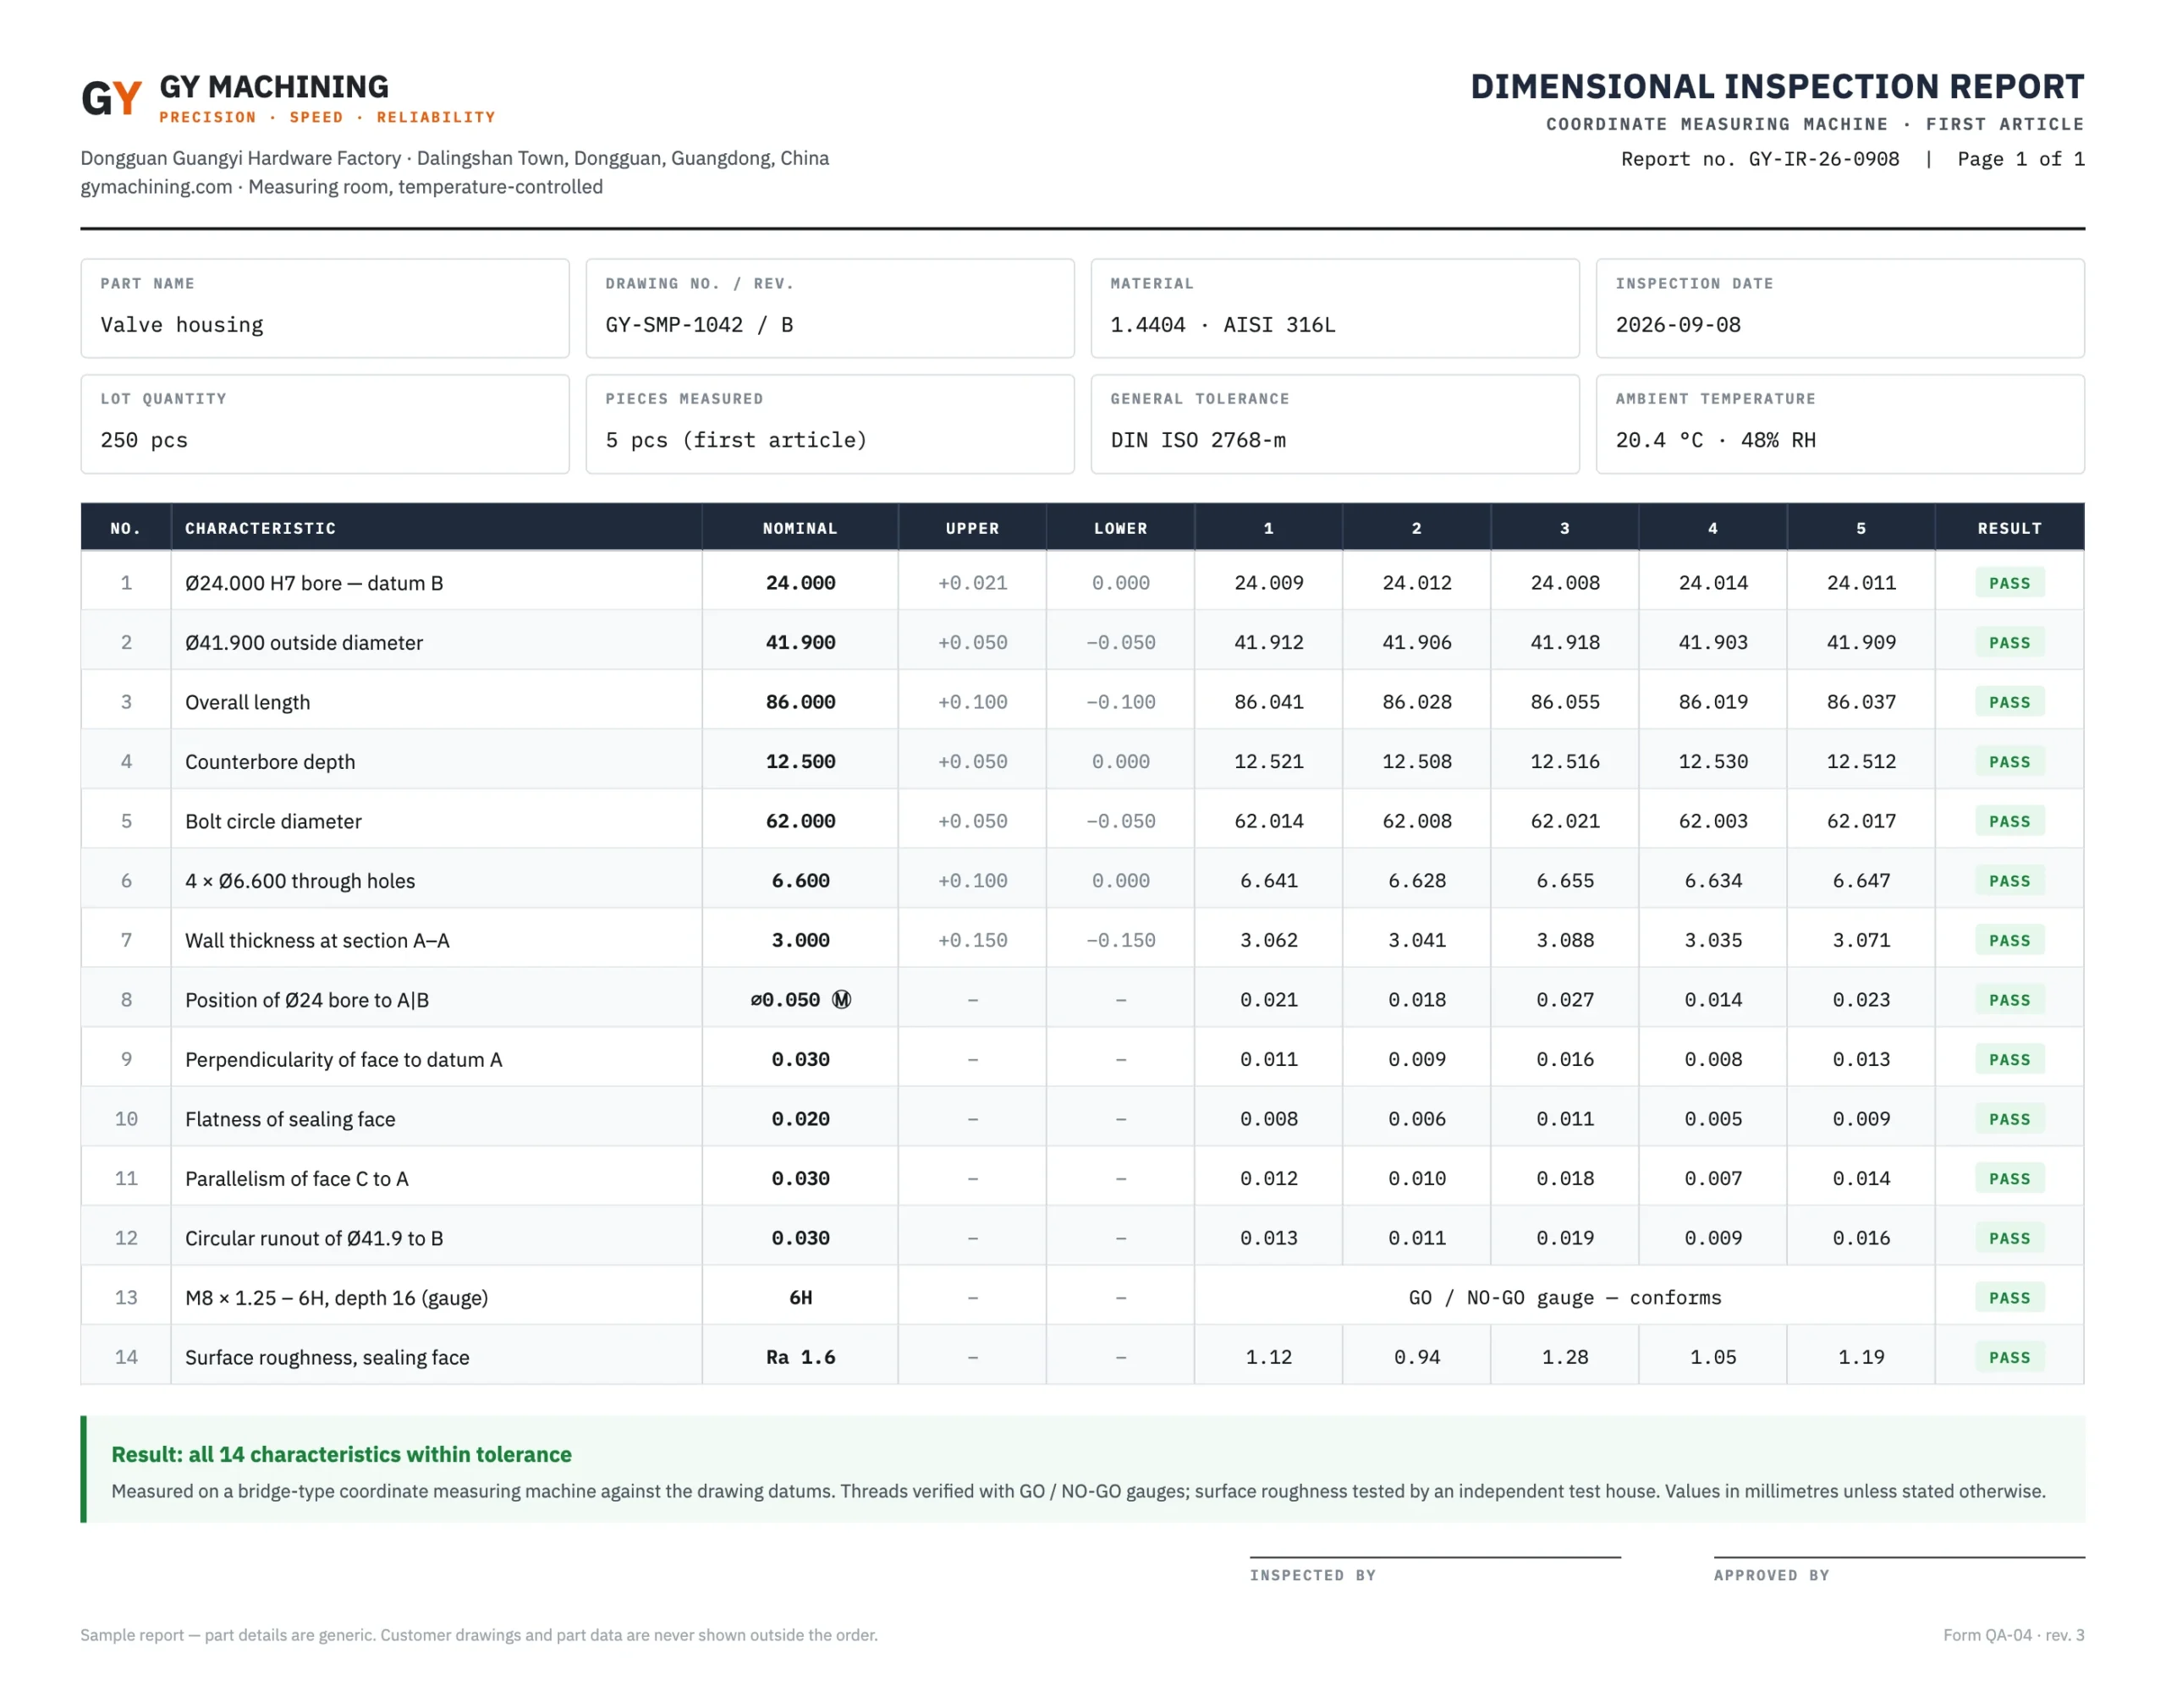
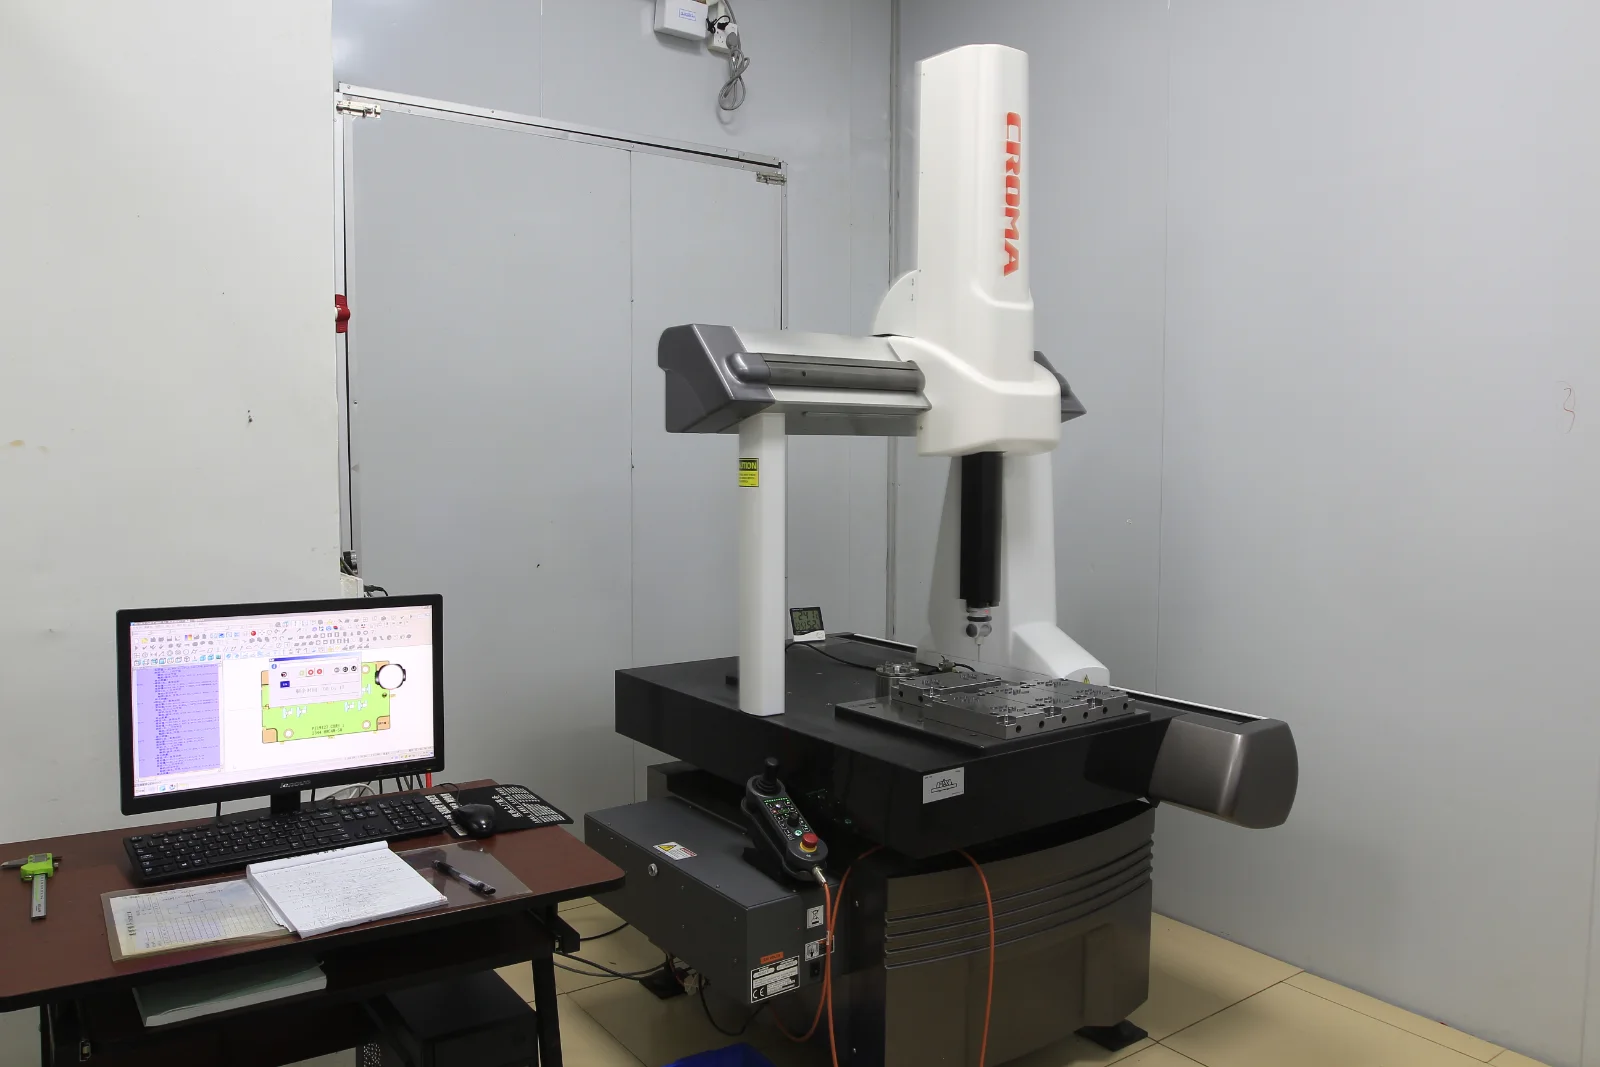
A temperature-controlled measuring room, a first article checked on the CMM before the rest of the run is cut, and a dimensional report with the values we actually measured. We are not ISO 9001 certified — we would rather tell you here than have you find out later.
Material checked in
Grade and heat number confirmed against the mill certificate before bar or plate reaches a machine. Where the drawing calls for a hardness, it is verified by an independent test house. EN 10204 3.1 certificates on request.
Checked at the machine
Operators measure critical features between operations with gauges and micrometers, so a drifting tool is caught in minutes, not at final inspection.
First article on the CMM
The first piece of every run is measured on a bridge-type CMM against your datums. The run only continues once it passes.
Report with the parts
One page per part: nominal, tolerance, measured value and deviation for every toleranced feature. Unmarked dimensions to ISO 2768-mK.
Surface finish and thread check
Roughness measured by an independent test house where Ra is called out; threads verified with GO / NO-GO gauges; plated and anodised parts checked for coating thickness and colour against the approved sample.
Final inspection and packing
100% visual check on every piece, sampled dimensional check on the batch to AQL, then parts packed in trays or foam with the report, packing list and photos sent to you before the box is sealed.
Three people, start to finish
No account managers and no ticket numbers. The owner, the engineer and your coordinator quote your part, follow it through the shop and ship it.
Will
Founder & General ManagerBought the first machining centre in 2008 and still walks the floor every day. Decides what we can and cannot take on.
Eileen
Project CoordinatorYour first and last contact. Quotes, order status, photos before shipment and the tracking number afterwards.
Bill
Engineering ManagerReads every drawing before it is priced, writes the DFM notes and signs off the first-article report.
Inside our factory
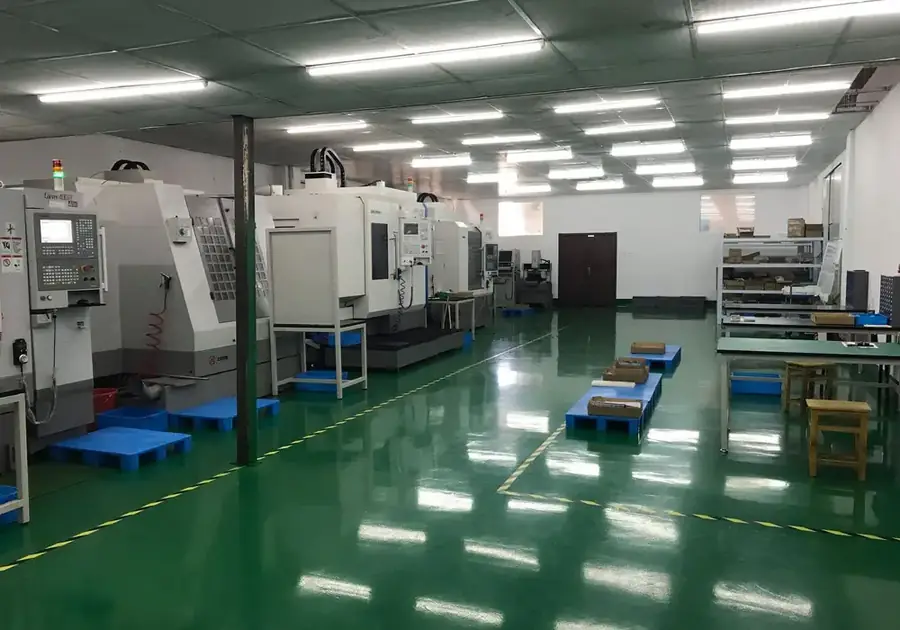
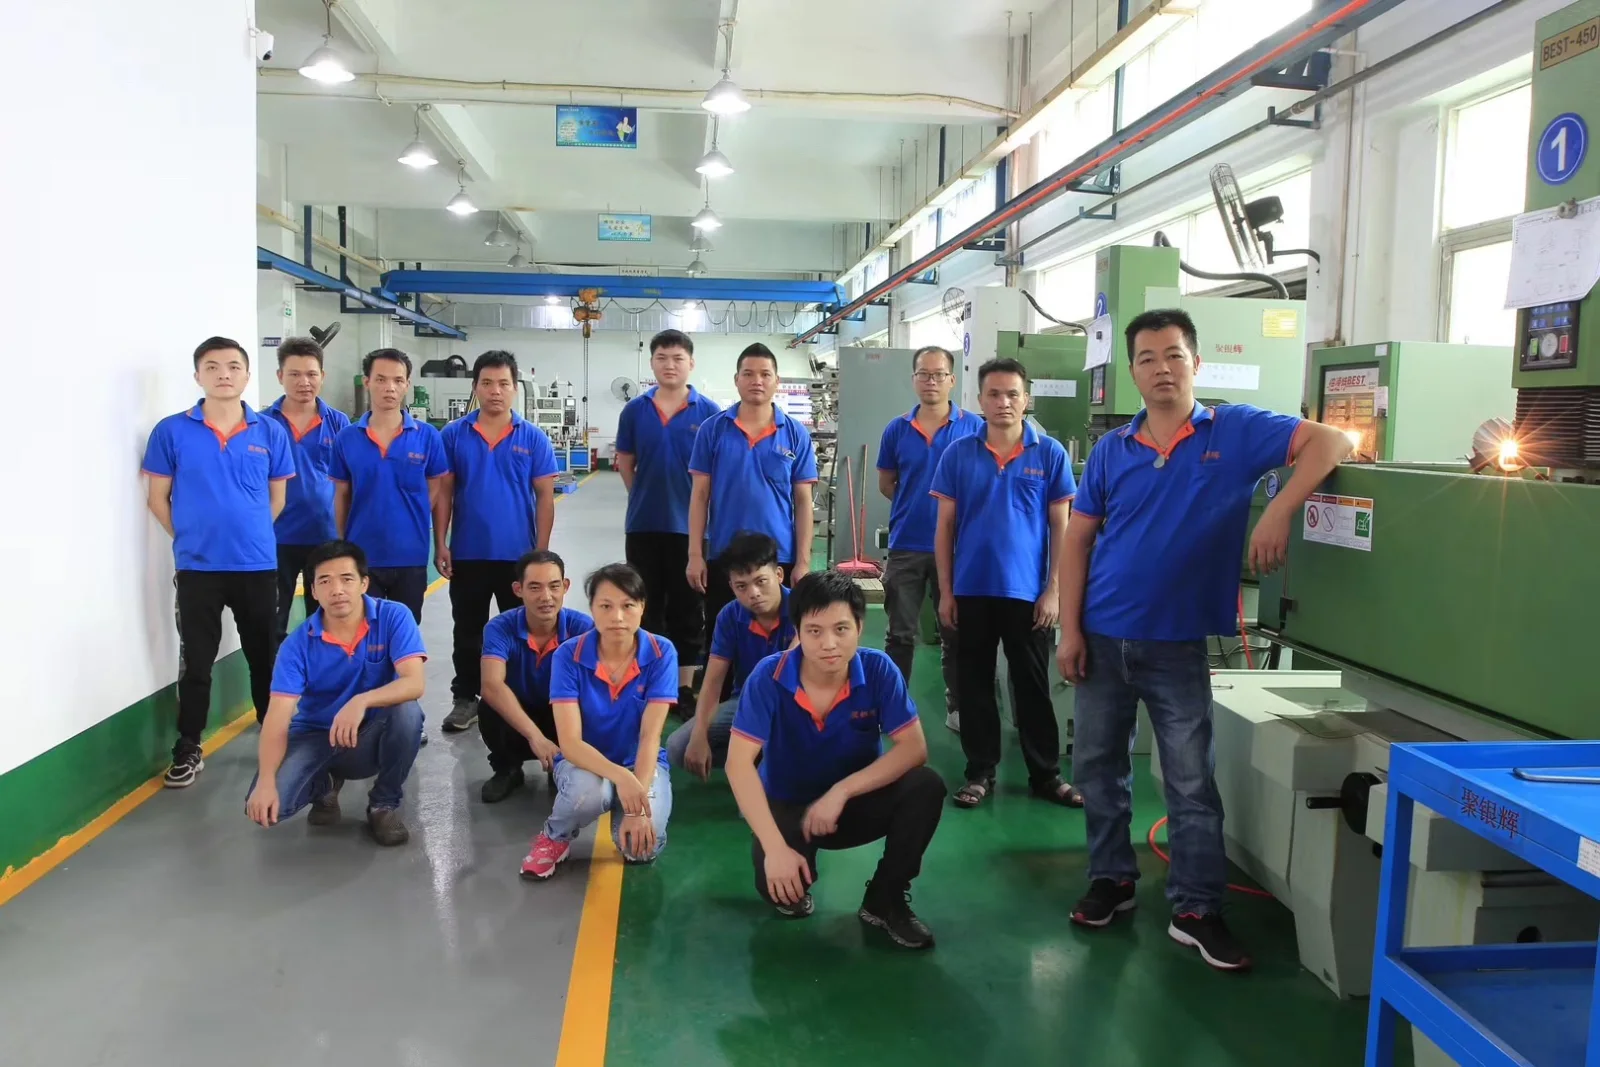
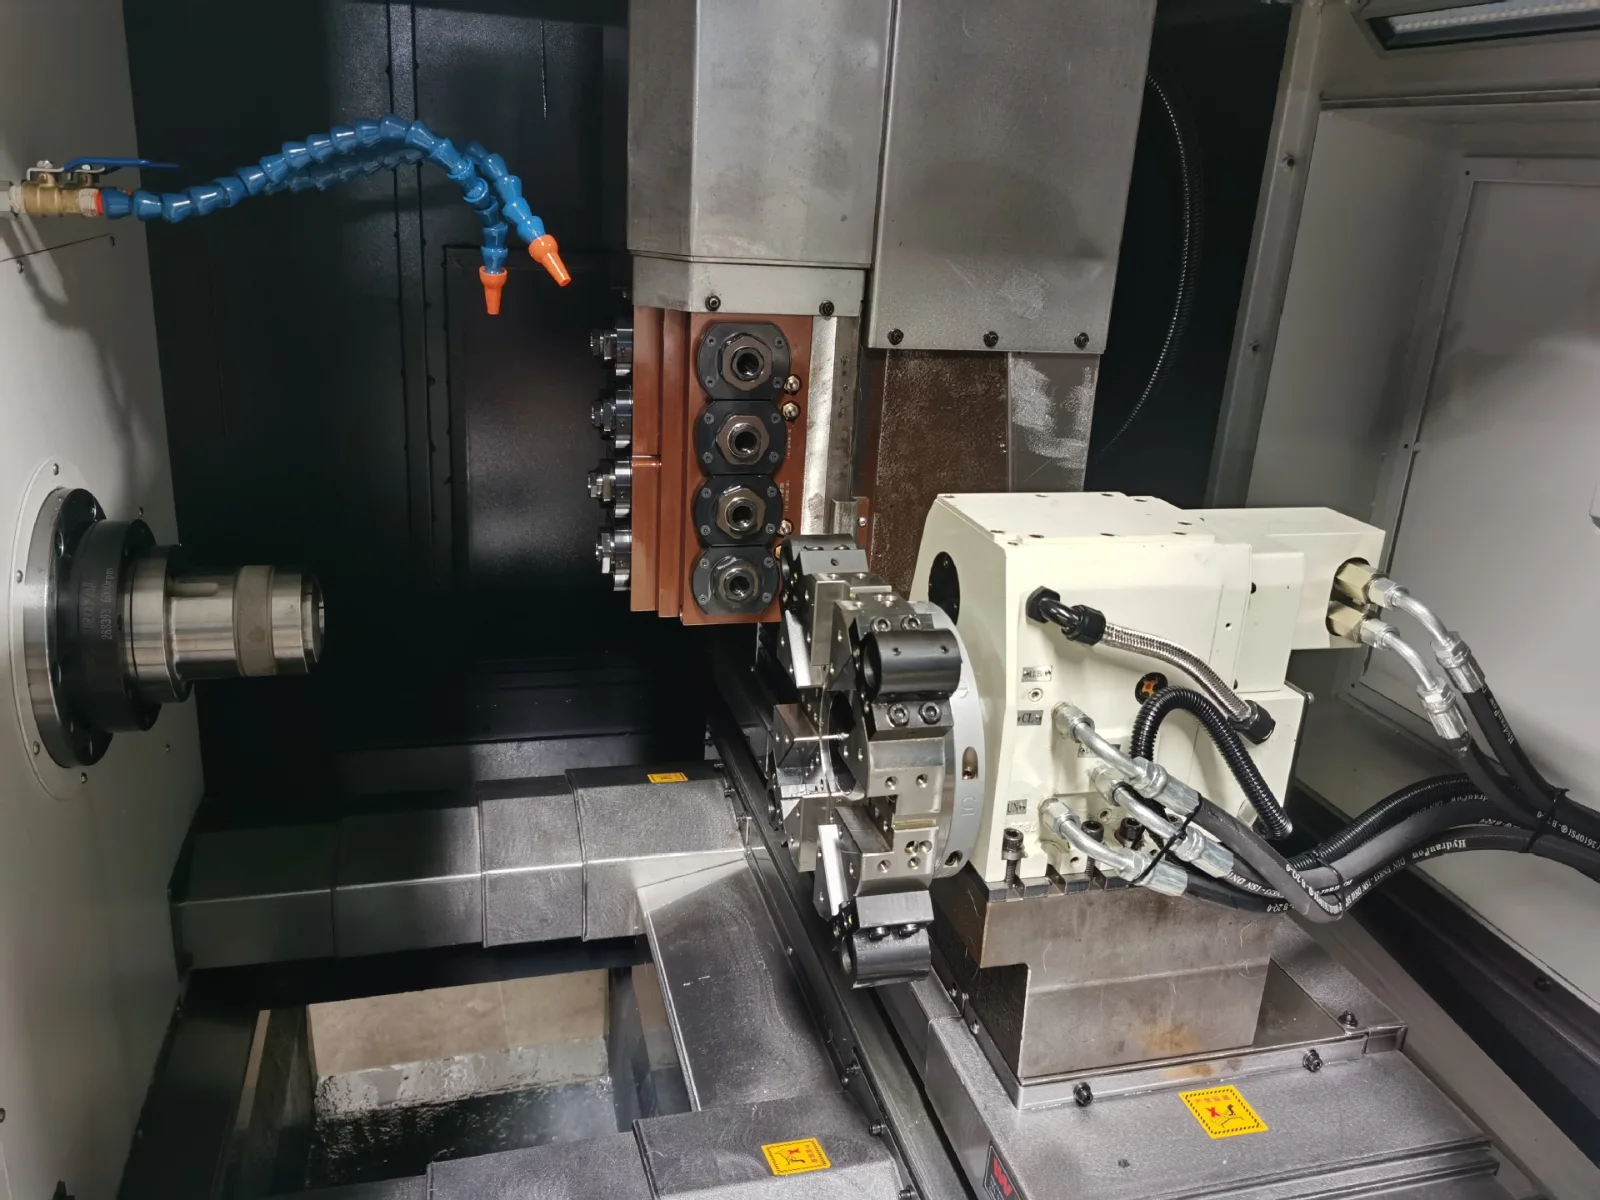
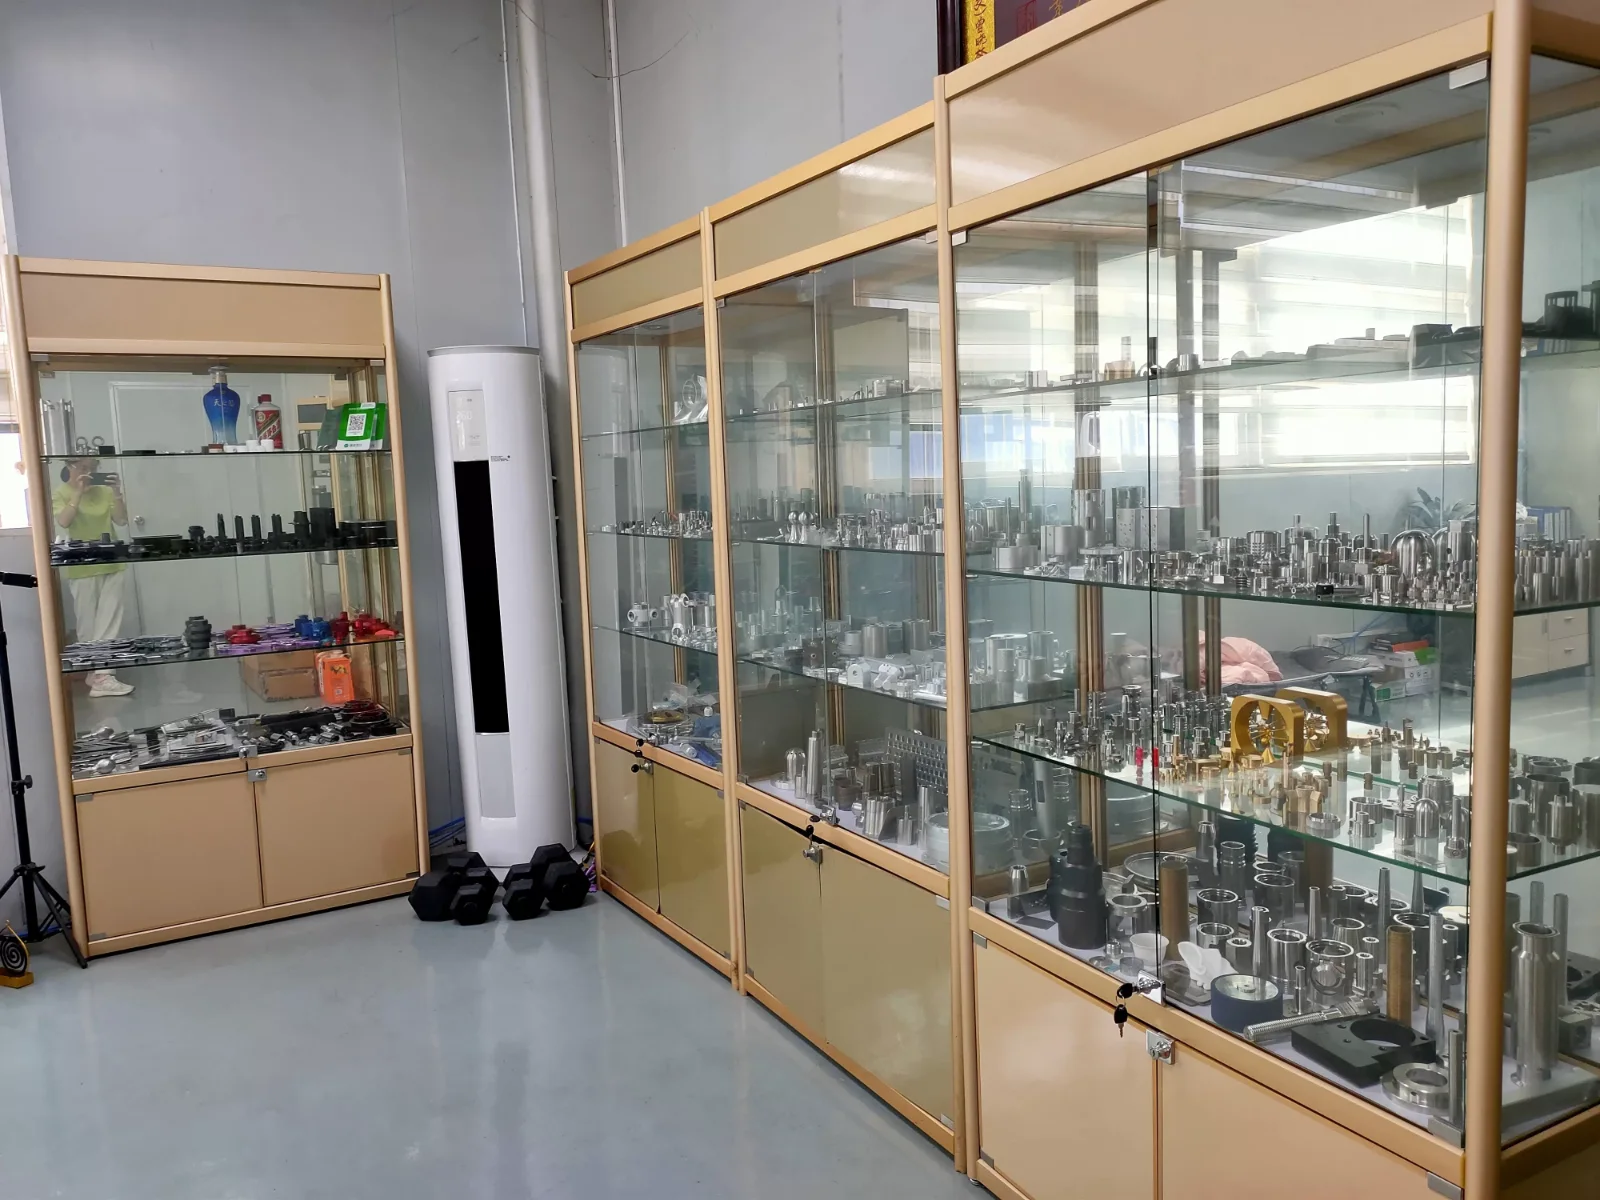
Dongguan Guangyi Hardware Factory runs 32 machining centres, 12 CNC lathes and 12 EDM machines under one roof in Dalingshan, with a temperature-controlled measuring room and a sample room full of the custom parts we have made for customers in 11 countries. Small enough that the owner still checks the drawings; big enough to run 10,000 pieces.
Send the drawing. You will have a price and a lead time in 16 hours.
STEP, IGES, X_T, DWG, DXF or PDF. Metric or inch. No minimum order.
Questions we get every week
What tolerance can you actually hold?
Do you have a minimum order quantity?
How fast is a quote, and how fast are parts?
You are not ISO 9001 certified — why should I trust the parts?
Will you sign an NDA before I send drawings?
Do you machine 5-axis parts?
Can you do assembly and finishing as one order?
How do parts get to me, and who pays duty?
CNC machining resources
Design guides, tolerance charts and answers to the questions we get on drawings every week.