CNC Machining for Consumer Products
Machined housings, hinges, bezels, buttons and hardware where the surface finish is judged by the person holding the product, not by a gauge. Anodising, plating and polishing handled here on one invoice.
Problems buyers bring us in this sector
On consumer parts the tolerance is rarely the problem — the finish is. These three complaints account for most rejected batches we have ever seen.
“The second batch does not match the first”
Anodising colour drifts between dye lots. We run matching parts in one lot wherever quantity allows, and keep a retained sample from the approved batch. Send a physical sample to match, not a Pantone number — the alloy and the etch change the result.
“There is a clamp mark on a visible face”
Mark the cosmetic faces on the drawing and we plan the workholding around them, clamping on faces that will be hidden or machined away. If every face is cosmetic, we say so and quote the extra handling.
“The edges feel sharp in the hand”
We break edges 0.2–0.3 mm as standard unless the drawing says otherwise, and tumble or blast where the design allows. Tell us which edges must stay crisp — a chamfer on the wrong edge is as much a defect as a burr.
What we machine for consumer product brands
On consumer parts, cosmetic consistency is usually harder than the tolerance. We finish in batches, from one anodising lot where we can, so parts in the same assembly match.
Housings and enclosures
Milled aluminium bodies and covers with a consistent brushed or bead-blasted surface.
Hinges and mechanisms
Turned and milled pivot parts where the action has to feel right, not just measure right.
Bezels, rings and trim
Cosmetic parts with a diamond-turned or polished face and a tight colour match batch to batch.
Buttons, knobs and dials
Knurled and machined controls in aluminium, brass and stainless.
Speaker and vent grilles
Fine hole patterns and slots milled into thin plate without burrs on the visible face.
Stands, mounts and bases
Weighted machined bases in steel and brass, finished to hide the machining marks.
What these parts are usually made from
Aluminium for almost everything cosmetic, brass and stainless where weight and feel sell the product.
What we watch on a consumer drawing
Colour match, edge quality and no witness marks
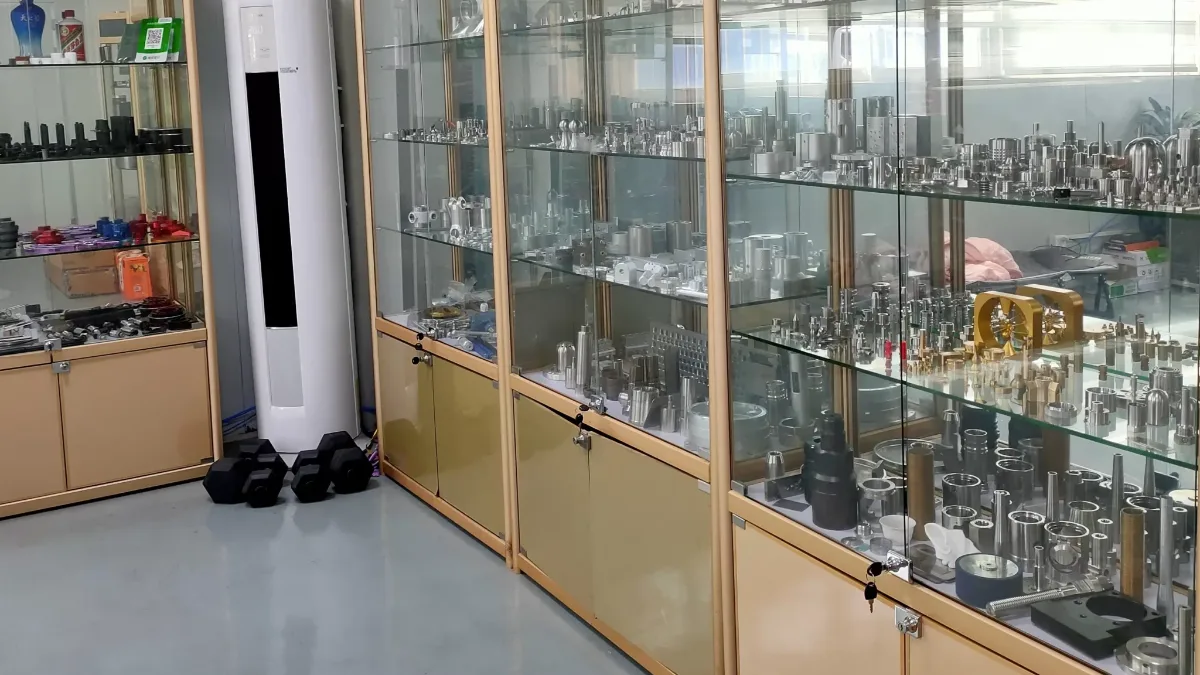
Three things get consumer parts rejected: colour drift between anodising lots, a sharp or ragged edge where a hand touches the part, and a witness mark from a clamp on a visible face. We plan the workholding around the cosmetic faces and finish matching parts in one lot.
- Anodising colourMatched within a lot
- Edge break0.2 – 0.3 mm unless drawn otherwise
- Surface finish, bead blastUniform, no directional marks
- Achievable, milled±0.002 mm
- Cosmetic facesMarked on the drawing, clamped elsewhere
- Sample before runYes, on request
What buyers in this industry ask
Can you match a colour we already have?
Will every part in the batch look the same?
Can you supply a sample before the full run?
How we make them
CNC Milling
Housings, plates and brackets on 2/3/4-axis centres. CNC milling →
CNC Turning
Shafts, bushings and fittings on twelve lathes. CNC turning →
Inspection
First article on the CMM before the run continues. Quality →
Send the drawing. You will have a price and a lead time in 16 hours.
STEP, IGES, X_T, DWG, DXF or PDF. Metric or inch. No minimum order.