CNC Machining for Telecom Equipment
Pin-fin heat sinks, RF cavities, filter housings and enclosure hardware, usually in 6061 with a bright or black anodised finish. This is the sector where we know exactly where our parts ended up.
Problems buyers bring us in this sector
Telecom is the sector where our customers have told us what the parts are for, so we know exactly where these three problems come from.
“The filter tunes out of band”
Cavity depth and wall thickness decide the passband. We hold both to the drawing and put the measured values in the first-article report, so you can correlate them with your network analyser results instead of guessing which cavity moved.
“Plating pushed the part out of tolerance”
We take the plating allowance out of the machined dimension. Tell us the plating specification and thickness in the RFQ and it is the finished, plated part that lands in tolerance — not the raw one.
“The heat-sink fins keep coming out wrong”
In 6061 we hold fins down to about 0.8 mm with a 1.5 mm gap, depending on height. If your geometry is past what milling can do without chatter, we say so and point you to skiving or extrusion rather than quote something we cannot make well.
What we machine for telecom customers
Telecom is the one industry where our customers have told us what the parts are for, so the examples below are real rather than generic.
Pin-fin heat sinks
Milled fin arrays in 6061 with a flat, lapped base for the power device.
RF cavity filters
Milled cavities and tuning posts where wall thickness and cavity depth decide the passband.
Filter and duplexer housings
Machined housings with silver-plated interiors and sealed covers.
Antenna mounting hardware
Brackets, clamps and adapters in aluminium and stainless, usually anodised or powder coated.
Waveguide components
Flanges and transitions machined to the drawing with sealing faces held flat.
Enclosure and chassis parts
Milled and sheet-metal enclosures, gasket grooves cut to your seal specification.
What these parts are usually made from
6061 for almost everything, copper and brass where conductivity decides it, stainless outdoors.
What we watch on a telecom drawing
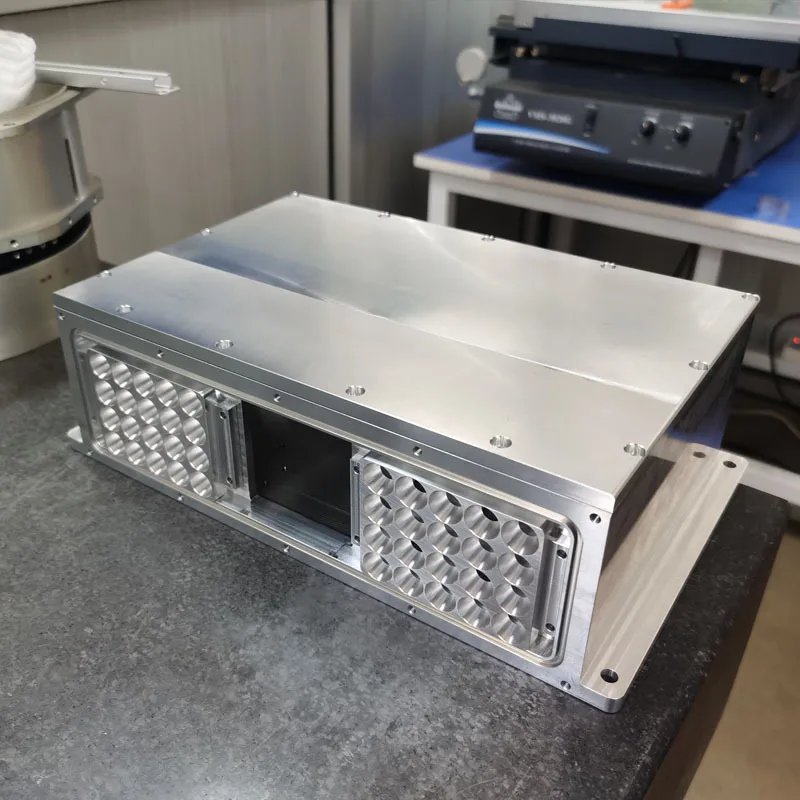
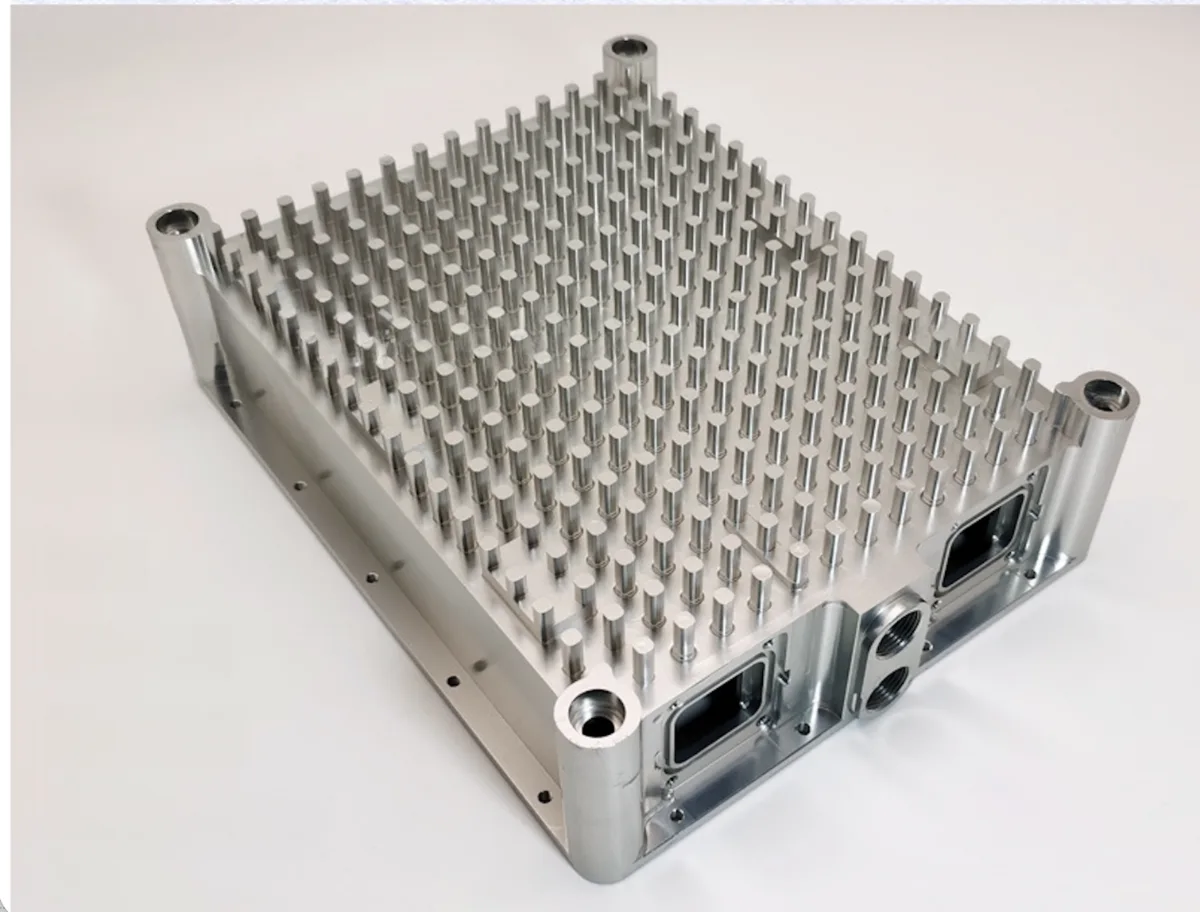
Enclosures, cavities and heat sinks that have to seal, shield and cool
The two parts on the left are typical: a milled enclosure whose cover has to seal flat and whose vent panels are cut from solid, and a one-piece chassis with a full field of pin fins for cooling. On RF hardware the electrical performance follows the geometry, so cavity depth and wall thickness are usually tighter than anything else on the drawing. Plating thickness matters too — tell us the specification and we will hold the machining tolerance with the plating allowance already taken out.
- Cavity depth tolerance±0.01 mm achievable
- Wall thickness, minimum0.8 mm in 6061
- Flatness, sealing faces0.03 mm over 100 mm
- Achievable, milled±0.002 mm
- Plating allowanceMachined in, on request
- Unmarked dimensionsISO 2768-mK
What buyers in this industry ask
Do you machine RF cavity filters to a tuning specification?
Can you plate the inside of a filter housing?
What is the thinnest fin you can machine on a heat sink?
How we make them
CNC Milling
Housings, plates and brackets on 2/3/4-axis centres. CNC milling →
CNC Turning
Shafts, bushings and fittings on twelve lathes. CNC turning →
Inspection
First article on the CMM before the run continues. Quality →
Send the drawing. You will have a price and a lead time in 16 hours.
STEP, IGES, X_T, DWG, DXF or PDF. Metric or inch. No minimum order.