CNC Machining Acetal and POM
Acetal is the plastic a machinist reaches for by default. It is stiff, it holds its size, it cuts to a clean shiny finish without fuss, and it is inexpensive. If a part does not need high temperature or chemical resistance, acetal is usually the right answer and the argument stops there.
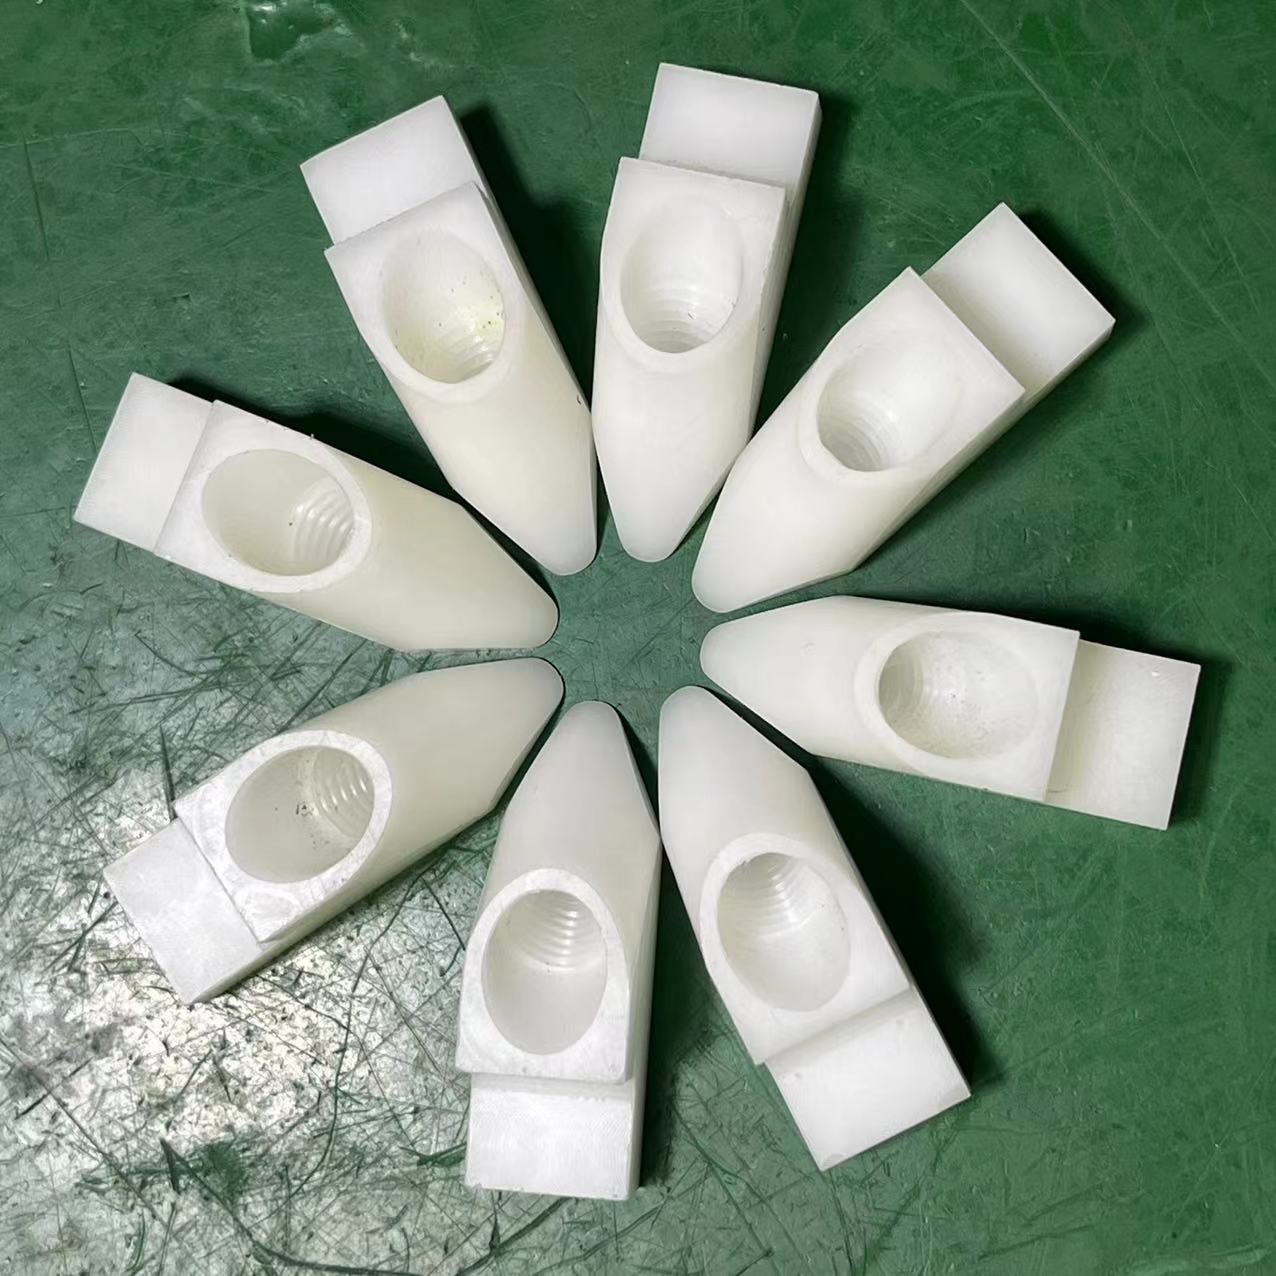
The two grades that matter
Acetal, POM and polyoxymethylene all name the same family. Within it there are two forms — homopolymer and copolymer — and if your drawing says Delrin, that comparison is worth reading on its own page. Delrin vs acetal copolymer →
| Grade | Best for | Notes |
|---|---|---|
| Homopolymer (POM-H) | Stiffness, strength and wear — gears, cams, loaded parts | Sold under the Delrin brand among others. Stiffer than copolymer, but can carry porosity down the centre of thick bar |
| Copolymer (POM-C) | Dimensional stability and chemical resistance, thick sections | More stable in hot water and alkaline conditions, no centre porosity, usually the safer choice for large machined blocks |
| Glass-filled acetal | Higher stiffness and lower thermal expansion | Abrasive to tooling; worth it when stiffness or stability drives the design |
| Acetal with PTFE | Low-friction bearing and sliding parts | Runs against metal without lubrication |
The plastic that behaves
Acetal cuts cleanly at high speed, breaks into proper chips instead of stringing, and leaves a surface straight off the tool that most plastics need a second operation to reach. It holds tolerance better than nylon because it barely absorbs moisture, and it stays stiff at room temperature where softer plastics creep.
Its limits are real but narrow: it softens well below 100 °C under load, it is attacked by strong acids, and it is close to impossible to bond — parts are designed to be screwed, snapped or pressed together rather than glued. It also burns readily, which matters in some enclosures.
For anything tightly toleranced we still rough, let the part relax and then finish, because extruded stock carries internal stress like any other plastic.
| At a glance | |
|---|---|
| Service temperature | Around 80–100 °C, lower under sustained load |
| Moisture absorption | Very low — the reason it holds size better than nylon |
| Machinability | The best of the engineering plastics |
| Bonding | Very poor — design for mechanical fastening |
| Typical parts | Gears, bushings, manifolds, rollers, insulating blocks, fixture components |
Three notes on acetal parts
Choose copolymer for thick sections and wet service
Homopolymer can carry porosity in the middle of a thick bar, and it is less happy in hot water and alkaline conditions. If you are machining a large block, or the part gets washed down, copolymer avoids both problems. The full comparison →
Do not plan to glue it
Acetal resists adhesives almost as well as it resists chemicals. Screws, press fits and snap features work; glue generally does not.
Give it a realistic tolerance
Acetal is the most stable common plastic, but it is still plastic. Mark which dimensions are functional and we will hold those and leave the rest sensible.
Finishes that work on acetal (pom)
Acetal is normally used exactly as machined — the finish off the tool is already good.
Finishing is done by partner shops we specify and inspect for — we do not run plating or coating tanks ourselves. How we handle finishing →
Send the acetal drawing
Send the drawing and the grade, or the drawing and a sentence about what the part has to survive. You get a price, a lead time, and an engineer’s note on anything that will fight the tolerances.