Precision CNC Machining Services
CNC milled, turned, and EDM components for prototypes, low-volume production and repeat orders.
- ISO 2768-m by default; ISO 2768-f on request
- ISO 286 fits — IT8, IT7, IT6, gauged or measured on the CMM
- Tighter tolerances — mark the drawing, we quote to it
- EN 10204 3.1 material certificates on request
Our Capabilities
GY provides high-quality CNC machined parts that meet your specifications and exceed your expectations. As an experienced CNC machining manufacturer, we make custom metal machined parts in aluminium, brass, stainless steel, copper, steel and more. Our capabilities also include CNC plastic machining in materials such as Delrin (POM), Nylon and PEEK. Our engineering and production staff provide CNC machining services to clients worldwide from our facility in Dongguan City, supported by a company-wide commitment to quality and customer satisfaction.
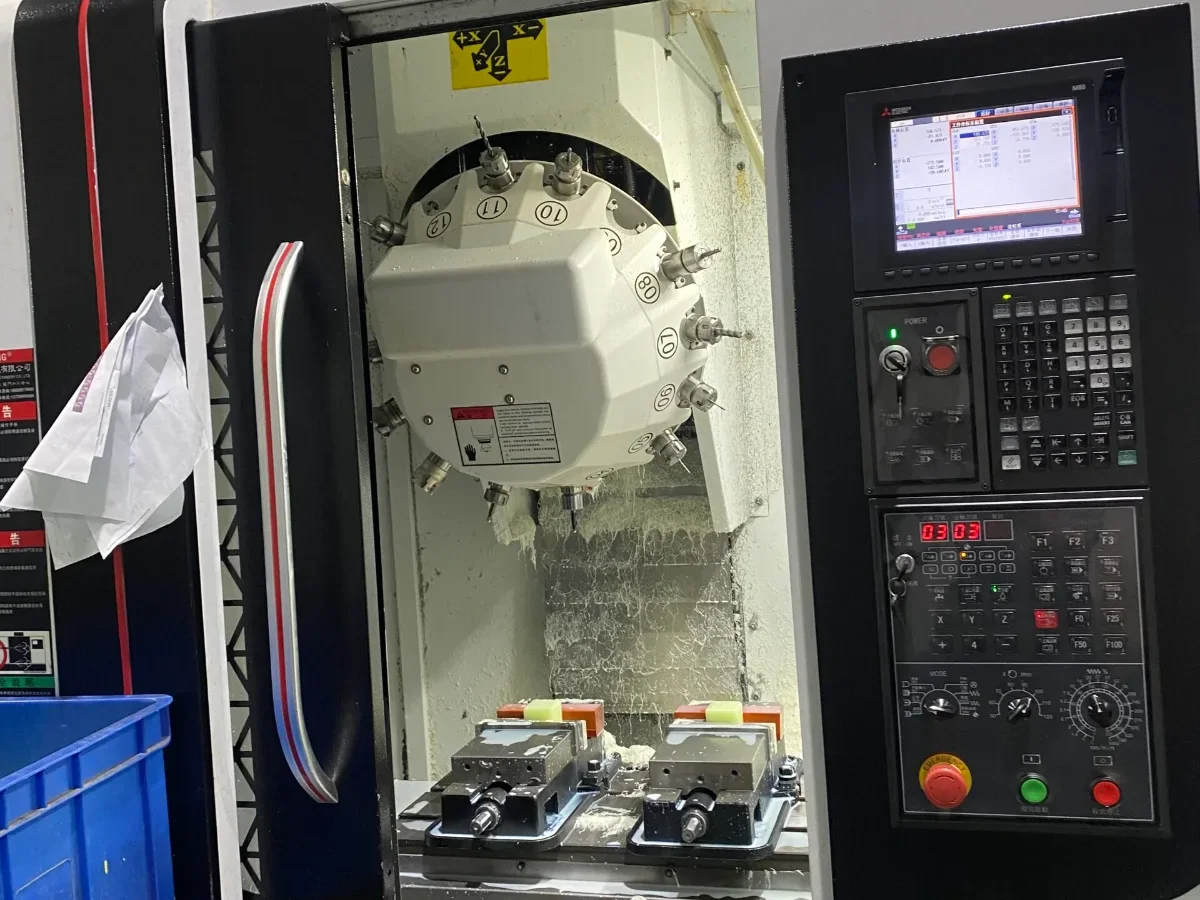
CNC Milling
Housings, brackets, manifolds, plates and fixtures on 32 vertical machining centres — 19 four-axis and 13 three-axis, up to 800 × 600 × 500 mm. A 4-axis rotary presents four faces in one setup, so hole patterns and cross-features hold position without refixturing. No simultaneous 5-axis in-house — if a part needs it, we can have it quoted by a five-axis partner shop and coordinate the job for you.
- Machines32 (19 four-axis)
- Envelope800 × 600 × 500 mm
- Tolerance±0.002 mm on critical features
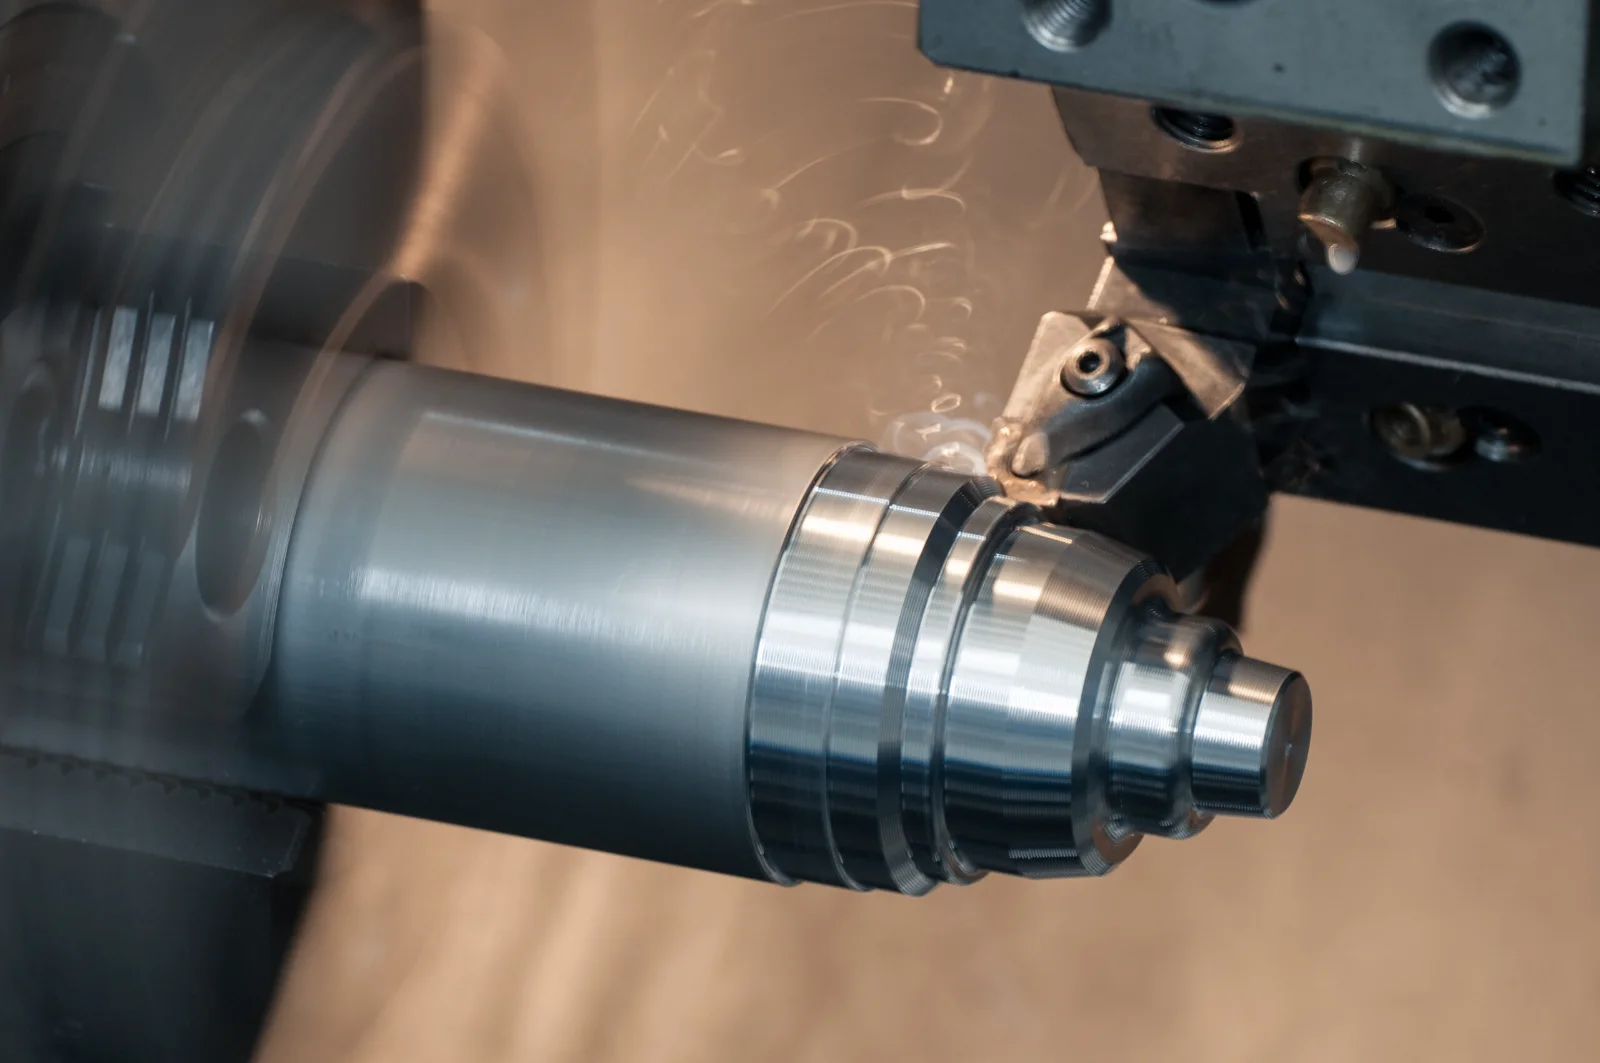
CNC Turning
Shafts, bushings, sleeves, fittings and threaded parts from Ø1 to 250 mm on eighteen CNC lathes, ten of them Swiss-type. Live tooling and a sub-spindle cut cross-holes, flats and keyways in the same setup, so concentricity is held to 0.01–0.03 mm TIR instead of depending on a second chucking. Threads cut or rolled, gauged GO / NO-GO.
- Machines18 lathes
- DiameterØ 1 – 250 mm
- FitsISO 286 IT6 – IT8
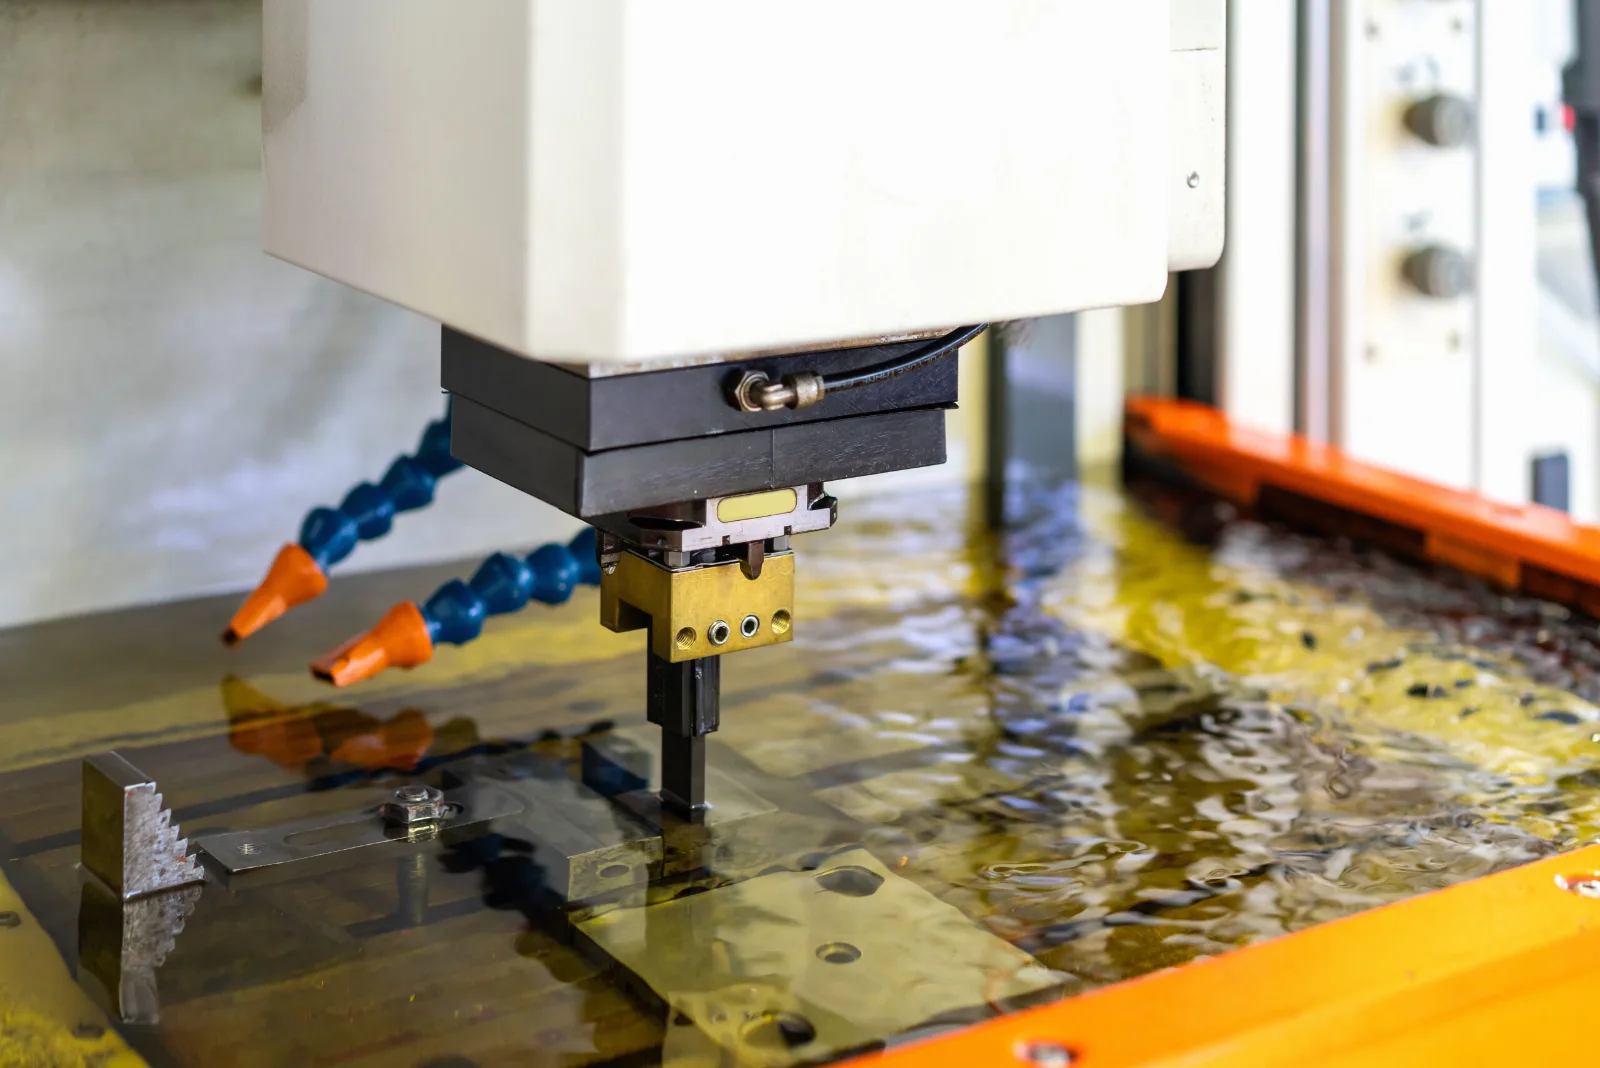
EDM Machining
Wire EDM cuts hardened tool steel, thin webs and sharp internal corners a cutter cannot reach — after heat treatment, so nothing moves afterwards. Sinker EDM burns blind pockets, deep ribs and mould detail with a graphite or copper electrode. Electrodes are made in house.
- Machines6 sinker in-house · wire at partner
- Wire tolerance±0.002 mm
- Sinker finishRa 0.4 – 3.2 µm
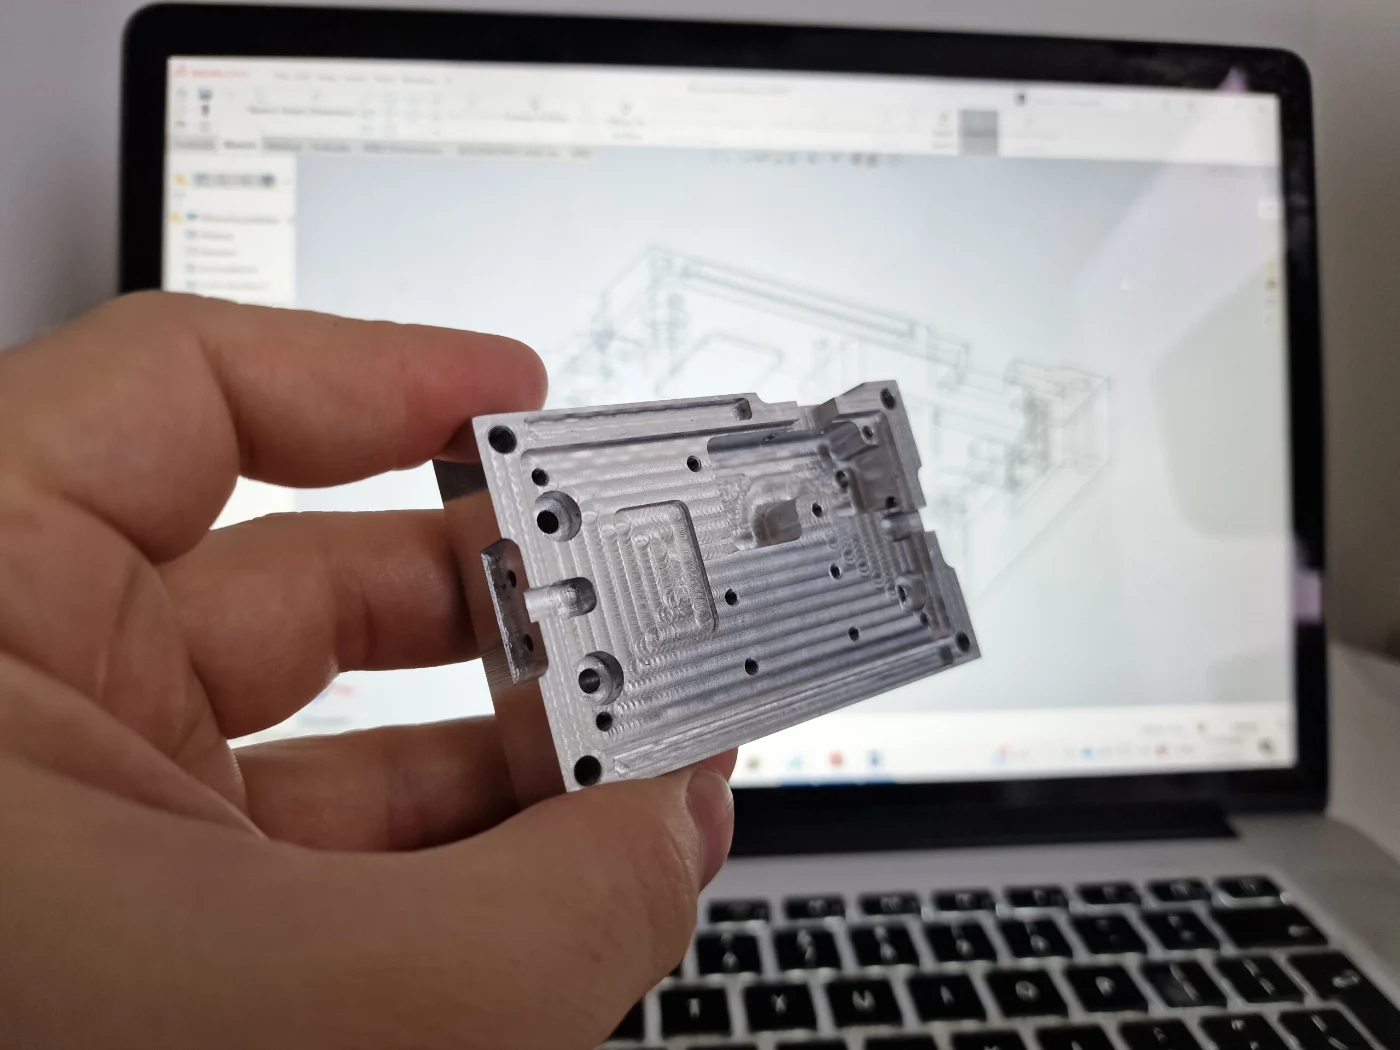
Prototyping & DFM
One to ten pieces, machined the same way production will be, so the first article tells you something true. Before we cut, an engineer reads the drawing and sends back what would make the part cheaper or more reliable — free, and without changing anything you did not agree to.
- Quantity1 – 10, no minimum
- DFM reviewFree, within 16 h
- ThenSame programme scales to production
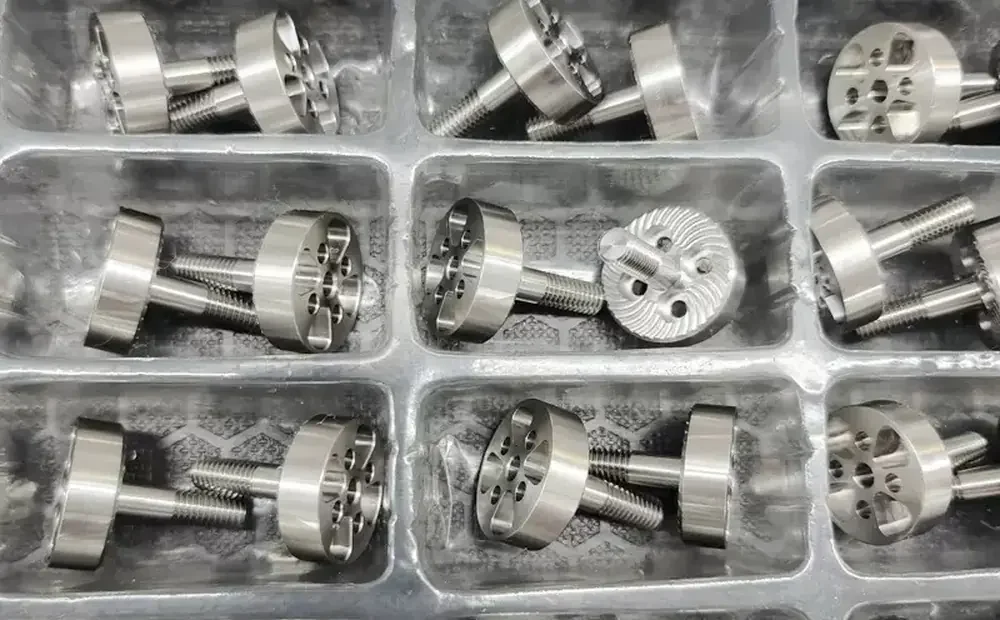
Assembly & Kitting
Machined, turned, sheet metal and finished parts brought together in our building: pressed-in inserts, sub-assemblies, kitted sets, one packing list. If two parts have to fit, we check the fit here before they ship.
- Sub-assemblyInserts, fasteners, fits checked
- PackingTrays, foam, kitted by set
- ShippingOne order, one date
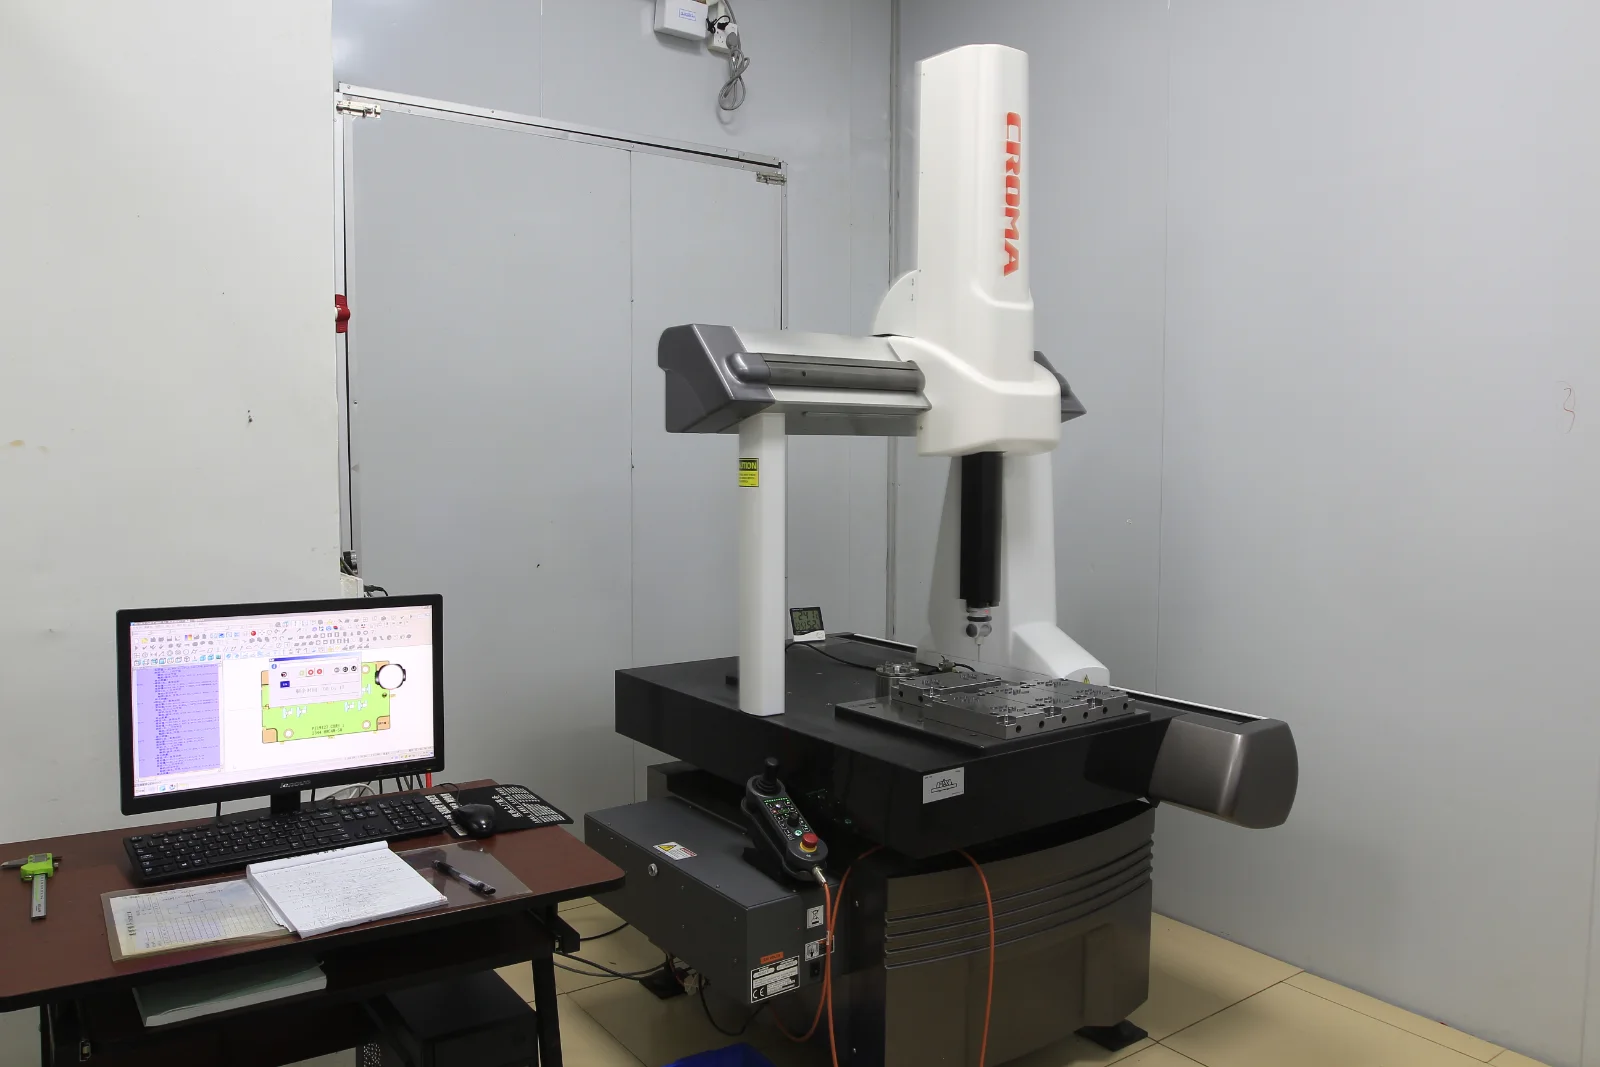
Inspection & Reports
First article on a bridge CMM, in-process gauging at the machine, and a dimensional report against the drawing with every batch. Certificates and surface-roughness tests through an independent lab when the drawing calls for them.
- CMMBridge type, measuring room
- Every batchDimensional report
- On requestEN 10204 3.1, Ra, hardness
What each process actually holds
Real figures, not marketing ones. Unmarked dimensions are ISO 2768-mK; the values below are what we hold on features you call out, and they are the figures we quote to — not the best day we ever had.
| Process | Metals | Plastics | Surface finish | Where it is checked |
|---|---|---|---|---|
| CNC milling | ±0.002 mm | ±0.10 mm | Ra 0.8 – 3.2 µm | CMM on first article; gauges in process |
| CNC turning | ±0.002 mm · IT6 – IT8 fits | ±0.10 mm | Ra 0.4 – 3.2 µm | Runout 0.01 – 0.03 mm TIR on the machine |
| Wire EDM | ±0.002 mm | — | Ra 0.4 – 1.6 µm | Hardened steel; 0.1 mm internal corner radius |
| Sinker EDM | ±0.002 mm | — | Ra 0.2 – 1.6 µm | Blind pockets, ribs and sharp internal corners |
| Grinding Partner | ±0.002 mm | — | Ra ≤ 0.2 µm | Hardened shafts and flat ground faces; inspected on return |
- Unmarked dimensionISO 2768-mK
- Marked dimensionHeld to the value on the drawing
- Tighter than listedAsk — often possible, quoted per feature
- PlasticsWider, because they move with heat and moisture
- ProofFirst article on the CMM, report with the batch
A tolerance is only as good as the way it is measured. Every batch leaves with a dimensional report against the drawing, and critical features are measured on a bridge CMM rather than eyeballed with calipers. How we check every part →
100+ materials, machined not sourced from a catalogue
Metals and engineering plastics from certified stock, or from material you send us. Each card opens the grade-by-grade page.
Common metal materials
Certified bar and plate stock, or material you supply.
- Aluminium 6061 / 7075
- Light, fast to cut, anodises well — the default for housings, plates and brackets
- Stainless steel 303 / 304 / 316L
- Corrosion resistance for fittings, manifolds, medical and food-contact parts
- Titanium Ti-6Al-4V
- Strength-to-weight and biocompatibility — EDC, aerospace, implants
- Brass C360 / Copper C110
- Electrical, thermal and decorative parts; the easiest metals in the shop
- Carbon, alloy & tool steel
- 1045, 4140, D2, S7 — shafts, fixtures, dies; hardened parts finished by EDM
Also: 5052, 6082, 2024 aluminium · 17-4 PH, 416 stainless · full metal list →
Common plastic materials
Machined from sheet and rod, not moulded — no tooling, any quantity.
- Acetal (POM) / Delrin
- Gears, bushings and precision moving parts; dimensionally stable
- Nylon PA6 / PA66
- Tough, wear-resistant rollers, guides and clamps
- Polycarbonate / Acrylic / ABS
- Clear covers, enclosures, prototypes
Also: PU · PP · PET · PSU / PPSU · PAI · PI · Ultem · G10 · carbon fibre · full plastics list →
Full material table — families, grades, typical use
| Family | Common grades | Typical use |
|---|---|---|
| Aluminium | 6061-T6, 7075-T6, 5052, 6082, 2024 | Housings, heat sinks, plates, brackets |
| Stainless steel | 303, 304, 316L, 17-4 PH, 416, 420 | Fittings, valve bodies, medical, marine |
| Carbon & alloy steel | 1018, 1045, 4140, 4340 | Shafts, gears, structural parts |
| Tool steel | D2 / SKD11, A2, S7, O1 | Dies, punches, wear plates — milled soft, EDM after hardening |
| Brass & copper | C360, C260, C110, C101, beryllium copper | Fittings, contacts, heat spreaders |
| Titanium | Ti-6Al-4V (Gr.5), Gr.2, Gr.23 | Knife and EDC parts, brackets, medical |
| Engineering plastics | Delrin (POM), Nylon 6/6, PEEK, PTFE, PC, Ultem, ABS, HDPE, PPS, PAI | Bushings, insulators, jigs, medical |
| Composites | G10 Garolite, carbon fibre | Handles, insulators, lightweight structures |
Finishes we specify and inspect for
Finishing is done by partner plants. We write the spec, allow for the coating in the machining, and check the parts when they come back.
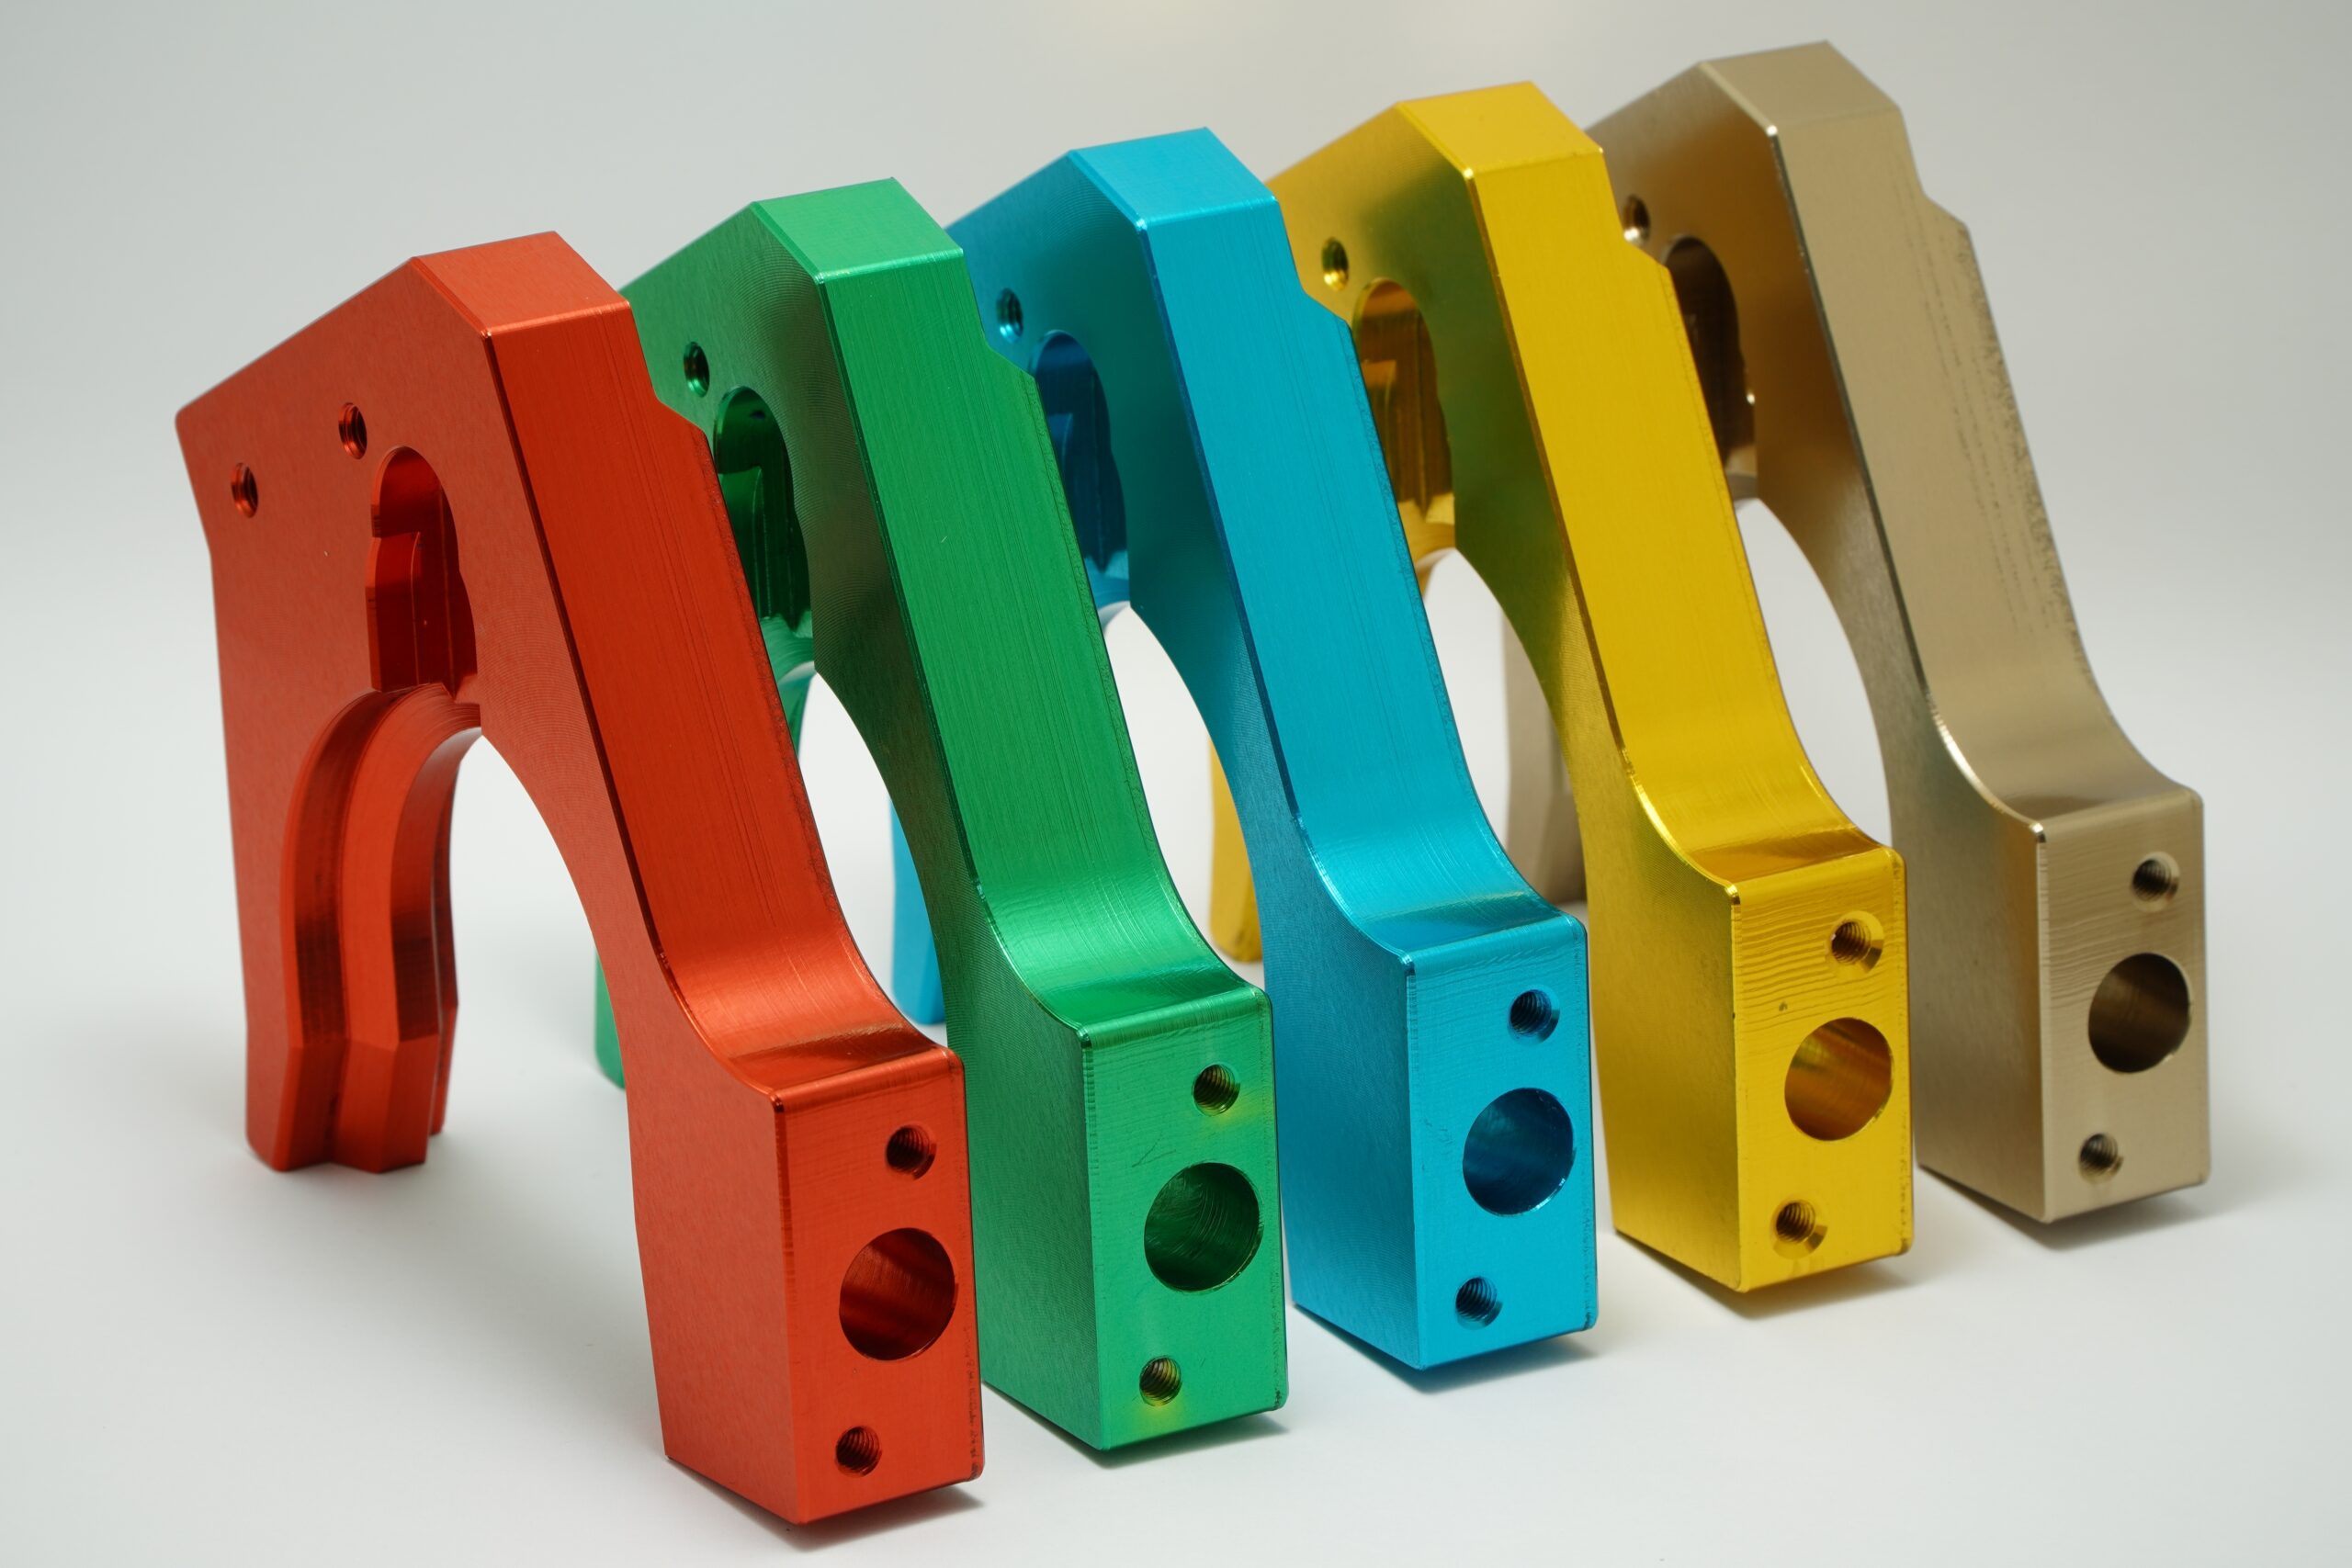
Anodising
Type II colour, Type III hard-coat — aluminium only
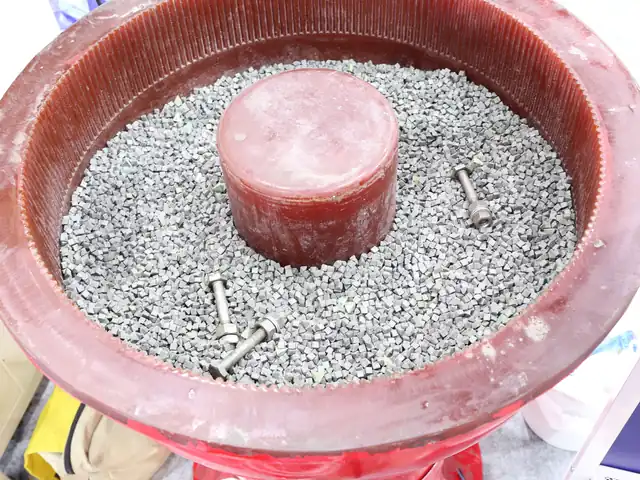
Tumbling
Deburred, stone-washed or brightened in vibratory media
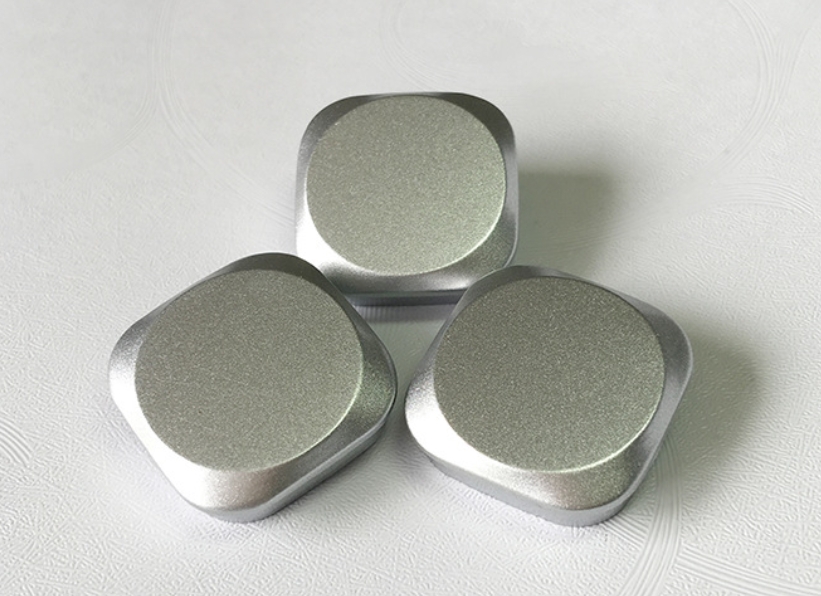
Bead blasting
Uniform matte that hides tool marks
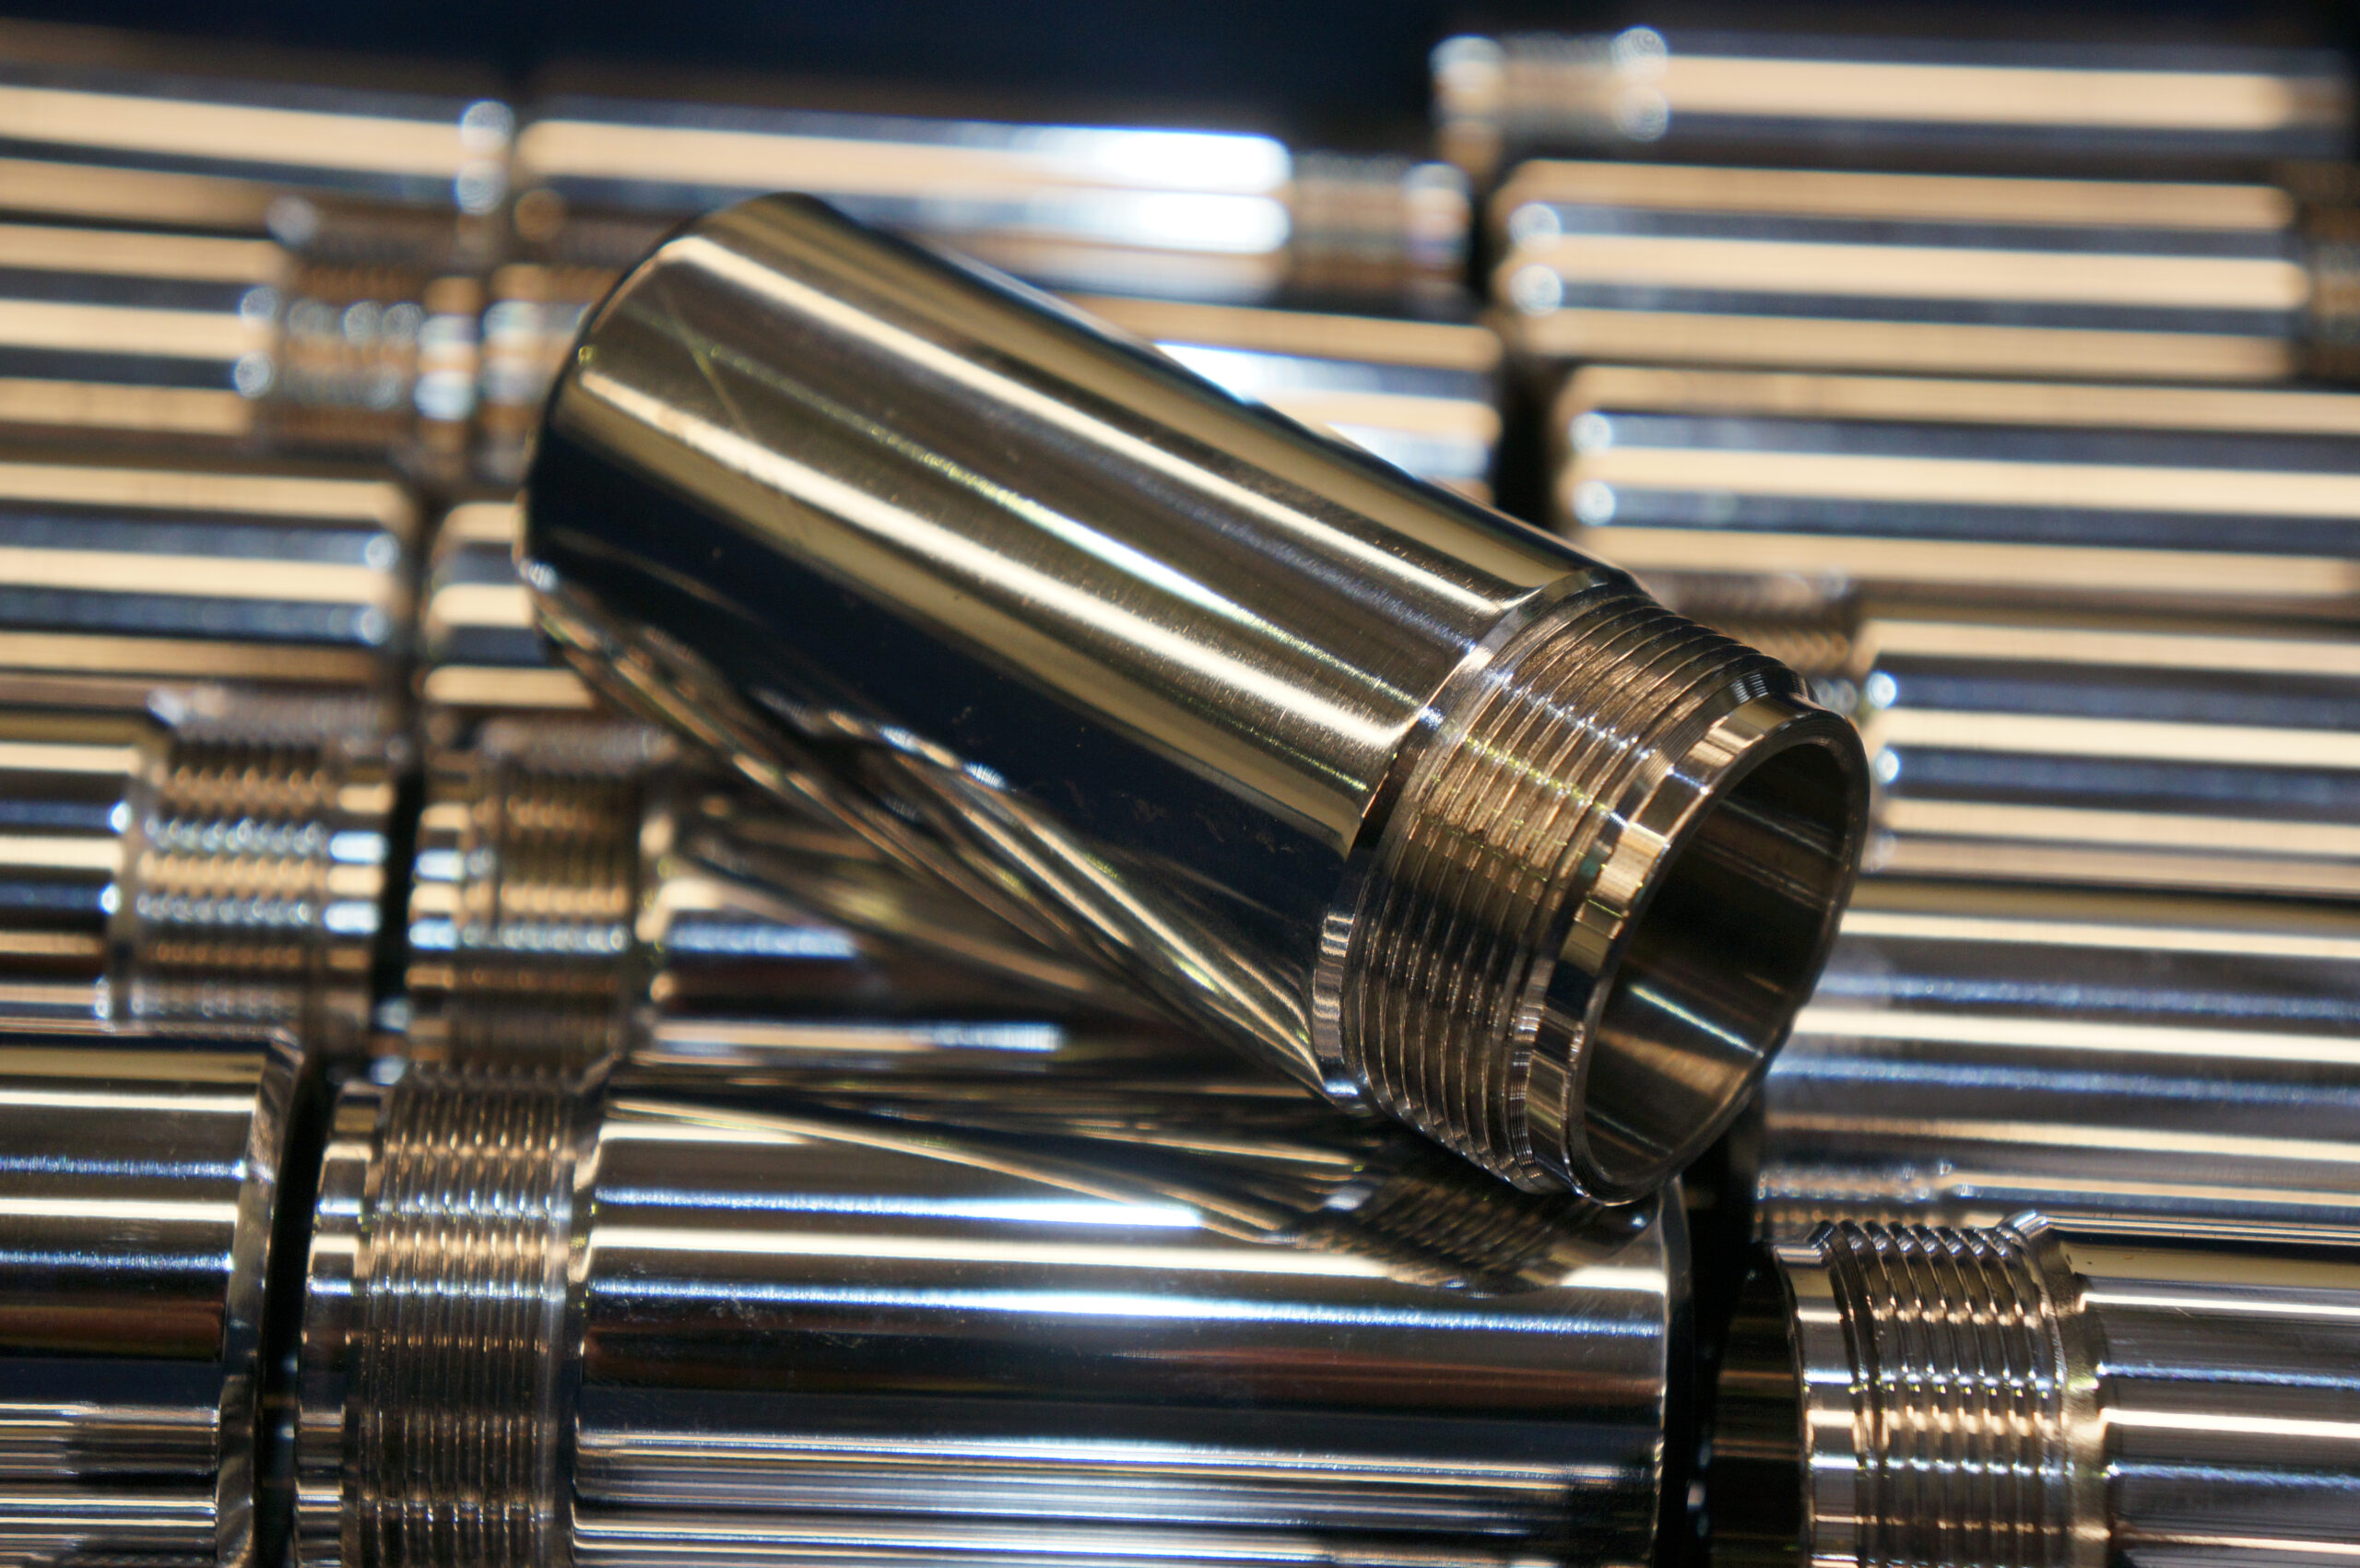
Plating
Zinc, nickel, chrome, electroless nickel
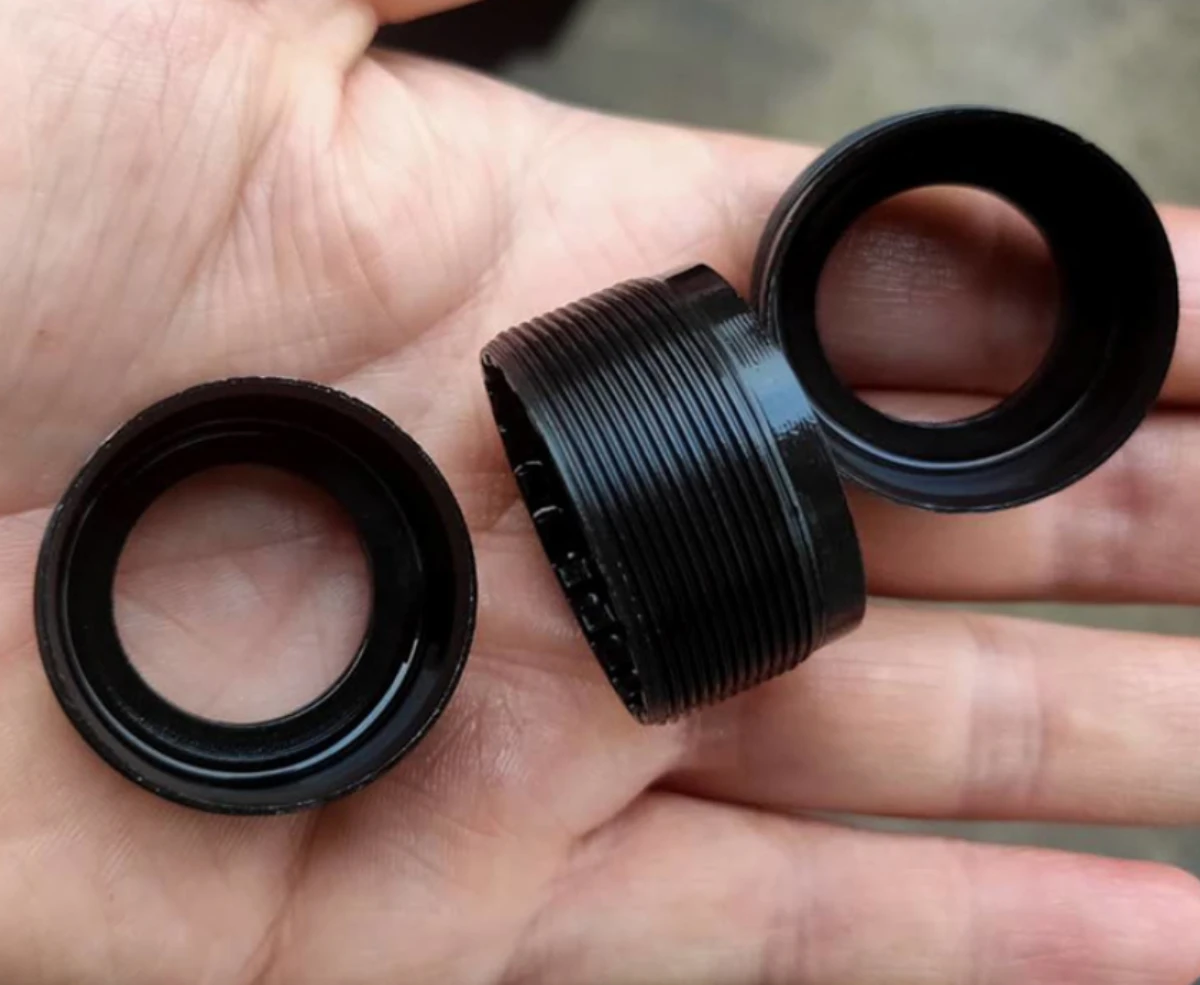
Black oxide
Steel tooling and fasteners, no size change
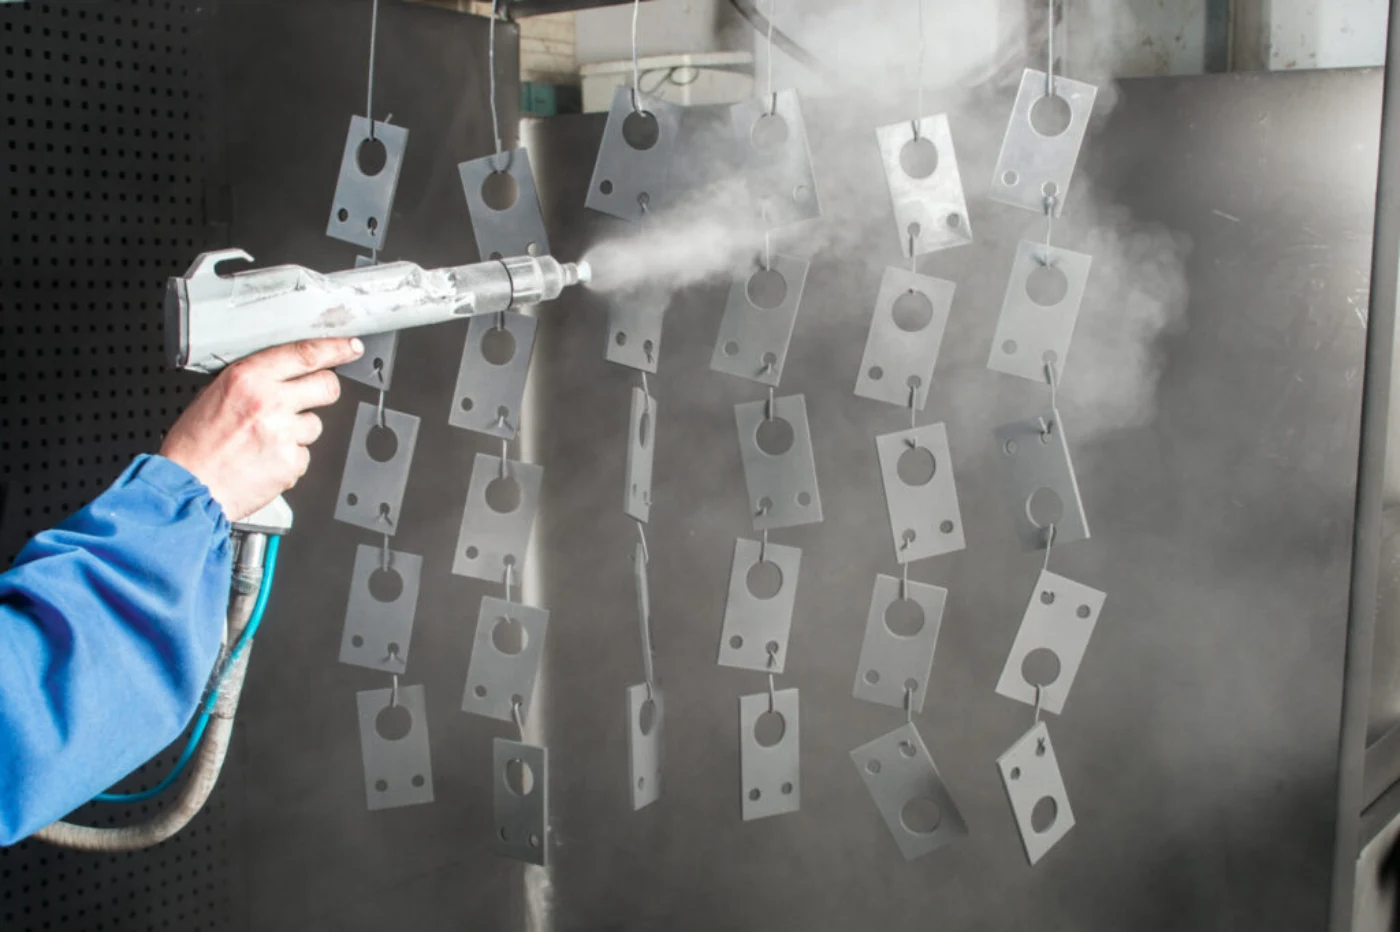
Powder coating
Tough colour film for housings and frames
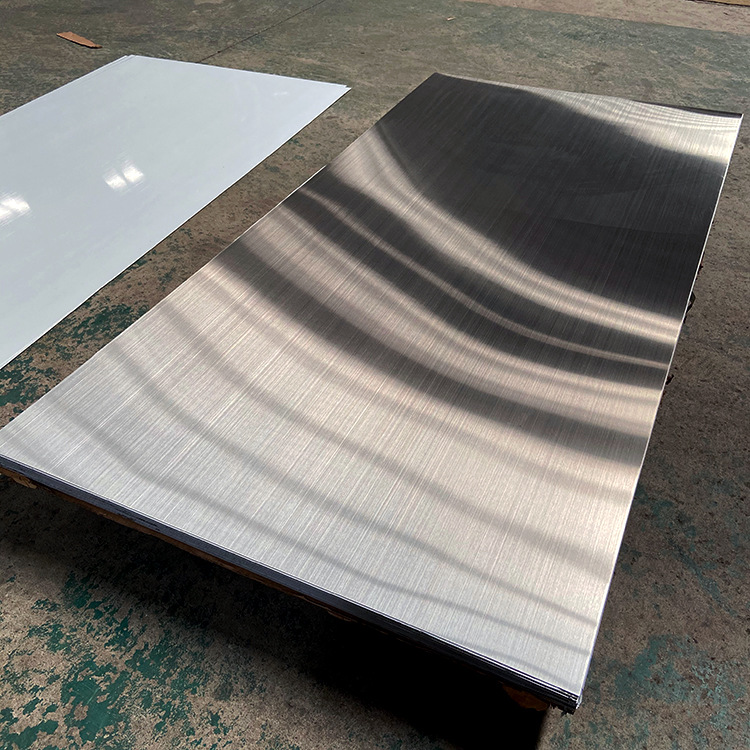
Brushing
Directional satin on stainless and aluminium
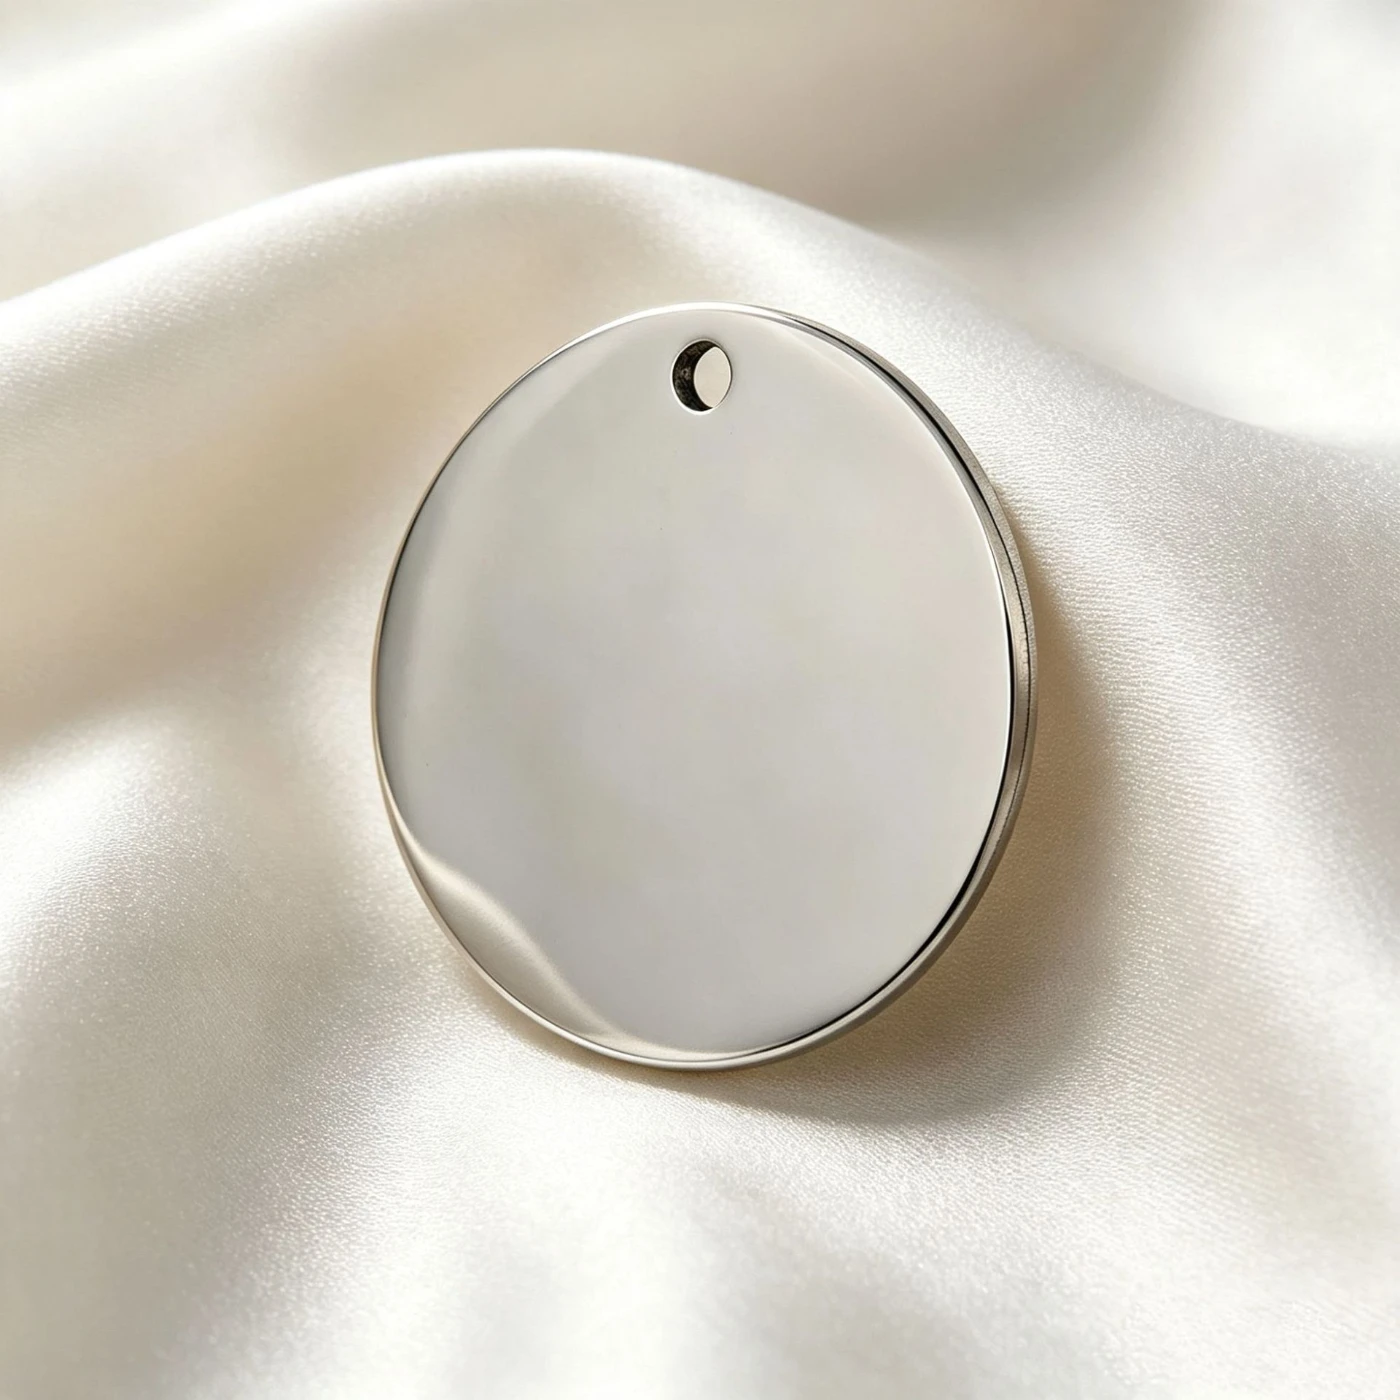
Polishing
Light polish or true mirror — two different jobs
From drawing to dock in five steps
Send files
STEP plus a 2D drawing to the quote form. NDA first if you prefer — we sign yours or send ours.
Engineer review
Bill reads the drawing, questions anything that decides whether the part works, and sends price and lead time within 16 hours.
Machine
Programmed and run in our own building, gauged between operations so a drifting tool is caught in minutes.
Measure
First article on the CMM against your datums before the run continues; dimensional report per batch.
Ship
Packed in trays or foam, photos before the box is sealed, DHL / FedEx / UPS with invoice and HS codes.
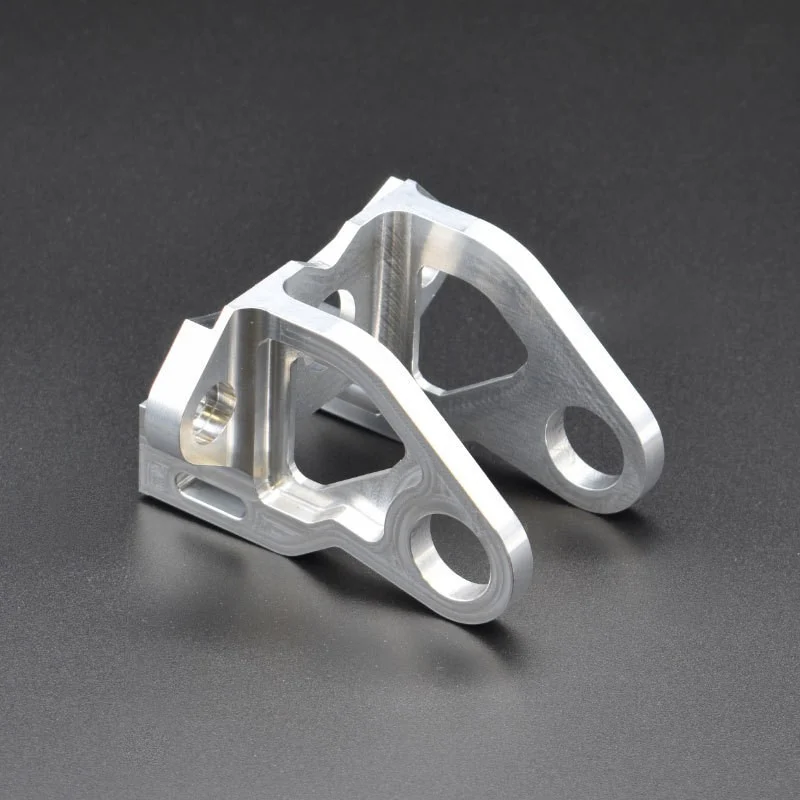
Parts off our machines
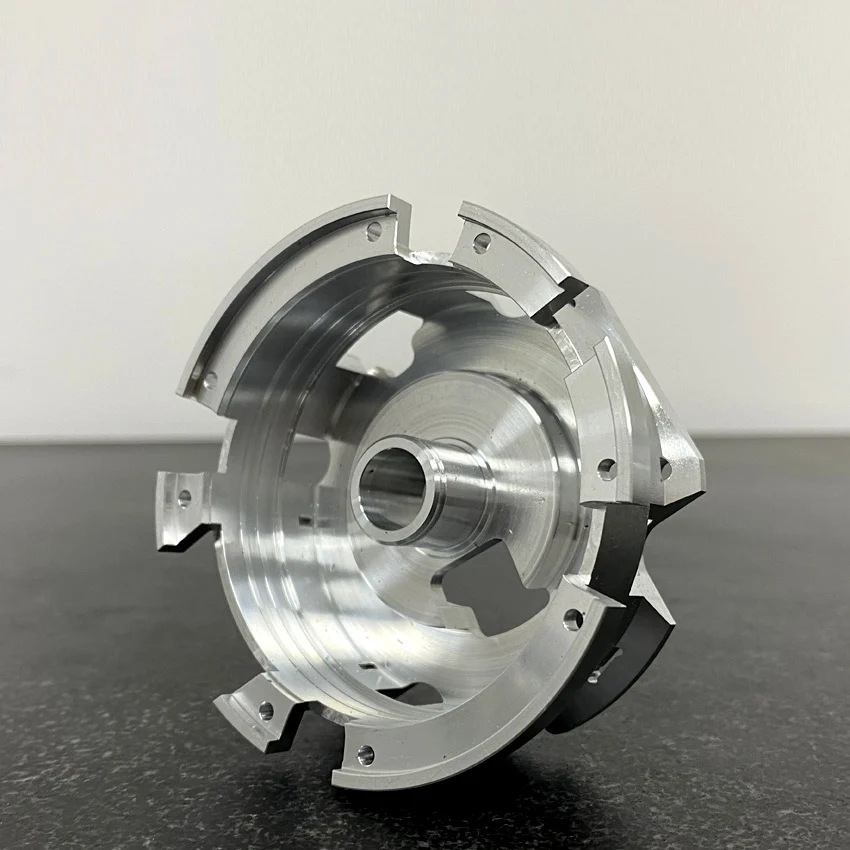
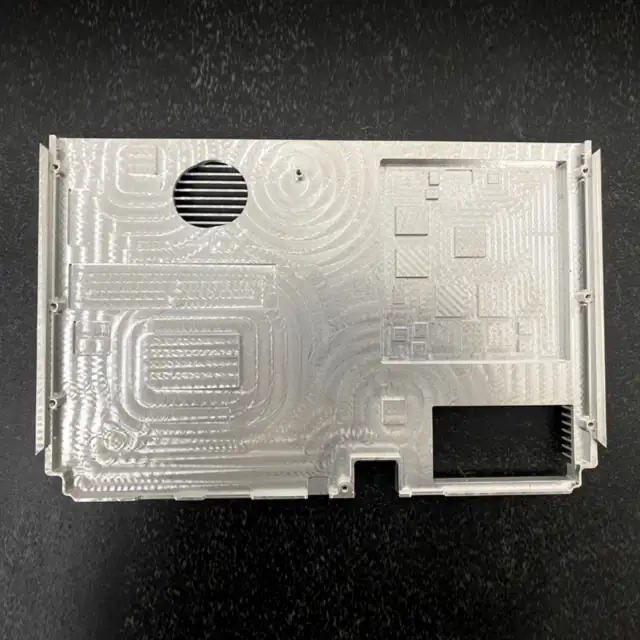
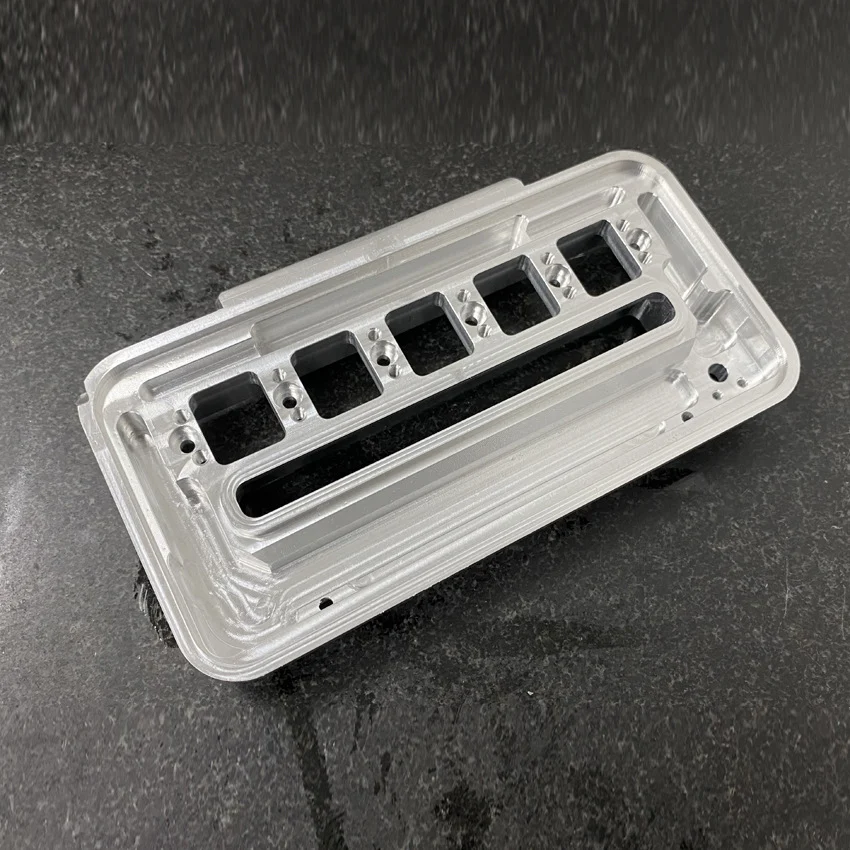
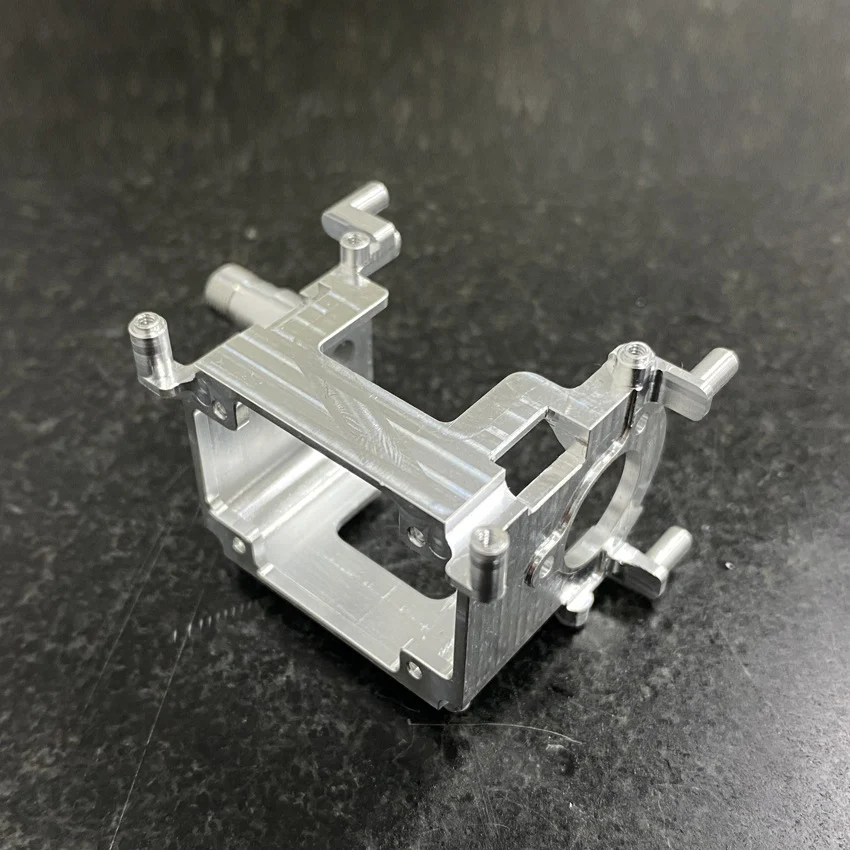
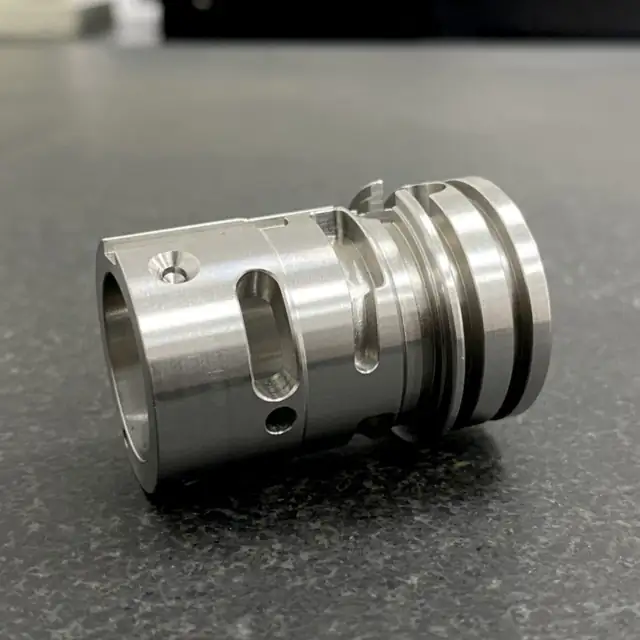
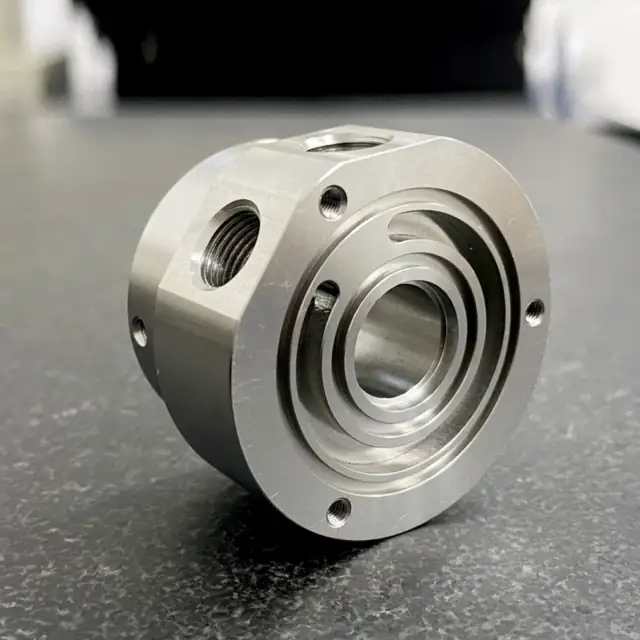
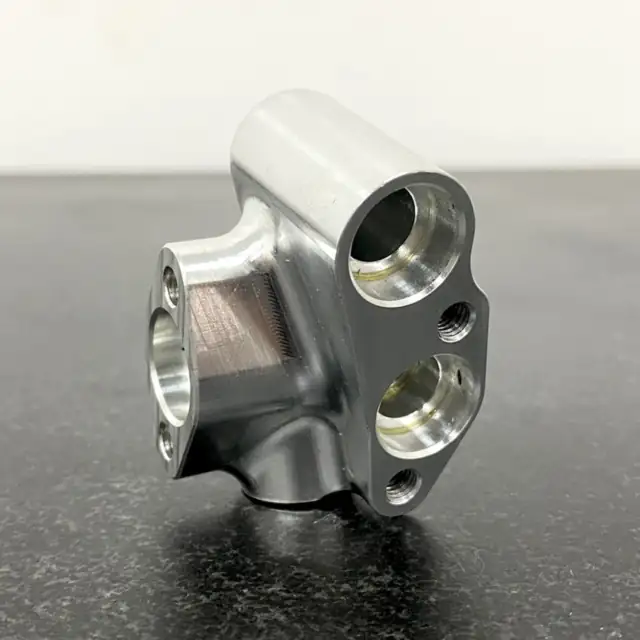
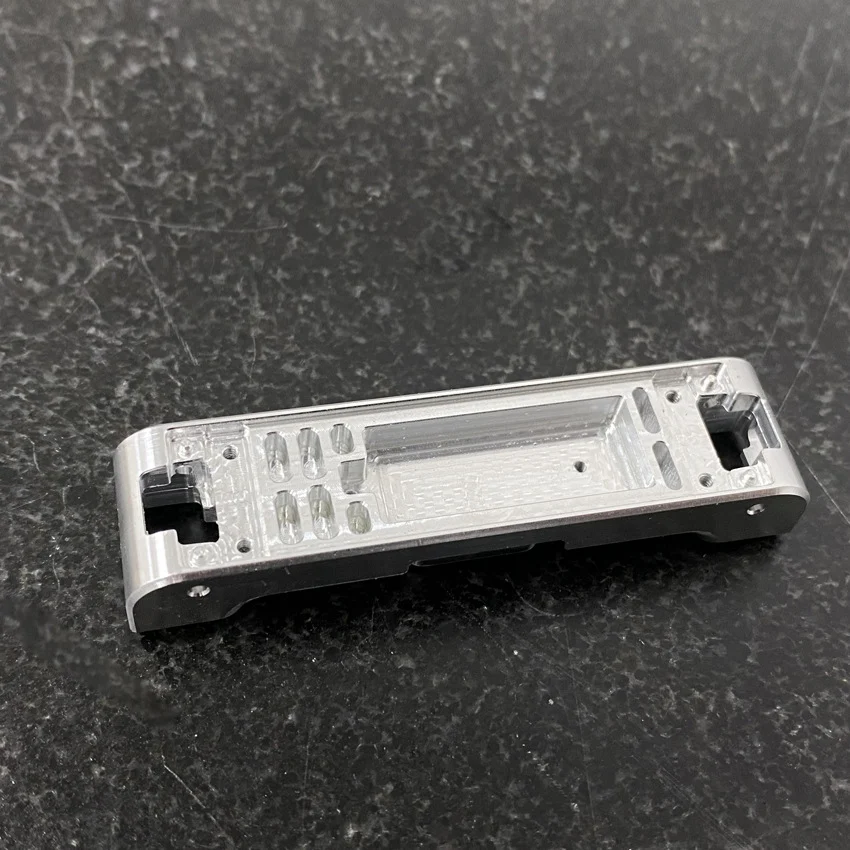
We do not publish customer parts or drawings. Every customer signs an NDA with us, and yours will be treated the same way. What you see here are sample parts from our own shop, our own floor and measuring room — never a customer’s job.
What buyers ask before the first order
What files do you need to quote a part?
Almost any 3D CAD file. STEP (.step / .stp) and IGES (.igs / .iges) are the safest, and we also open Parasolid (.x_t / .x_b), ACIS (.sat), SolidWorks (.sldprt), Inventor (.ipt), Creo / Pro-E (.prt), CATIA (.catpart), NX, Solid Edge, Rhino (.3dm), JT and Fusion 360 exports. If your software exports something else, send it anyway and we will tell you within the hour whether we can read it.
Send the 2D drawing as PDF (or DWG / DXF) with it — that is where tolerances, threads, surface finish and datums live, and a model on its own leaves every one of them to guesswork. For a simple part a dimensioned PDF alone is enough to quote. STL and OBJ meshes are fine for a rough price but not for machining: we ask for the solid model before anything is cut. Every file is covered by NDA and seen only by the engineering team.
Are you ISO 9001 certified?
No — not ISO 9001, 13485 or IATF 16949, and we would rather tell you here than have you find out during supplier approval. What we have instead is a temperature-controlled measuring room, a CMM with a Renishaw PH10M head, a first article measured before the rest of the run is cut, and a dimensional report with every batch.
Will you sign an NDA before I send drawings?
Yes. Send yours or we will send ours, before you upload anything. Files are used to quote and make your parts, nothing else, and are seen only by the engineering team.
What is the minimum order?
None. One prototype is quoted, machined and inspected the same way as a thousand. Unit price falls with quantity because setup is shared, and the quote shows both.
How fast can I get a quote and the parts?
A price and lead time within 16 hours of receiving usable files. Parts typically 5–10 working days depending on material and process; expedite is possible on many jobs — ask when you send the drawing.
Do you do 5-axis machining?
Not on our own machines. We run 3- and 4-axis milling, turning with live tooling, and EDM; four-axis covers most housings, manifolds and brackets in one setup. If your part genuinely needs simultaneous five-axis, send the drawing anyway: with your permission we pass it to one five-axis shop we know well, get you their price, and coordinate the job — engineering questions, inspection and shipping still go through GY. The quote states plainly which operations are done outside our own shop.
How do you ship, and who handles duties?
Express by DHL, FedEx or UPS door to door, with commercial invoice and HS codes — the right choice for samples and small batches. For bulk orders we usually recommend sea or rail freight, which we run regularly to Australia and Germany. To the US, fast sea freight takes about 20–25 days at roughly $3.48/kg; slow sea freight 35–40 days at roughly $2.12/kg (indicative 2026 rates — we quote the actual freight with the parts). DDP is available if you would rather we handle duties and brokerage up front.
Ready for a quote?
Send the drawing — price and lead time within 16 hours. STEP, IGES, X_T, DWG, DXF or PDF.
No minimum order.