Sinker EDM Machining Services
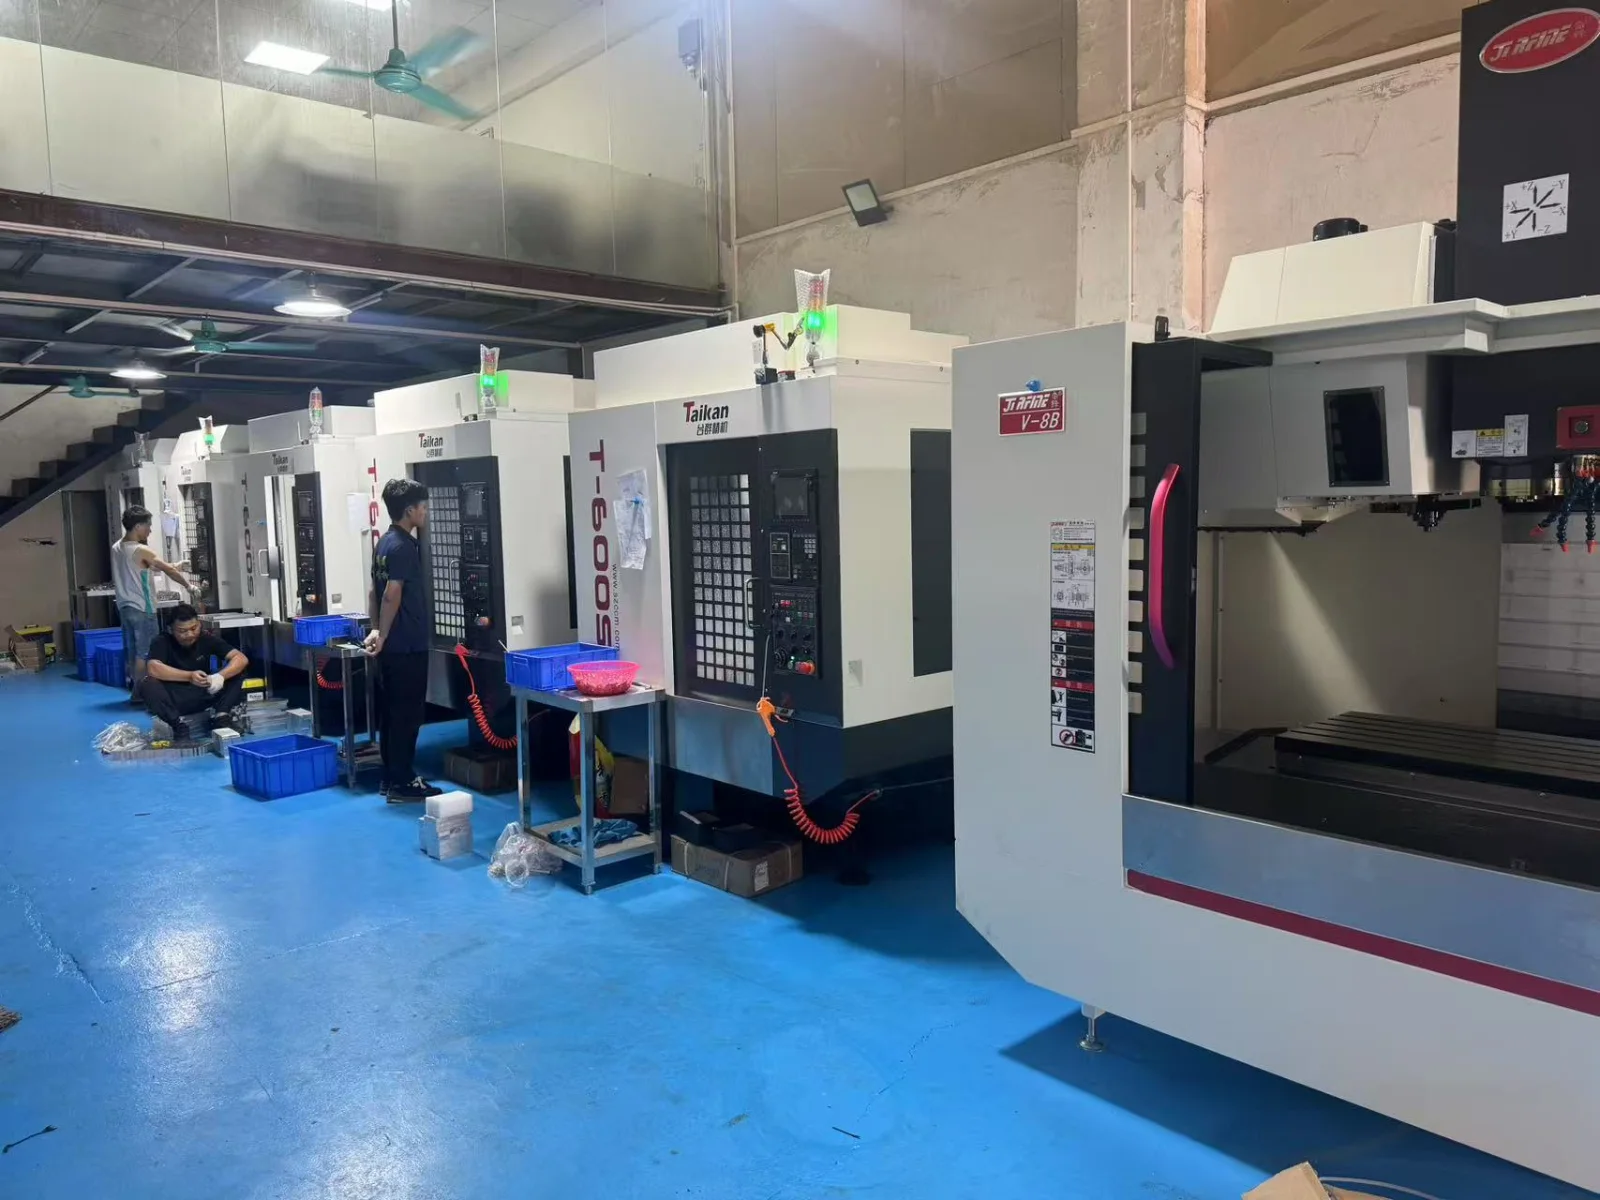
Six sinker EDM machines for blind cavities, square internal corners, deep keyways and features that have no through-path for a wire. Electrodes designed and machined in-house, so lead time does not depend on anyone else.
Burning a shape, not cutting it
Sinker EDM — also called die sinking or ram EDM — pushes a shaped copper or graphite electrode into the workpiece under a dielectric fluid. The spark erodes the exact negative of the electrode. Because nothing rotates and nothing touches, we can produce a square internal corner with no radius at all, sink a cavity into fully hardened steel, and reach into places where no cutter has clearance.
What we can sink
- Sinker EDM machines6
- Max workpiece500 × 350 × 250 mm
- Achievable tolerance±0.01 mm
- Internal cornerSquare — no radius required
- Surface finishRa 0.4 – 3.2 µm
- Max depthUp to 150 mm
- ElectrodesCopper and graphite, made in-house
- Material hardnessNo limit
A finer finish costs more time, not more money per part — tell us the Ra you actually need and we will quote the settings that reach it without over-polishing.
What customers use our sinker EDM for
Blind cavities
Pockets with a closed bottom, where a wire has no way in and a cutter cannot reach the corner.
Square internal corners
Keyways, hex and square broach forms, and splines with no corner radius.
Injection mould cores and cavities
Detail sunk into hardened tool steel after heat treatment.
Deep ribs and slots
Narrow features deeper than any end mill of that diameter can cut without chatter.
Text, logos and serial marks
Engraved into hardened surfaces where laser marking will not survive the process.
Broken tap and stud removal
Eroding out a seized tool without damaging the thread around it.
Materials we sink
Any conductive material, hardened or annealed. Tool steels are the everyday work; we also sink stainless, titanium and carbide.
Before you send the drawing
Do I need to supply the electrode?
Wire EDM or sinker EDM — which do I need?
How square can an internal corner really be?
What surface finish comes off the machine?
Often ordered together
Wire EDM
Through-profiles, sharp corners and hardened plate, cut with a wire. Wire EDM →
CNC Milling
The part and its electrodes are milled on the same floor, days before they meet. CNC milling →
Surface finishing
Polishing, plating and coating after the cavity is sunk. Surface finishes →
Send the drawing. You will have a price and a lead time in 16 hours.
STEP, IGES, X_T, DWG, DXF or PDF. Metric or inch. No minimum order.